
As a leading industrial fluid equipment manufacturer established in 2003, Depam (Hangzhou) Pump Technology Co., Ltd. has dedicated over two decades to perfecting precision fluid handling solutions. With 400+ employees operating across a 35,000㎡ production facility, our company combines German engineering expertise with continuous innovation to deliver annual output valued at approximately 500 million RMB. Specializing in high-end positive displacement pumps and integrated fluid systems, we serve global industries including petrochemical refining, nuclear power, metallurgy, renewable energy, and environmental protection through our three operational brands: Depam, Knirowa, and Dailupu.
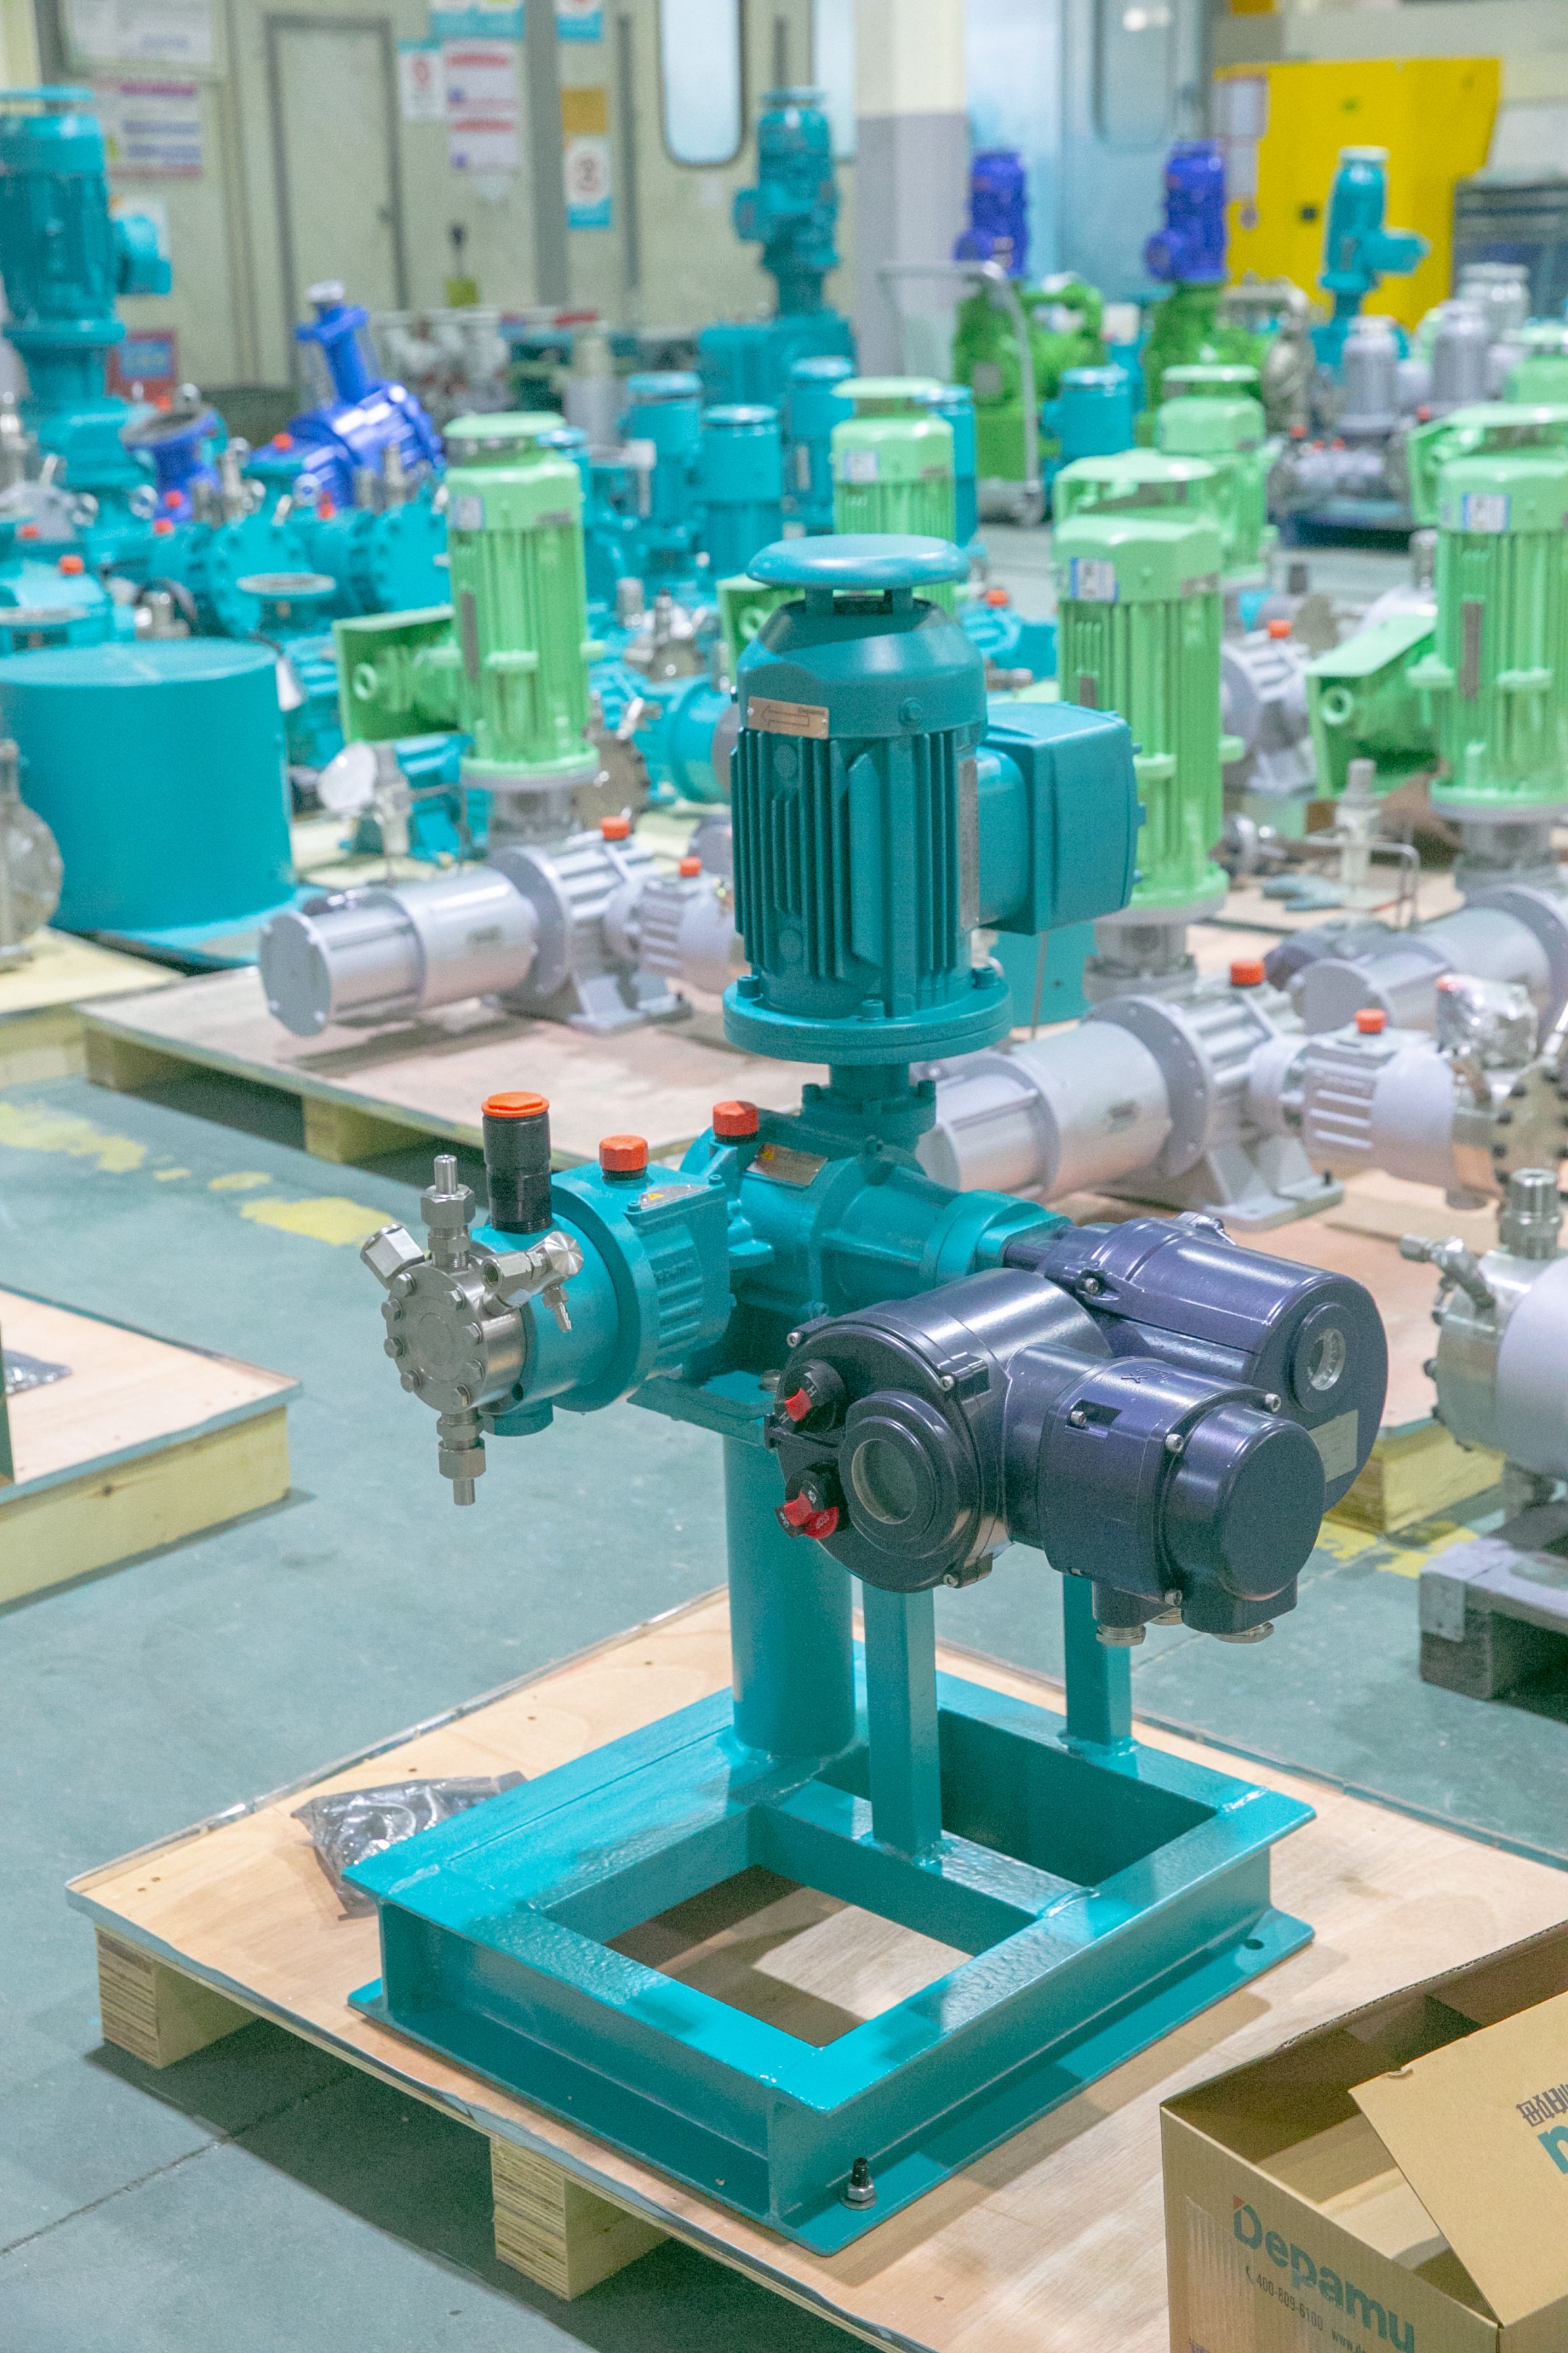
Core Product Expertise: Hydraulic Diaphragm Metering Pumps
Our flagship hydraulic diaphragm metering pumps represent the pinnacle of precision chemical injection technology. Designed as industrial-grade “precision infusion devices,” these pumps deliver chemical agents with ±1% accuracy through adjustable stroke length and operating frequency control. The hydraulic-driven diaphragm structure ensures completely leak-free operation even when handling highly corrosive, volatile, or high-pressure media. This makes them indispensable in petrochemical processing, wastewater treatment, pharmaceutical manufacturing, food production, and new energy applications requiring exact dosage control.
The pumps’ robust construction features 316L stainless steel wetted parts, PTFE diaphragms, and Hastelloy valves to withstand aggressive chemicals. Their modular design allows easy maintenance and component replacement, while the intelligent control system supports remote monitoring and automatic calibration. With flow rates ranging from 5 L/h to 20,000 L/h and pressure capacities up to 400 bar, our metering pumps meet diverse industrial requirements from laboratory-scale operations to full-scale production lines.
High-Pressure Process Reciprocating Pumps: Industrial Powerhouses
Serving as “powerful pressure boosters” in industrial pipelines, our high-pressure process reciprocating pumps generate pressures exceeding 35MPa through precision-engineered plunger reciprocation. These pumps excel at transporting viscous fluids, high-temperature liquids, and media containing solid particles over long distances or to elevated pressure zones. Their continuous-duty design ensures reliable operation in demanding environments like oilfield water injection, petrochemical process transfer, pipeline增压 (pressure boosting), and geothermal energy extraction.
Key technical advantages include:
- Pressure stability with ±1% variation under constant load
- Flow rate consistency maintained through variable speed drives
- Material compatibility with duplex stainless steel, nickel-based alloys, and ceramic-lined components
- Energy efficiency optimized through hydraulic end design improvements
- Safety certifications including API 674, CE, and ATEX compliance
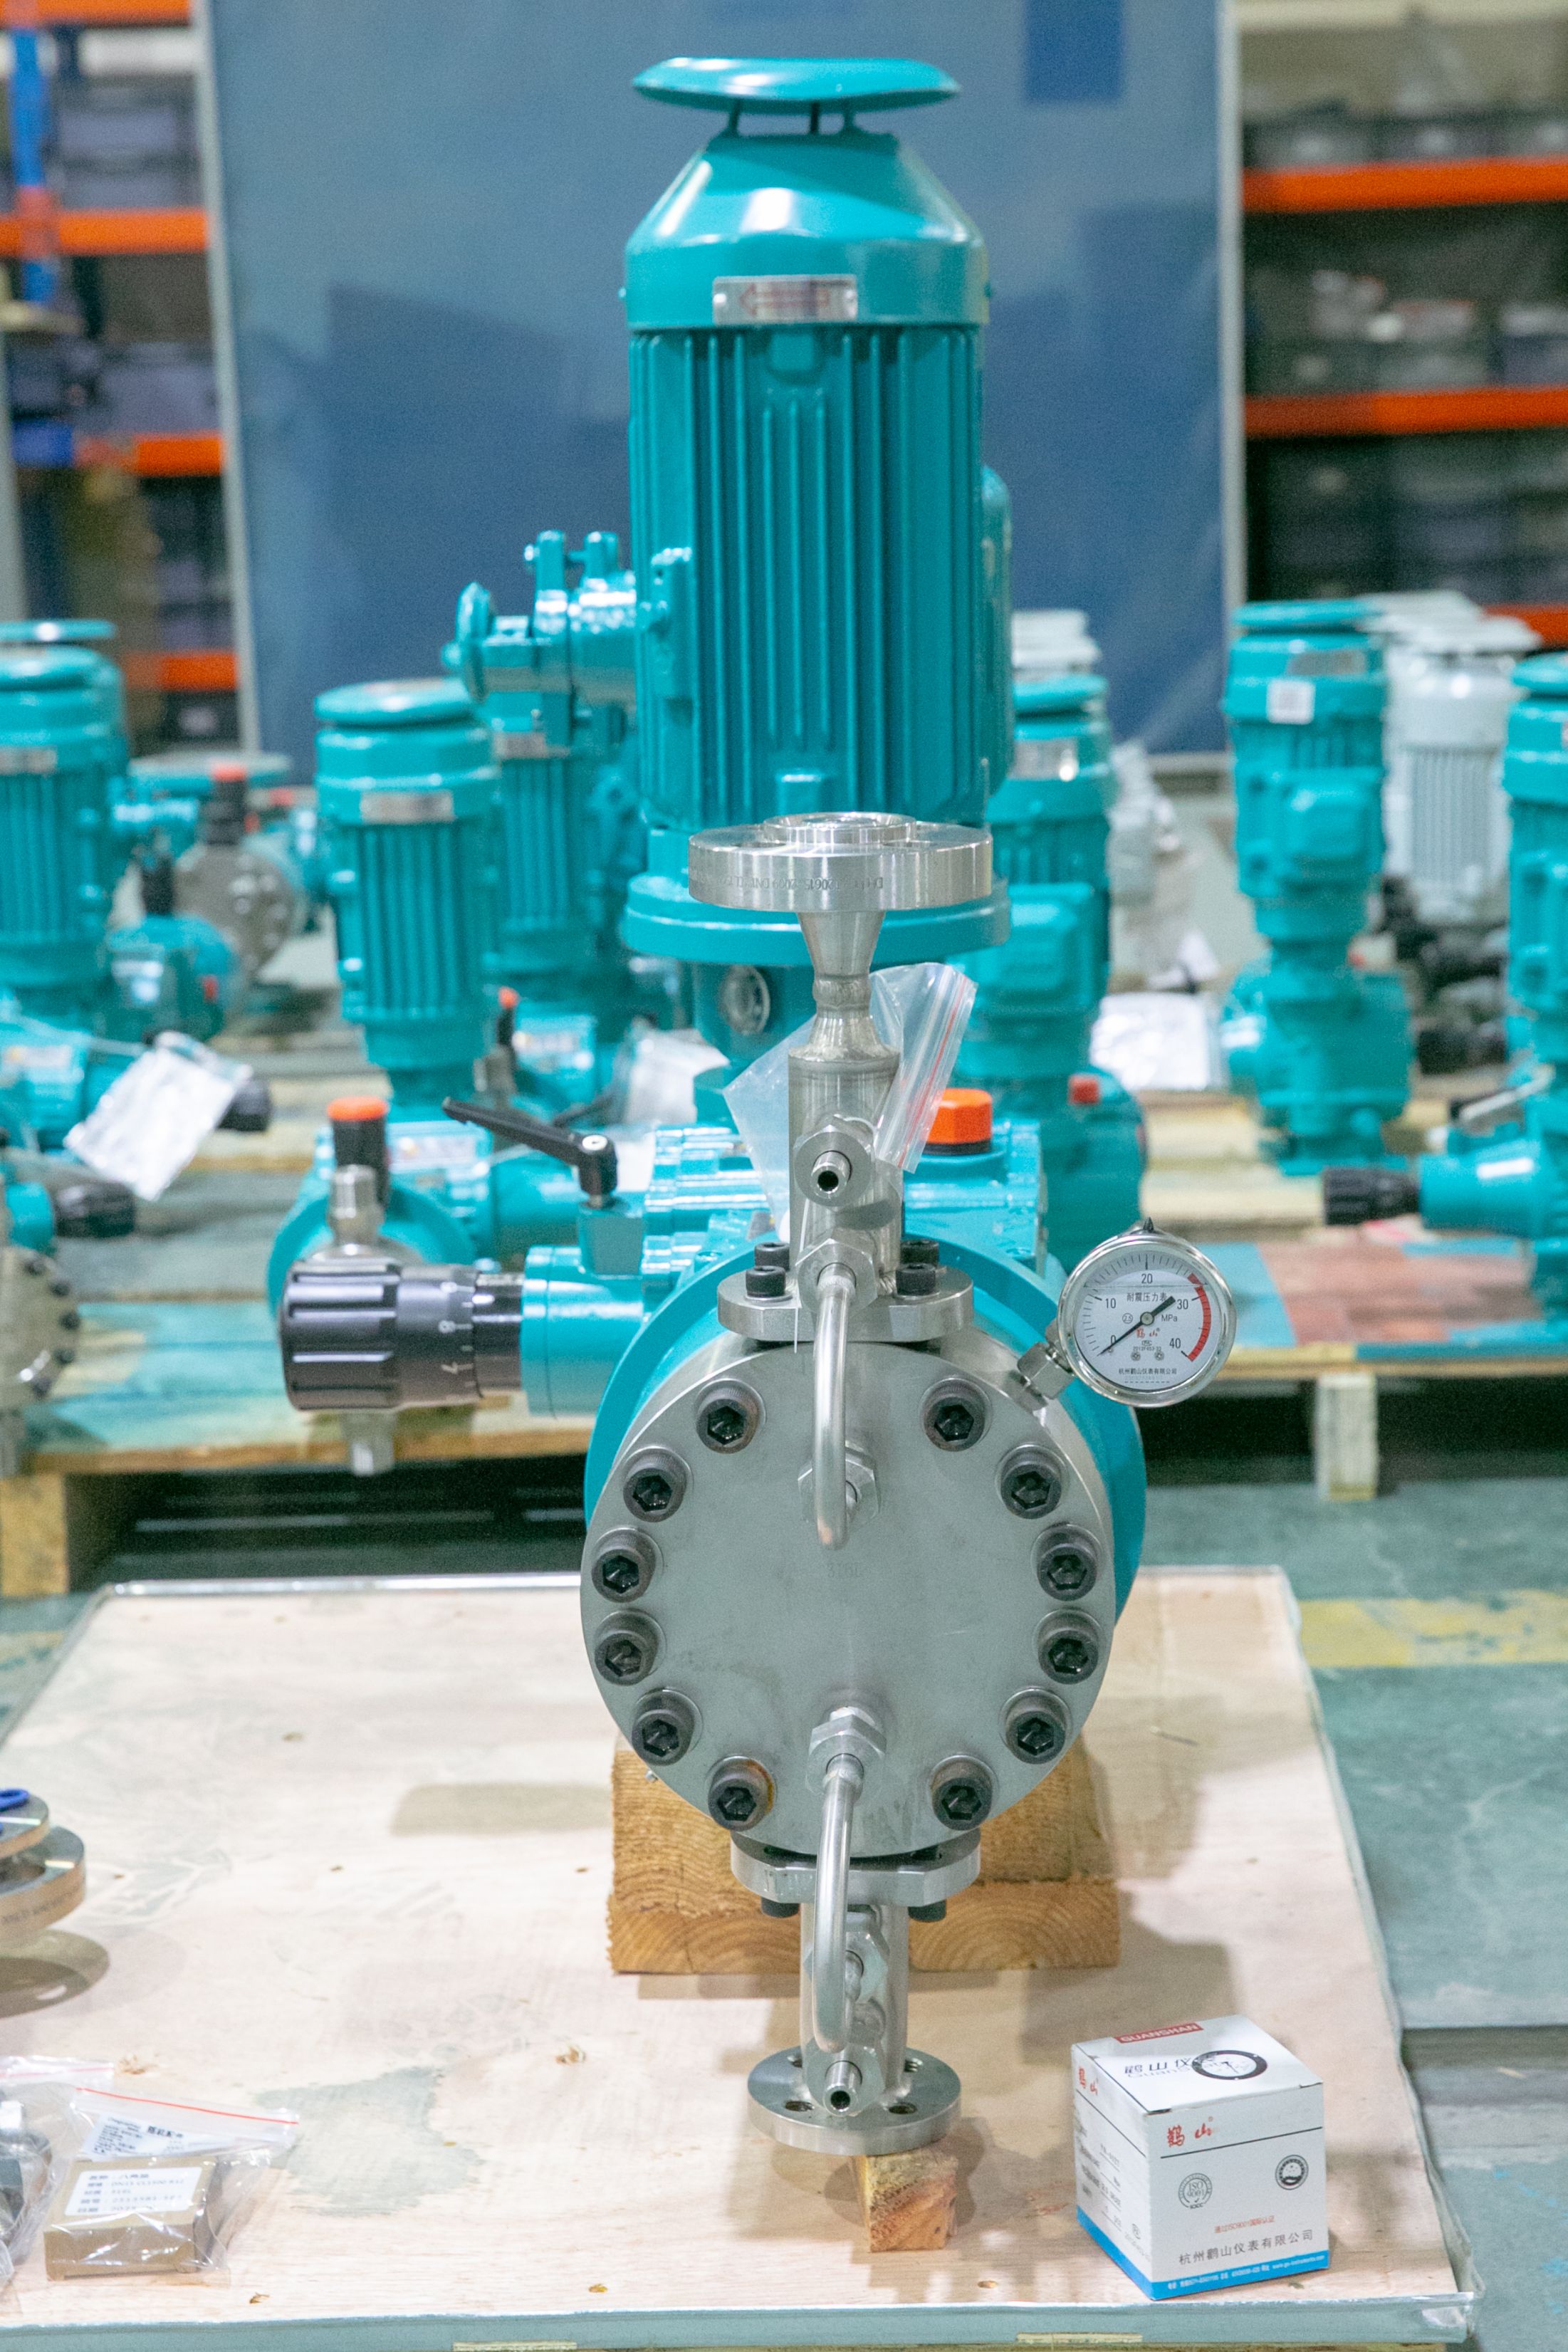
Technical Specifications Comparison
| Parameter | Hydraulic Diaphragm Metering Pump | High-Pressure Reciprocating Pump |
|---|---|---|
| Flow Rate Range | 5-20,000 L/h | 0.5-500 m³/h |
| Pressure Capacity | Up to 400 bar | Up to 500 bar |
| Precision | ±1% | ±2% |
| Media Compatibility | Corrosive chemicals, solvents, acids | Viscous fluids, slurries, high-temp liquids |
| Typical Applications | Chemical dosing, water treatment, food processing | Oilfield injection, pipeline transfer, pressure testing |
Integrated Fluid Solutions: Chemical Dosing Systems
Our fully automatic chemical dosing systems represent the next generation of industrial fluid management. Combining storage, dissolution, mixing, metering, and control functions into a single skid-mounted unit, these systems operate as “automated chemical preparation stations” that arrive pre-assembled and factory-tested for immediate operation. The intelligent control system manages multiple dosing points simultaneously, adjusting injection rates based on process parameters like pH, conductivity, or flow rate.
Key system features include:
- Dual-tank configuration for continuous operation during refilling
- Explosion-proof design for hazardous area applications
- Remote monitoring via MODBUS or PROFIBUS protocols
- Dry powder/liquid dual-mode dosing capability
- Automatic backflushing to prevent clogging
These systems have been successfully implemented in boiler water treatment at power plants, wastewater neutralization at chemical facilities, and scale inhibition in oilfield produced water treatment. One notable project at a Middle Eastern petrochemical complex reduced chemical consumption by 18% while improving product quality consistency through precise dosing control.
Customization Capabilities: Engineering Beyond Standards
What truly distinguishes Depam is our ability to transform standard products into tailored solutions. Our engineering team works closely with clients to analyze process requirements including media characteristics, temperature ranges, pressure profiles, and spatial constraints. This collaborative approach has produced specialized equipment such as:
- Submersible metering pumps for offshore platform applications
- High-temperature reciprocating pumps (up to 350°C) for geothermal power
- ATEX-certified explosion-proof pumps for refinery operations
- Mobile dosing trailers for temporary water treatment projects
- Multi-pump synchronized systems for large-scale chemical blending
Our customization process follows ISO 9001 quality management standards, with each project undergoing FEA analysis, 3D modeling, and virtual commissioning before production. This rigorous approach ensures that customized solutions deliver the same reliability and performance as our standard product lines.
Industry Application Breakdown
Our diverse product portfolio serves multiple industrial sectors with specialized solutions:
- Petrochemical Refining (41%): Metering pumps for catalyst injection, reciprocating pumps for crude transfer, dosing systems for sulfur recovery
- Oil & Gas (23%): High-pressure pumps for water injection, chemical injection pumps for enhanced oil recovery, offshore platform equipment
- Nuclear Power (8%): Boron dosing systems, primary circuit sampling pumps, radiation-resistant fluid handling equipment
- Environmental Protection (13%): Wastewater neutralization systems, sludge transfer pumps, ozone generation feed pumps
- New Energy (7%): Lithium battery electrolyte pumps, hydrogen production chemical dosing, geothermal power plant equipment
FAQ
What makes hydraulic diaphragm metering pumps more reliable than mechanical diaphragm types?
Hydraulic diaphragm pumps use pressurized hydraulic fluid to actuate the diaphragm, eliminating diaphragm stress from mechanical linkage. This design provides longer diaphragm life (typically 8,000-10,000 hours vs. 3,000-5,000 hours for mechanical types), better pressure stability, and the ability to handle higher pressures (up to 400 bar vs. 250 bar maximum for mechanical diaphragm pumps).
How do you ensure chemical compatibility with your pump materials?
Our material selection process involves three key steps: 1) Analyzing the chemical composition, concentration, and temperature of the media 2) Conducting laboratory corrosion tests on candidate materials 3) Selecting from our range of 316L stainless steel, duplex steel, Hastelloy, PTFE, PVDF, and ceramic-lined components. We provide detailed material compatibility charts and offer free sample testing for critical applications.
What maintenance procedures are required for high-pressure reciprocating pumps?
Regular maintenance includes: 1) Daily inspection of lubrication levels and pressure gauges 2) Weekly checking of plunger packing and valve condition 3) Monthly replacement of lubricating oil and filters 4) Quarterly inspection of the hydraulic end for wear 5) Annual overhaul of major components. Our pumps come with predictive maintenance manuals and we offer training programs for client maintenance teams.
Can your chemical dosing systems handle viscous chemicals?
Yes, our systems can be configured with progressive cavity pumps or gear pumps for viscous media up to 100,000 cP. Special features include heated tanks for temperature-sensitive chemicals, agitators for slurry mixing, and self-cleaning filters to prevent clogging. We recently supplied a system handling 85% phosphoric acid at 150°C for a fertilizer plant.
Summary
Depam Pump Technology stands as a comprehensive solution provider in industrial fluid handling, combining German-engineered precision with Chinese manufacturing efficiency. Our product range from hydraulic diaphragm metering pumps to integrated chemical dosing systems addresses the complete spectrum of industrial fluid management requirements. With 22 years of continuous innovation, 400+ skilled professionals, and 35,000㎡ of advanced production facilities, we deliver not just equipment but complete process optimization solutions. Our commitment to quality is demonstrated through ISO 9001, ISO 14001, and ISO 45001 certifications, along with product certifications including CE, ATEX, and API standards. Whether you require standard products or customized fluid systems, Depam provides the expertise, technology, and support to keep your industrial processes running smoothly and efficiently.