
When it comes to industrial fluid handling, lobe pumps stand out as versatile and reliable solutions across various sectors. As a leading lobe pump manufacturer and supplier since 2003, Depampump (Hangzhou) Pump Technology Co., Ltd. has established itself as a trusted name in the global market. Our comprehensive range of lobe pumps, combined with our ability to deliver custom solutions, makes us the preferred choice for businesses seeking high-performance fluid transfer equipment.
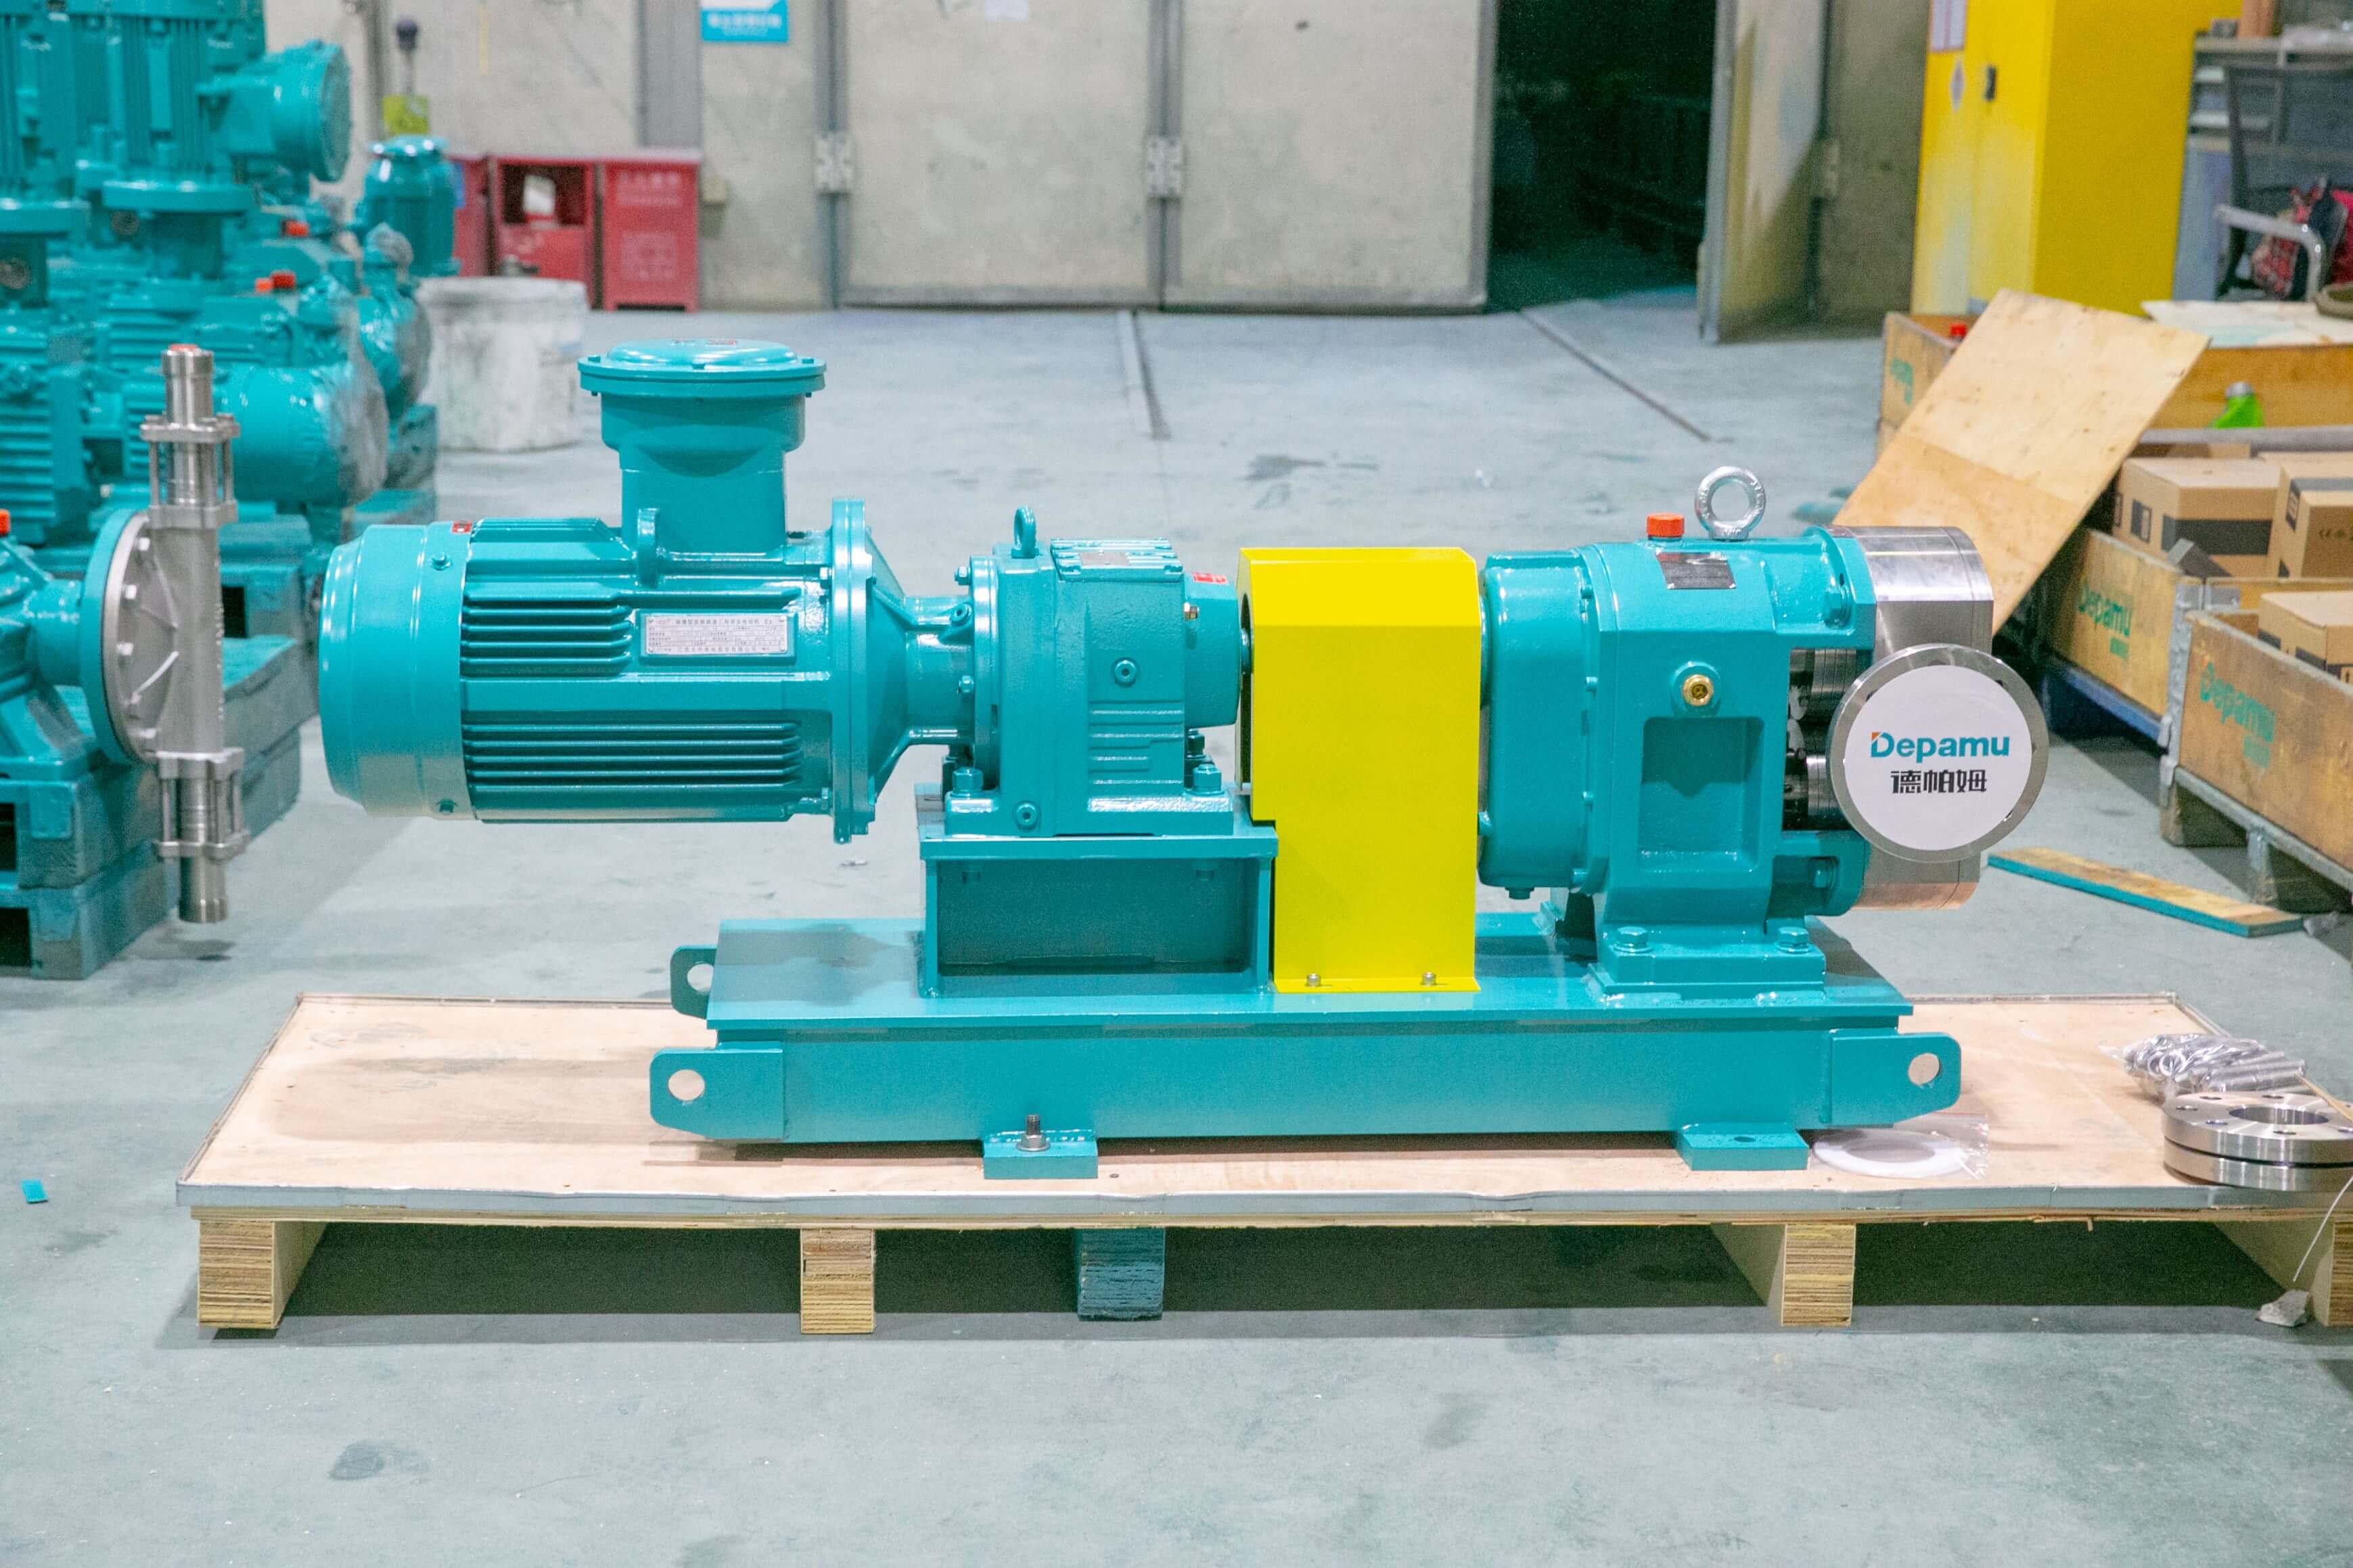
Understanding Lobe Pumps: The Industrial Workhorse
Lobe pumps belong to the category of positive displacement pumps, known for their ability to handle a wide variety of fluids with precision and reliability. These pumps feature two or more lobes that rotate in opposite directions within a pump casing, creating a suction effect that draws fluid in and then pushes it out through the discharge port. The non-contacting design of the lobes ensures minimal wear and tear, making lobe pumps ideal for applications requiring gentle handling of shear-sensitive products or abrasive slurries.
At Depampump, we specialize in manufacturing lobe pumps that excel in demanding industrial environments. Our pumps are engineered to handle fluids with varying viscosities, from thin liquids to thick slurries, while maintaining consistent flow rates and pressure levels. This versatility makes our lobe pumps suitable for diverse applications across multiple industries.
Our Lobe Pump Product Range: Tailored to Your Needs
As a comprehensive lobe pump supplier, we offer a wide range of standard and custom-designed lobe pumps to meet the specific requirements of our global clientele. Our product portfolio includes:
- Standard Lobe Pumps: Designed for general industrial applications, these pumps provide reliable performance for transferring a variety of fluids.
- Sanitary Lobe Pumps: Built with hygienic materials and finishes, these pumps are ideal for food, beverage, and pharmaceutical applications where cleanliness is paramount.
- High-Pressure Lobe Pumps: Engineered to generate significant pressure, these pumps are suitable for applications requiring forceful fluid transfer, such as in oil and gas operations.
- Chemical-Resistant Lobe Pumps: Constructed with materials that resist corrosion, these pumps handle aggressive chemicals and solvents with ease.
- Custom Lobe Pumps: Our engineering team works closely with clients to design and manufacture lobe pumps tailored to specific process requirements, including unique materials, sizes, and configurations.
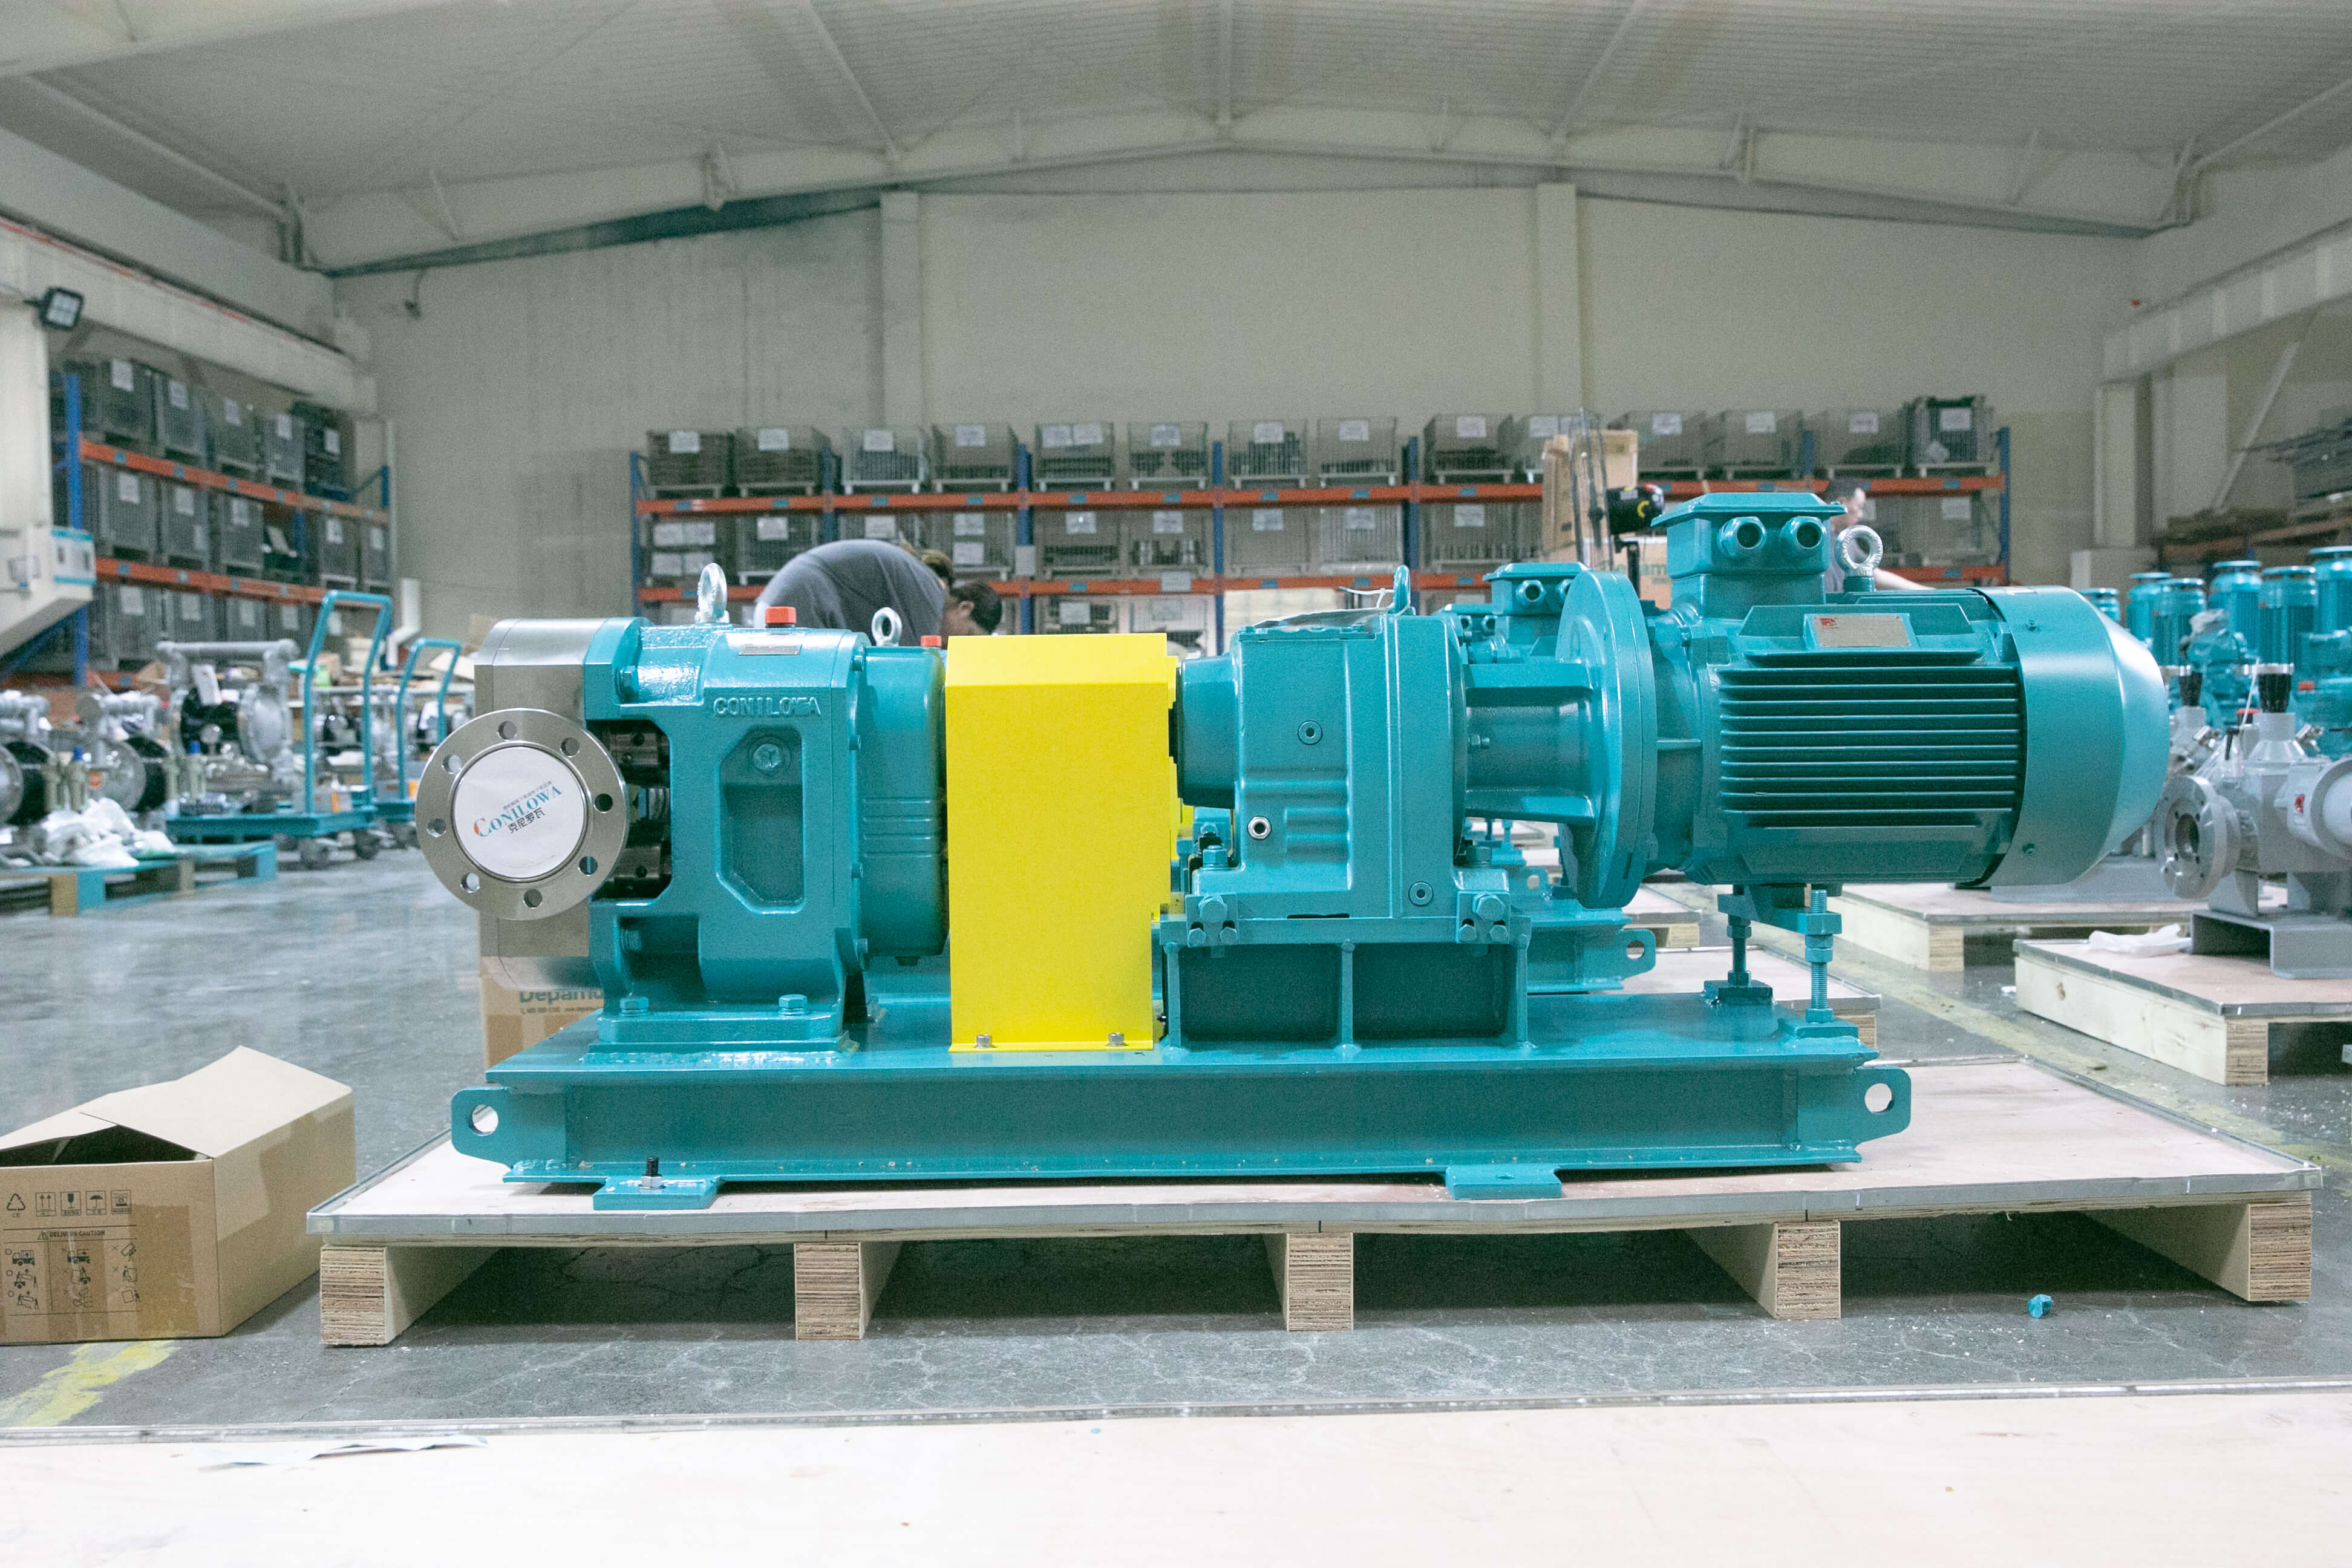
Key Features of Our Lobe Pumps
Our lobe pumps are designed with several key features that set them apart in the market:
- Robust Construction: Built to withstand harsh industrial environments, our pumps feature durable materials and precision engineering.
- Efficient Performance: The lobe design ensures smooth, pulsation-free flow, minimizing energy consumption and maximizing efficiency.
- Easy Maintenance: The simple, accessible design of our lobe pumps makes routine maintenance and repairs straightforward, reducing downtime.
- Versatile Applications: From handling delicate food products to transferring abrasive slurries, our lobe pumps adapt to a wide range of fluids and processes.
- Customization Options: We offer extensive customization options to tailor our lobe pumps to your specific process requirements, ensuring optimal performance.
Industries Served by Our Lobe Pumps
Depampump’s lobe pumps find applications across numerous industries, thanks to their versatility and reliability. Some of the key sectors we serve include:
| Industry | Applications |
|---|---|
| Chemical Processing | Transferring corrosive chemicals, solvents, and acids; handling slurries and viscous fluids |
| Oil & Gas | High-pressure fluid transfer in upstream and downstream operations; handling crude oil, drilling mud, and produced water |
| Food & Beverage | Transferring delicate food products like yogurt, cream, and sauces; handling viscous ingredients and slurries |
| Pharmaceuticals | Handling sterile fluids and active pharmaceutical ingredients (APIs); ensuring gentle product transfer |
| Water Treatment | Transferring chemicals for water treatment processes; handling sludge and wastewater |
| Pulp & Paper | Handling pulp slurries, coatings, and adhesives; transferring chemicals for paper production |
Why Choose Depampump as Your Lobe Pump Supplier?
With numerous lobe pump manufacturers in the market, selecting the right partner for your industrial fluid handling needs is crucial. Here are several compelling reasons to choose Depampump:
- Extensive Experience: With over two decades of experience in the pump industry, we have the knowledge and expertise to deliver high-quality solutions.
- Customization Capabilities: Our ability to design and manufacture custom lobe pumps sets us apart, ensuring we can meet even the most unique process requirements.
- Global Reach: As an established lobe pump manufacturer with a global presence, we serve clients across multiple continents, providing localized support and service.
- Quality Assurance: We adhere to stringent quality control measures throughout the manufacturing process, ensuring our lobe pumps meet international standards for performance and reliability.
- After-Sales Support: Our commitment to customer satisfaction extends beyond the sale, with comprehensive after-sales support, including maintenance, repairs, and spare parts availability.
- Competitive Pricing: We offer high-quality lobe pumps at competitive prices, providing excellent value for money without compromising on performance or reliability.
Case Study: Custom Lobe Pump Solution for a Chemical Processing Plant
One of our recent projects involved designing and manufacturing a custom lobe pump for a chemical processing plant in Europe. The client required a pump capable of handling a highly corrosive chemical slurry with a viscosity of 5,000 cP at a flow rate of 50 m³/h and a pressure of 10 bar. The pump needed to operate continuously for 24 hours a day, with minimal downtime for maintenance.
Our engineering team worked closely with the client to understand their specific requirements and challenges. We designed a custom lobe pump featuring:
- A robust casing constructed from Hastelloy C-276, a nickel-based alloy known for its exceptional resistance to corrosion by a wide range of chemicals.
- Specialized lobes with a unique profile to optimize flow and minimize shear, ensuring gentle handling of the slurry.
- A heavy-duty gearbox and motor combination to provide the necessary power and torque for continuous operation.
- Easy-access design for quick and straightforward maintenance, reducing downtime and operational costs.
The custom lobe pump was manufactured, tested, and delivered to the client within the agreed-upon timeline. Since installation, the pump has been operating flawlessly, meeting the client’s production targets and exceeding their expectations for reliability and performance. This project exemplifies our ability to deliver tailored solutions that address our clients’ most challenging fluid handling requirements.
FAQ
What is the typical lifespan of a lobe pump?
The lifespan of a lobe pump depends on various factors, including the materials of construction, the nature of the fluid being pumped, operating conditions, and maintenance practices. With proper maintenance and operation within specified parameters, our lobe pumps can last for many years, often exceeding a decade in service.
Can lobe pumps handle abrasive fluids?
Yes, lobe pumps are well-suited for handling abrasive fluids. The non-contacting design of the lobes minimizes wear and tear, while the choice of materials for the pump casing and internal components can be tailored to resist abrasion. For highly abrasive applications, we recommend selecting hardened materials or coatings to extend the pump’s service life.
What is the maximum viscosity that a lobe pump can handle?
The maximum viscosity that a lobe pump can handle depends on the specific design and size of the pump. Our lobe pumps can handle viscosities ranging from thin liquids to highly viscous slurries, with some models capable of pumping fluids with viscosities exceeding 1,000,000 cP. We can provide detailed specifications and recommendations based on your specific application.
How do I select the right lobe pump for my application?
Selecting the right lobe pump involves considering several factors, including the nature of the fluid being pumped (viscosity, corrosivity, abrasiveness), required flow rate and pressure, operating temperature, and any specific process requirements. Our team of experts can guide you through the selection process, helping you choose the most suitable lobe pump for your needs or designing a custom solution if required.
Summary
As a leading lobe pump manufacturer and supplier, Depampump (Hangzhou) Pump Technology Co., Ltd. is committed to delivering high-quality, reliable fluid handling solutions to industries worldwide. Our comprehensive range of standard and custom lobe pumps, combined with our extensive experience and engineering expertise, enables us to meet the most demanding industrial requirements. Whether you need a pump for chemical processing, oil and gas operations, food production, or any other application, we have the knowledge and capabilities to provide a solution that enhances your process efficiency and reliability. Contact us today to discuss your lobe pump requirements and discover how we can support your business growth.