
In industrial applications requiring precise fluid handling under extreme conditions, high pressure diaphragm reciprocating pumps represent the pinnacle of engineering excellence. As a specialized manufacturer with over two decades of experience, Depamp (Hangzhou) Pump Technology Co., Ltd. has established itself as a global leader in custom-engineered pumping solutions for demanding environments. This comprehensive guide explores the technical specifications, application scenarios, and customization options available for these critical industrial components.
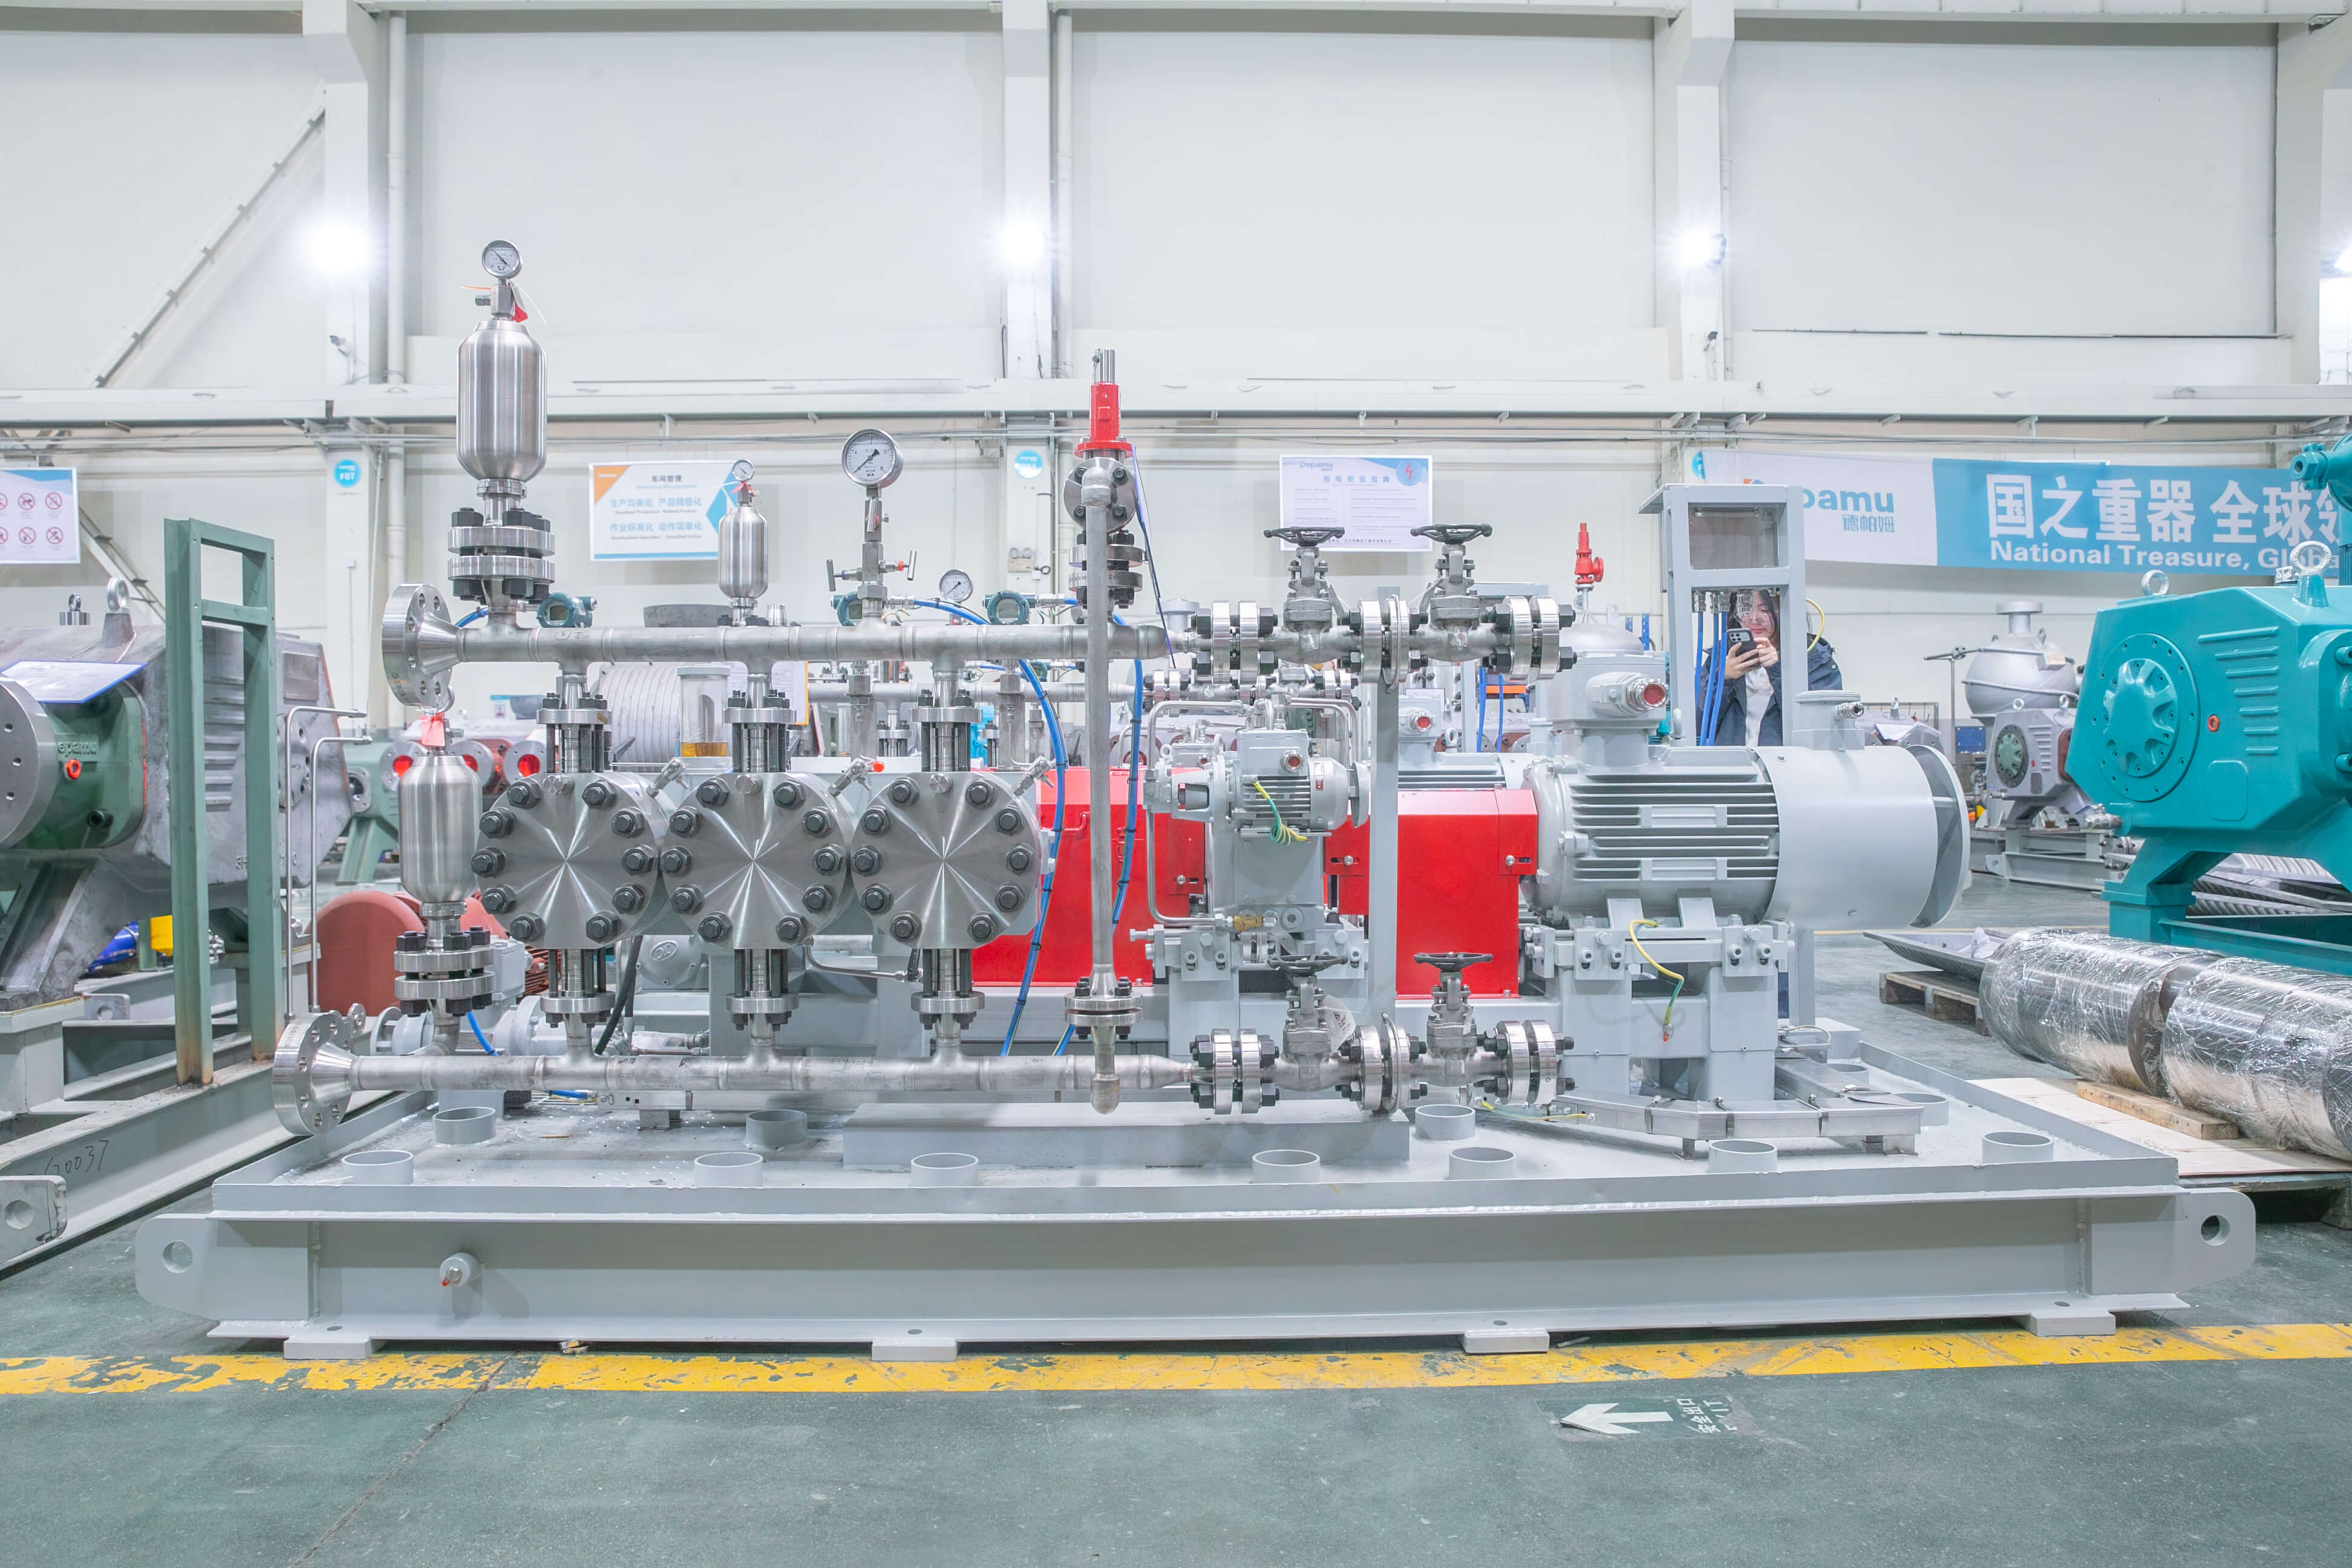
Technical Foundations of High Pressure Diaphragm Pumps
The core innovation of diaphragm reciprocating pumps lies in their unique operating principle that combines the reliability of reciprocating motion with the containment benefits of diaphragm technology. Unlike traditional piston pumps, these systems use a flexible diaphragm to separate the process fluid from the hydraulic mechanism, eliminating internal leaks and cross-contamination risks. This design enables operation with corrosive, abrasive, or hazardous fluids while maintaining precise flow control.
Depamp’s engineering team has perfected this technology through continuous innovation since the company’s founding in 2003. Our current generation of high pressure diaphragm pumps achieves pressure ratings exceeding 35MPa (5,000 psi) while maintaining flow rates from 0.5 to 500 liters per hour. The modular design allows customization of key components including diaphragm materials, valve types, and housing construction to match specific application requirements.
Key technical advantages of our diaphragm pump technology include:
- 100% leak-proof operation through hydraulic diaphragm actuation
- Precision flow control with ±1% accuracy across operating range
- Ability to handle viscosities up to 10,000 cP and temperatures from -40°C to +180°C
- Self-priming capability up to 9 meters without external assistance
- ATEX and API 675 certifications for hazardous environment applications
Industry-Specific Application Solutions
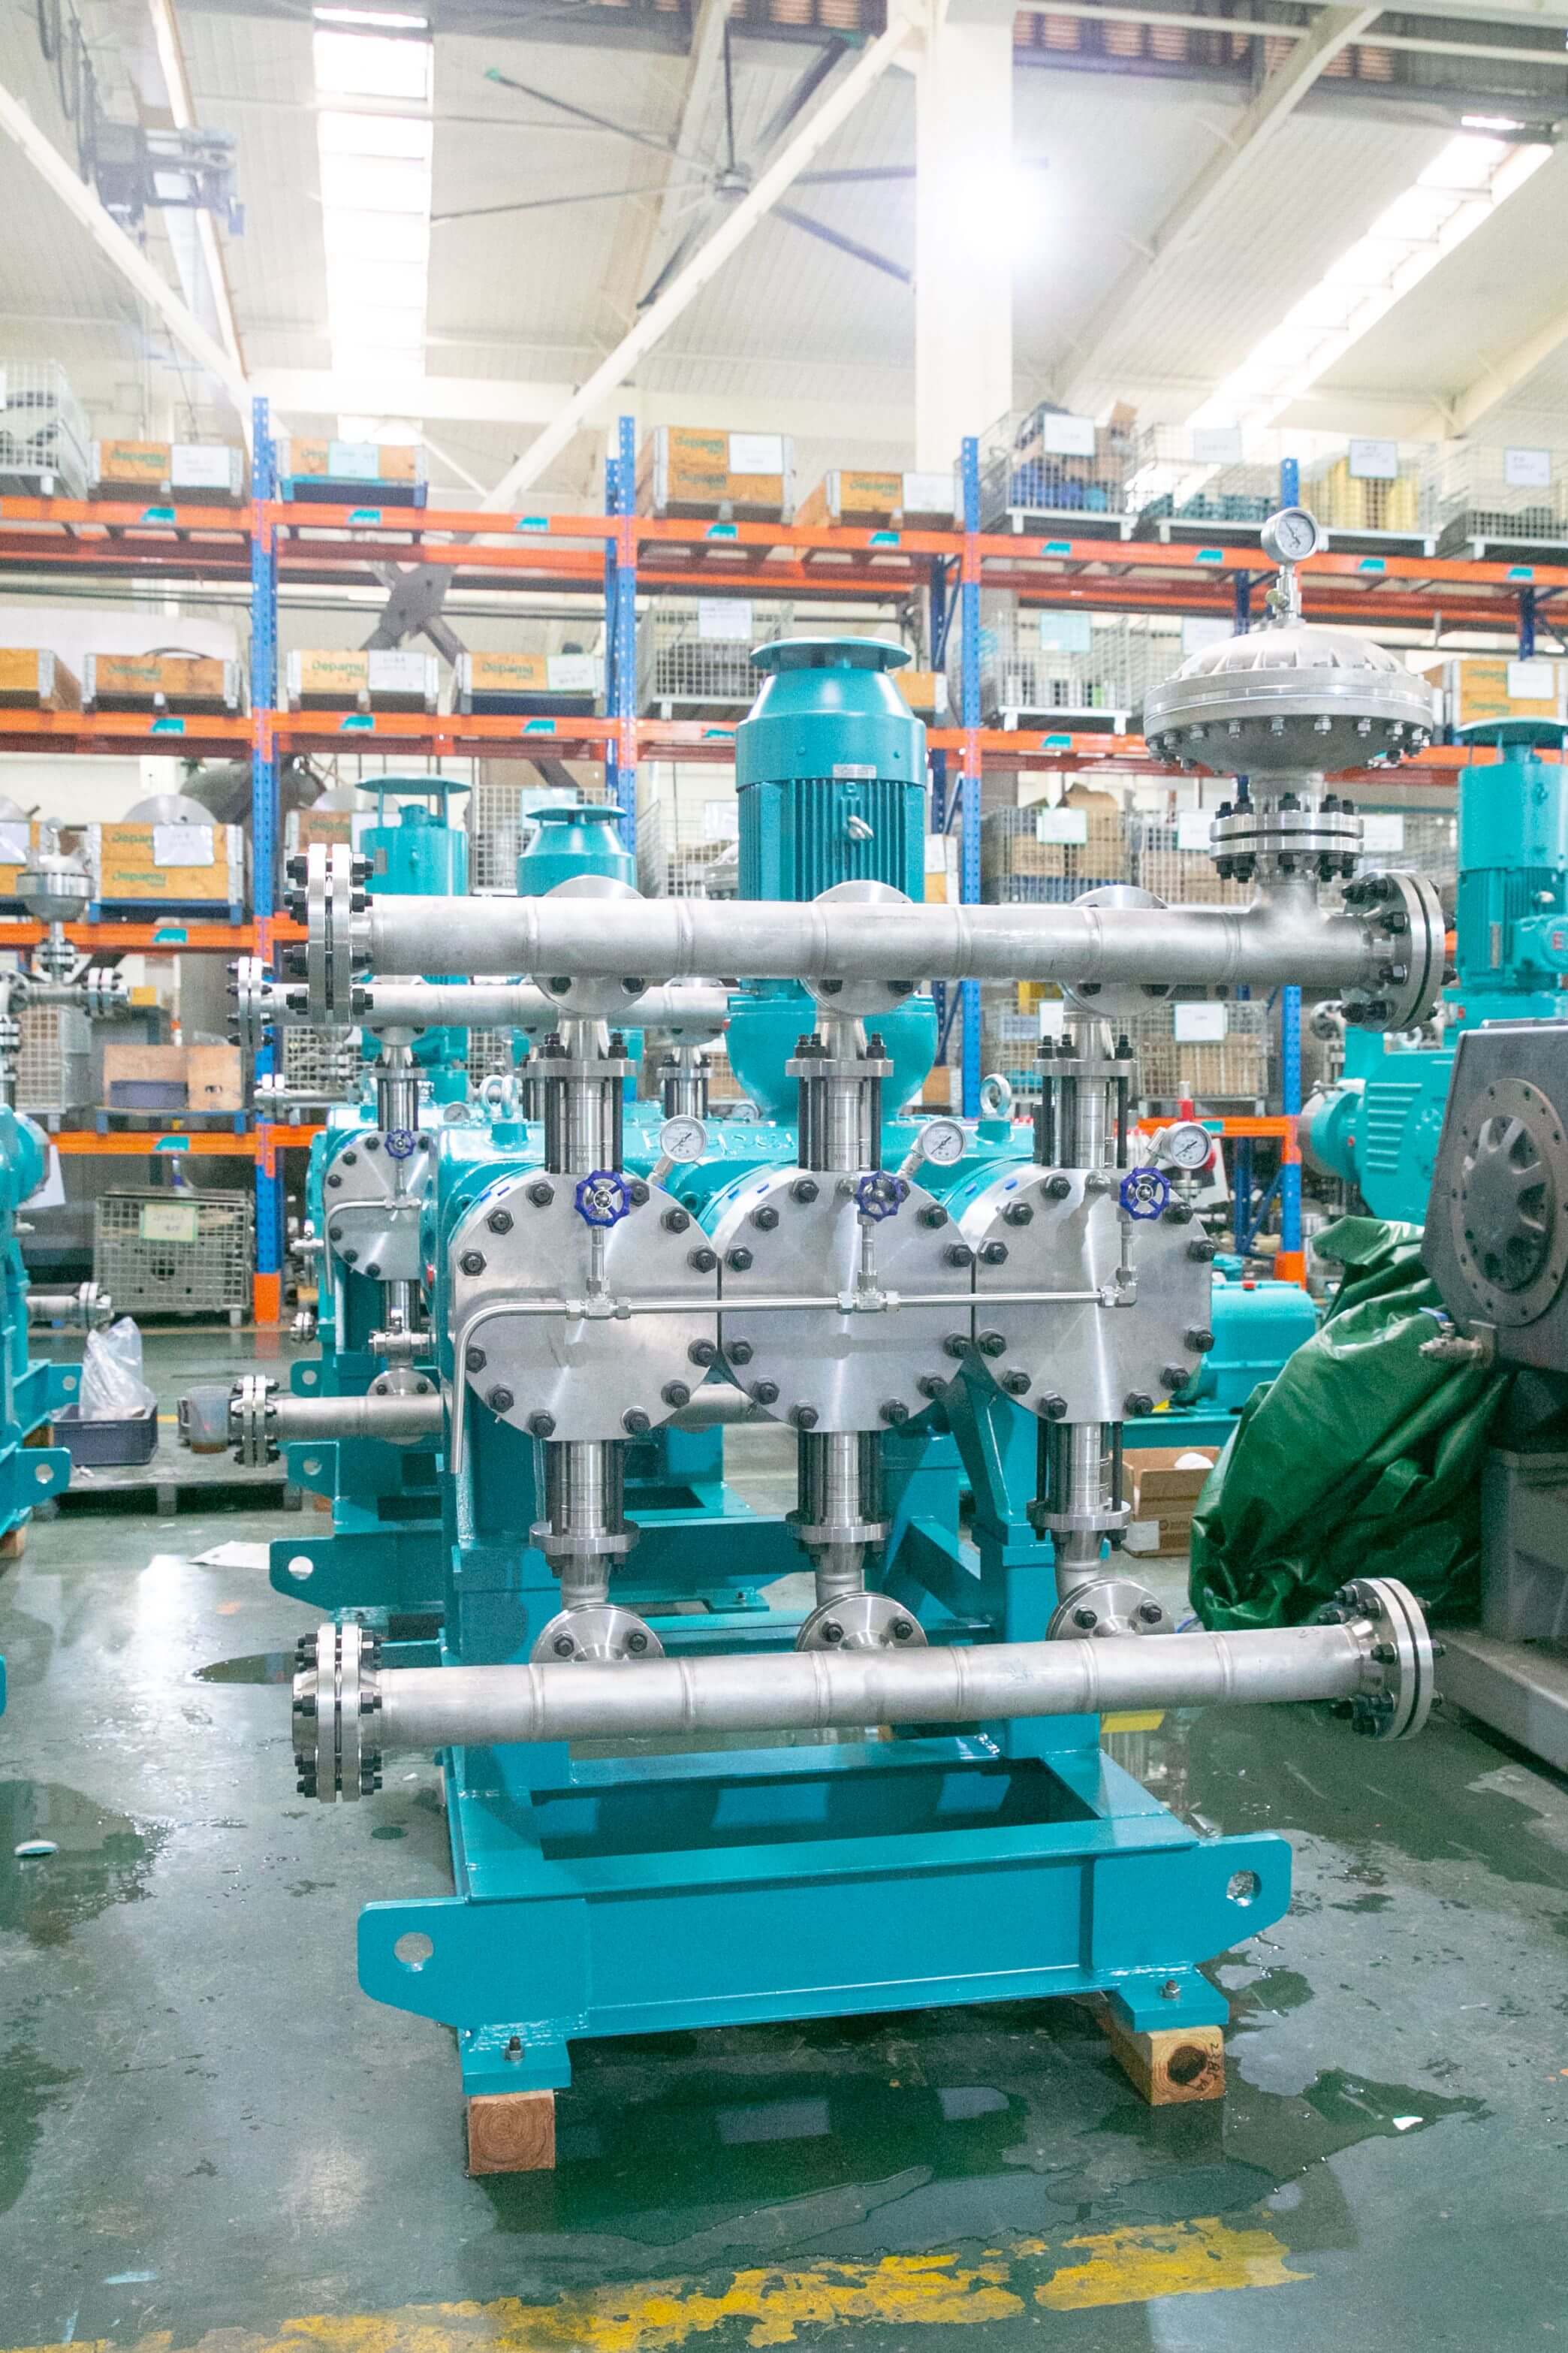
The versatility of high pressure diaphragm pumps makes them essential across multiple industrial sectors. At Depamp, we’ve developed specialized configurations for each application domain, incorporating industry-specific features and certifications. Our engineering team works closely with clients to analyze process requirements and recommend optimal pump configurations.
Petrochemical Processing
In refinery operations, our pumps handle critical chemical injection tasks including catalyst activation, corrosion inhibition, and hydrogen sulfide scavenging. The ability to precisely meter chemicals at pressures up to 35MPa ensures optimal reaction conditions while maintaining safety standards. Specialized materials like Hastelloy C-276 and PTFE enable operation with aggressive chemicals at elevated temperatures.
Oil & Gas Production
For upstream applications, we supply pumps for water injection, chemical EOR (Enhanced Oil Recovery), and well stimulation. Our high pressure models (up to 70MPa) are designed for deep well applications, with compact footprints suitable for offshore platforms. The positive displacement design maintains consistent flow regardless of discharge pressure fluctuations.
Nuclear Power Generation
Nuclear applications demand the highest reliability standards. Our pumps comply with RCC-M and other nuclear industry specifications, featuring redundant diaphragm systems and specialized monitoring for early failure detection. Applications include boron injection, coolant chemistry control, and waste processing systems.
Water Treatment Systems
Municipal and industrial water treatment facilities rely on our pumps for precise dosing of coagulants, flocculants, and disinfectants. The leak-proof design prevents contamination of potable water supplies while maintaining accurate chemical delivery. Stainless steel construction ensures long service life in corrosive environments.
Custom Engineering Capabilities
What truly distinguishes Depamp as a manufacturer is our comprehensive customization capability. With 400+ engineering professionals and 35,000m² production facilities, we can transform standard products into fully customized solutions tailored to specific process requirements. Our customization process follows a structured methodology:
1. Process Analysis: Detailed review of fluid properties, operating parameters, and environmental conditions
2. Material Selection: Choice from 300+ materials including duplex stainless steels, superalloys, and engineered plastics
3. Component Configuration: Customization of diaphragms, valves, seals, and drive systems
4. Safety Integration: Incorporation of pressure relief, leak detection, and containment systems
5. Documentation Package: Complete technical drawings, operation manuals, and certification records
A recent project for a Middle Eastern refinery demonstrates our customization capabilities. The client required a pump system capable of injecting a viscous polymer solution at 25MPa with 0.5% accuracy. Our solution featured:
- Specialized PTFE/glass diaphragm with reinforced construction
- Hydraulic end designed for viscous fluid handling
- Integrated pulse dampener to maintain flow stability
- Explosion-proof motor and control system for Zone 1 hazardous area
- Local and remote monitoring interfaces
Quality Assurance and Certification
As an ISO 9001:2015 certified manufacturer, Depamp maintains rigorous quality control throughout the production process. Each pump undergoes comprehensive testing including:
- Hydrostatic pressure testing to 1.5x maximum operating pressure
- Performance verification under actual process conditions
- Material traceability and NDT (Non-Destructive Testing) inspections
- Functional testing of all safety systems
- Packaging and transportation validation
Our products comply with international standards including API 675, ATEX, CE, and PED. For nuclear applications, we provide documentation packages meeting RCC-M and other industry-specific requirements. The quality assurance system extends to our supply chain, with all critical components sourced from certified suppliers and subjected to incoming inspection.
| Quality Parameter | Testing Method | Acceptance Criteria |
|---|---|---|
| Pressure Rating | Hydrostatic test | 1.5x max operating pressure |
| Flow Accuracy | Gravimetric calibration | ±1% of set point |
| Material Purity | Spectrographic analysis | Meets ASTM specifications |
| Diaphragm Integrity | Helium leak test | 1×10⁻⁹ mbar·l/s |
FAQ
What makes diaphragm pumps suitable for high pressure applications?
Diaphragm pumps achieve high pressure capabilities through their positive displacement design combined with hydraulic amplification. The diaphragm acts as a barrier between the process fluid and hydraulic system, allowing pressure generation without direct contact between moving parts and the handled fluid. This design enables pressure ratings exceeding 35MPa while maintaining leak-proof operation.
How do you ensure chemical compatibility with aggressive fluids?
Our material selection process considers all aspects of chemical compatibility including corrosion resistance, swelling, and permeation. We maintain an extensive database of material performance data and work with leading polymer suppliers to identify optimal solutions. For critical applications, we conduct immersions tests with actual process fluids under operating conditions to validate material selection.
What maintenance is required for high pressure diaphragm pumps?
These pumps require minimal maintenance when properly specified and operated. Typical maintenance includes periodic diaphragm inspection (every 2,000-5,000 operating hours), valve seat replacement, and lubrication of moving parts. Our pumps feature modular designs that allow quick replacement of wear parts without specialized tools. We provide comprehensive maintenance manuals and training programs for customer personnel.
Can you supply pumps for ATEX Zone 0 hazardous areas?
Yes, we have extensive experience supplying pumps for explosive atmospheres. Our ATEX-certified models comply with Directive 2014/34/EU and feature explosion-proof motors, static grounding systems, and containment designs that prevent ignition sources. We can certify pumps for Zone 0, Zone 1, or Zone 2 applications depending on customer requirements.
What lead times should be expected for custom pump orders?
Standard models typically ship within 4-6 weeks of order confirmation. Custom-engineered solutions require additional time for design review, material procurement, and testing. Our average lead time for fully customized pumps is 12-16 weeks, with expedited options available for urgent requirements. We maintain strategic stock of critical components to minimize production delays.
Summary
As a specialized manufacturer of high pressure diaphragm reciprocating pumps, Depamp (Hangzhou) Pump Technology combines technical expertise with manufacturing excellence to deliver solutions for the world’s most demanding industrial applications. Our comprehensive capabilities span from standard product lines to fully customized systems, supported by rigorous quality assurance and global certification standards. With applications across petrochemical, oil & gas, nuclear power, and water treatment industries, we continue to push the boundaries of pumping technology while maintaining our commitment to reliability, safety, and performance.