
When it comes to industrial fluid handling, precision and reliability are non-negotiable. For over two decades, Depamp (Hangzhou) Pump Technology Co., Ltd. has been at the forefront of developing innovative pumping solutions that meet the most demanding requirements across various industries. As a specialized manufacturer of rotary lobe pumps and other volumetric pumps, we understand the critical role these devices play in ensuring smooth operations and optimal productivity.
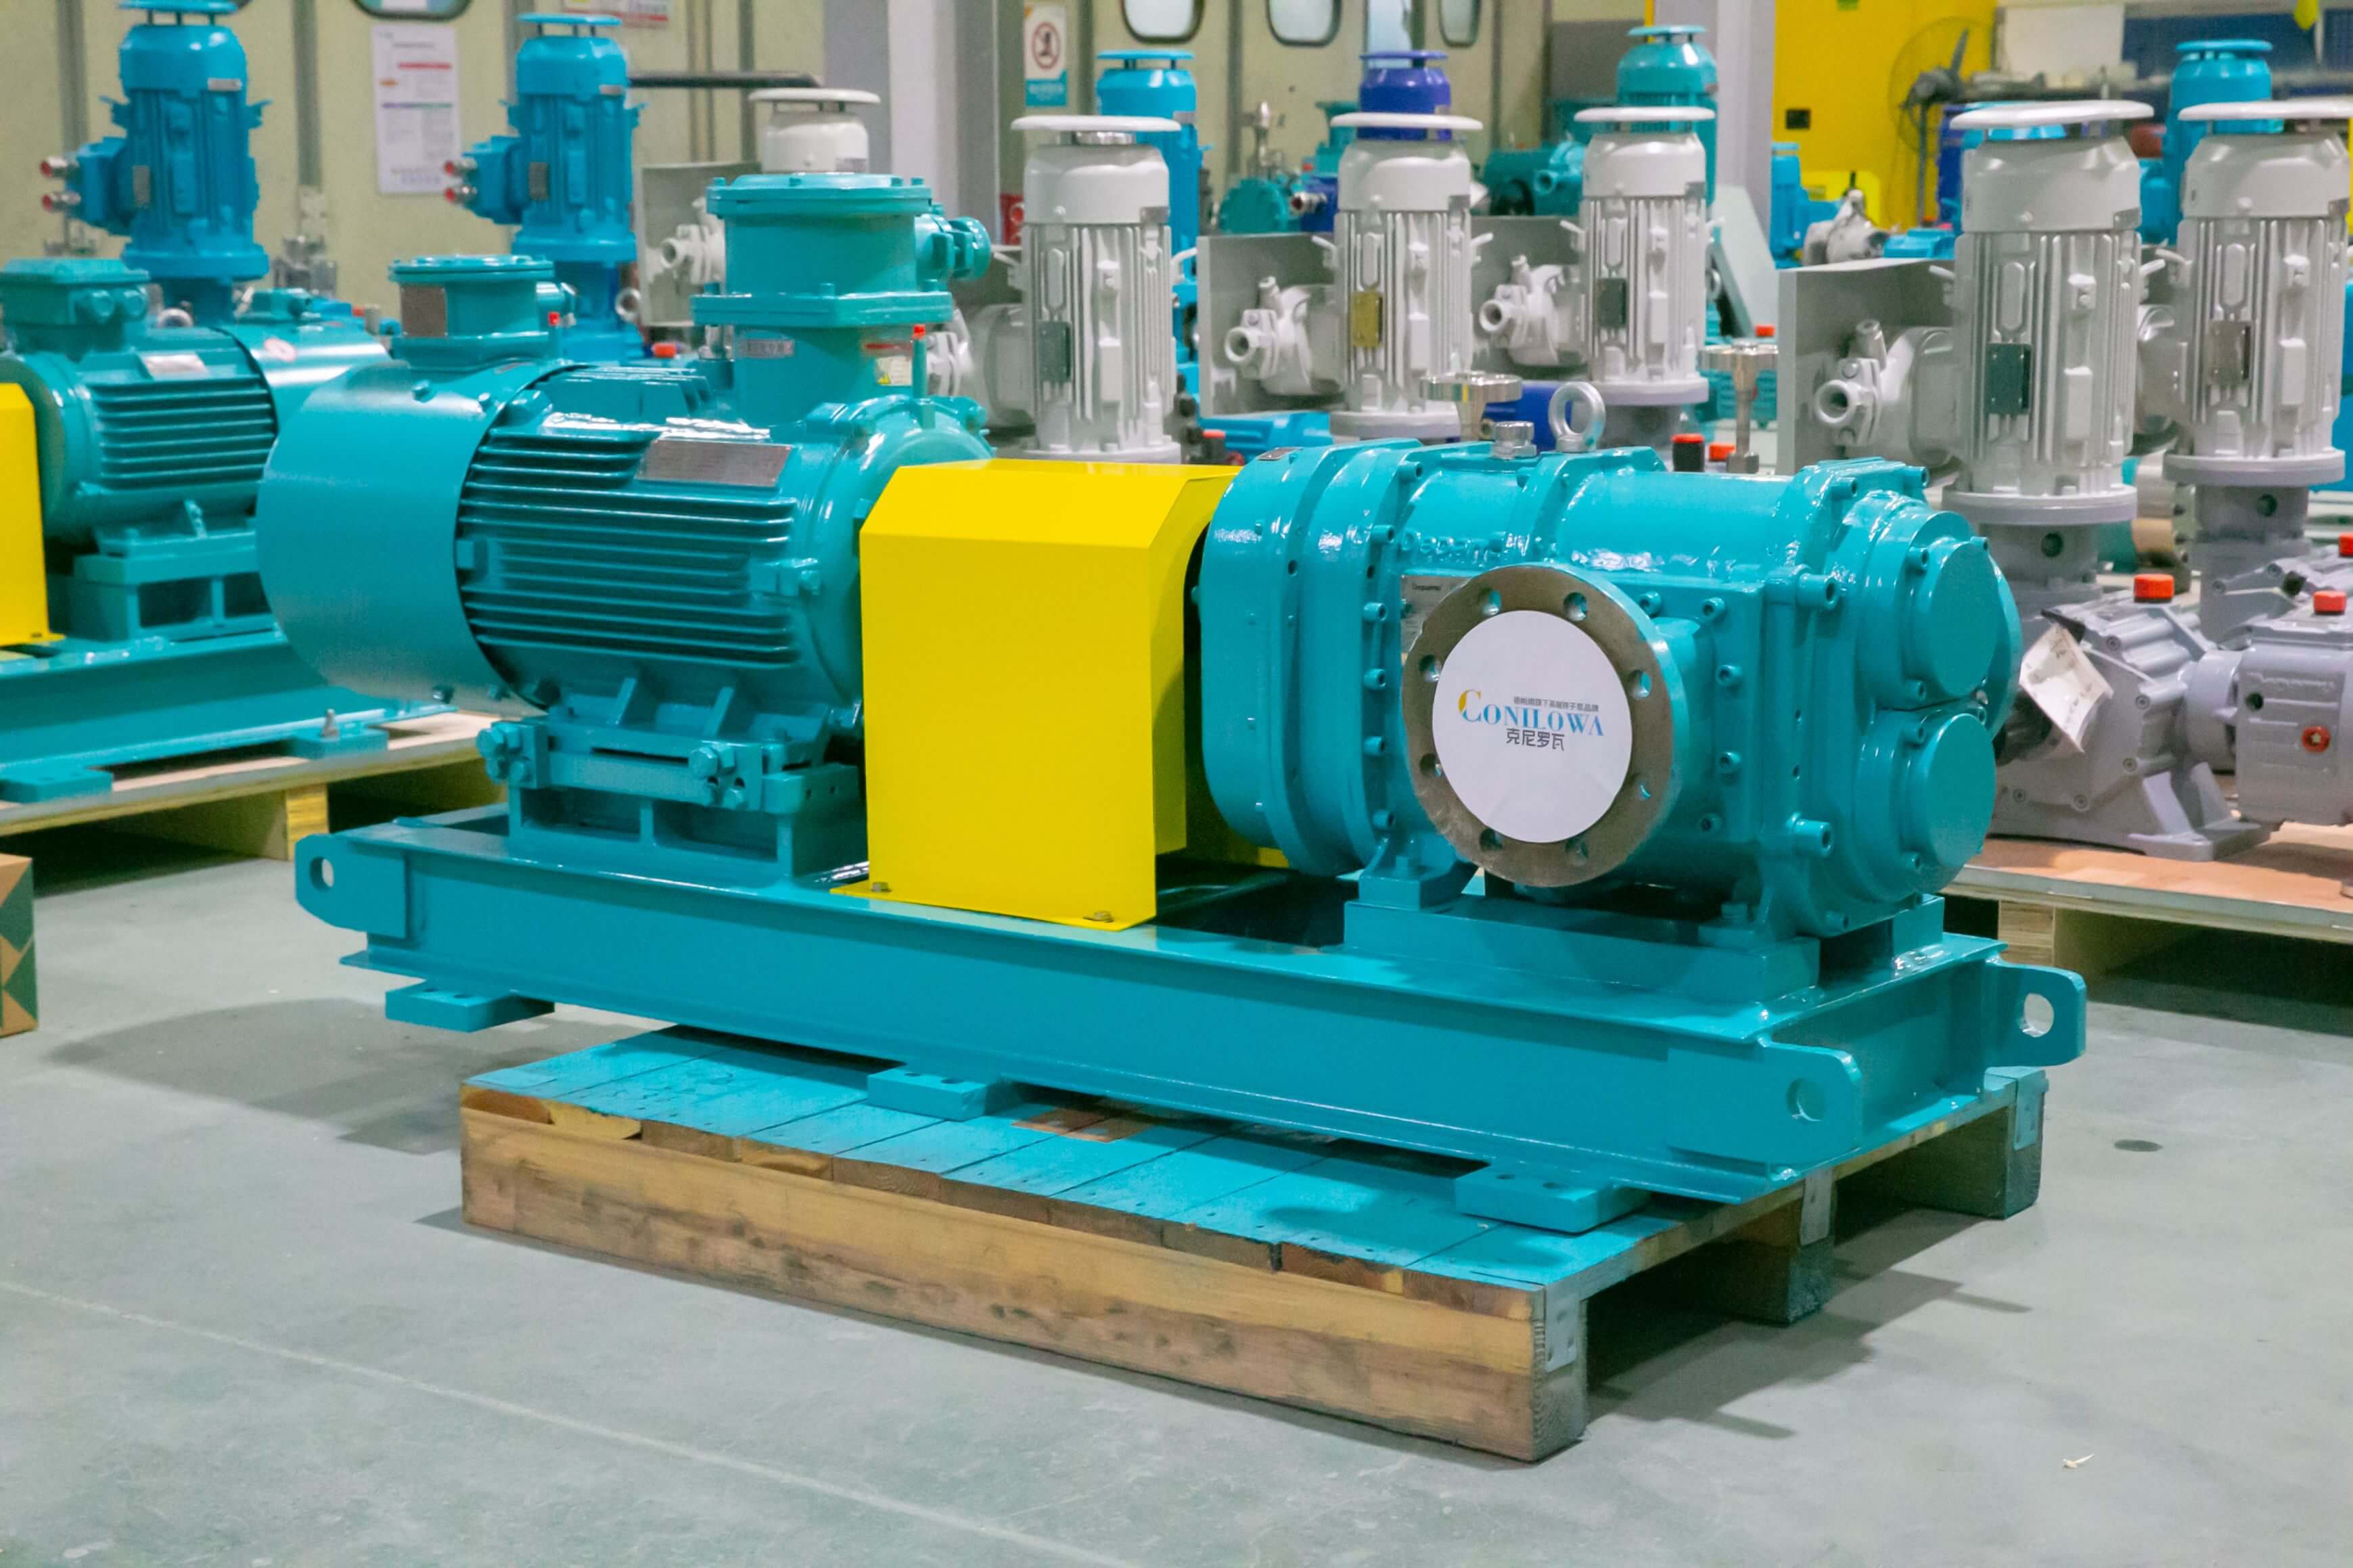
Understanding Rotary Lobe Pumps: The Industrial Workhorse
Rotary lobe pumps, also known as lobe pumps or rotary positive displacement pumps, are versatile machines designed to handle a wide range of fluids – from thin liquids to viscous slurries. These pumps operate through the synchronized rotation of two or more lobes that create expanding and contracting chambers to move fluid through the system. The non-contacting design between lobes ensures gentle handling of shear-sensitive materials while maintaining consistent flow rates.
At Depamp, we’ve engineered our rotary lobe pumps to excel in challenging environments. Our proprietary designs feature precision-machined lobes that maintain optimal clearance throughout their service life, reducing wear and minimizing maintenance requirements. The robust construction with heavy-duty bearings and seals enables our pumps to handle pressures up to 35MPa and temperatures ranging from -40°C to +350°C.
Customized Solutions for Diverse Industrial Applications
What sets Depamp apart as a rotary lobe pump manufacturer is our commitment to providing tailored solutions rather than off-the-shelf products. We recognize that different industries have unique requirements when it comes to fluid handling:
Chemical Processing Industry
In chemical plants, our rotary lobe pumps excel at transferring corrosive chemicals, solvents, and viscous polymers. The hermetic seal design prevents leaks and emissions, ensuring worker safety and environmental compliance. Our pumps can handle fluids with varying viscosities without requiring speed adjustments, maintaining consistent process conditions.
Oil & Gas Sector
For upstream and downstream oil & gas applications, our pumps are engineered to withstand harsh conditions. They’re used for crude oil transfer, cementing operations, and chemical injection in well stimulation processes. The ability to handle abrasive slurries containing sand or proppants makes them ideal for hydraulic fracturing applications.
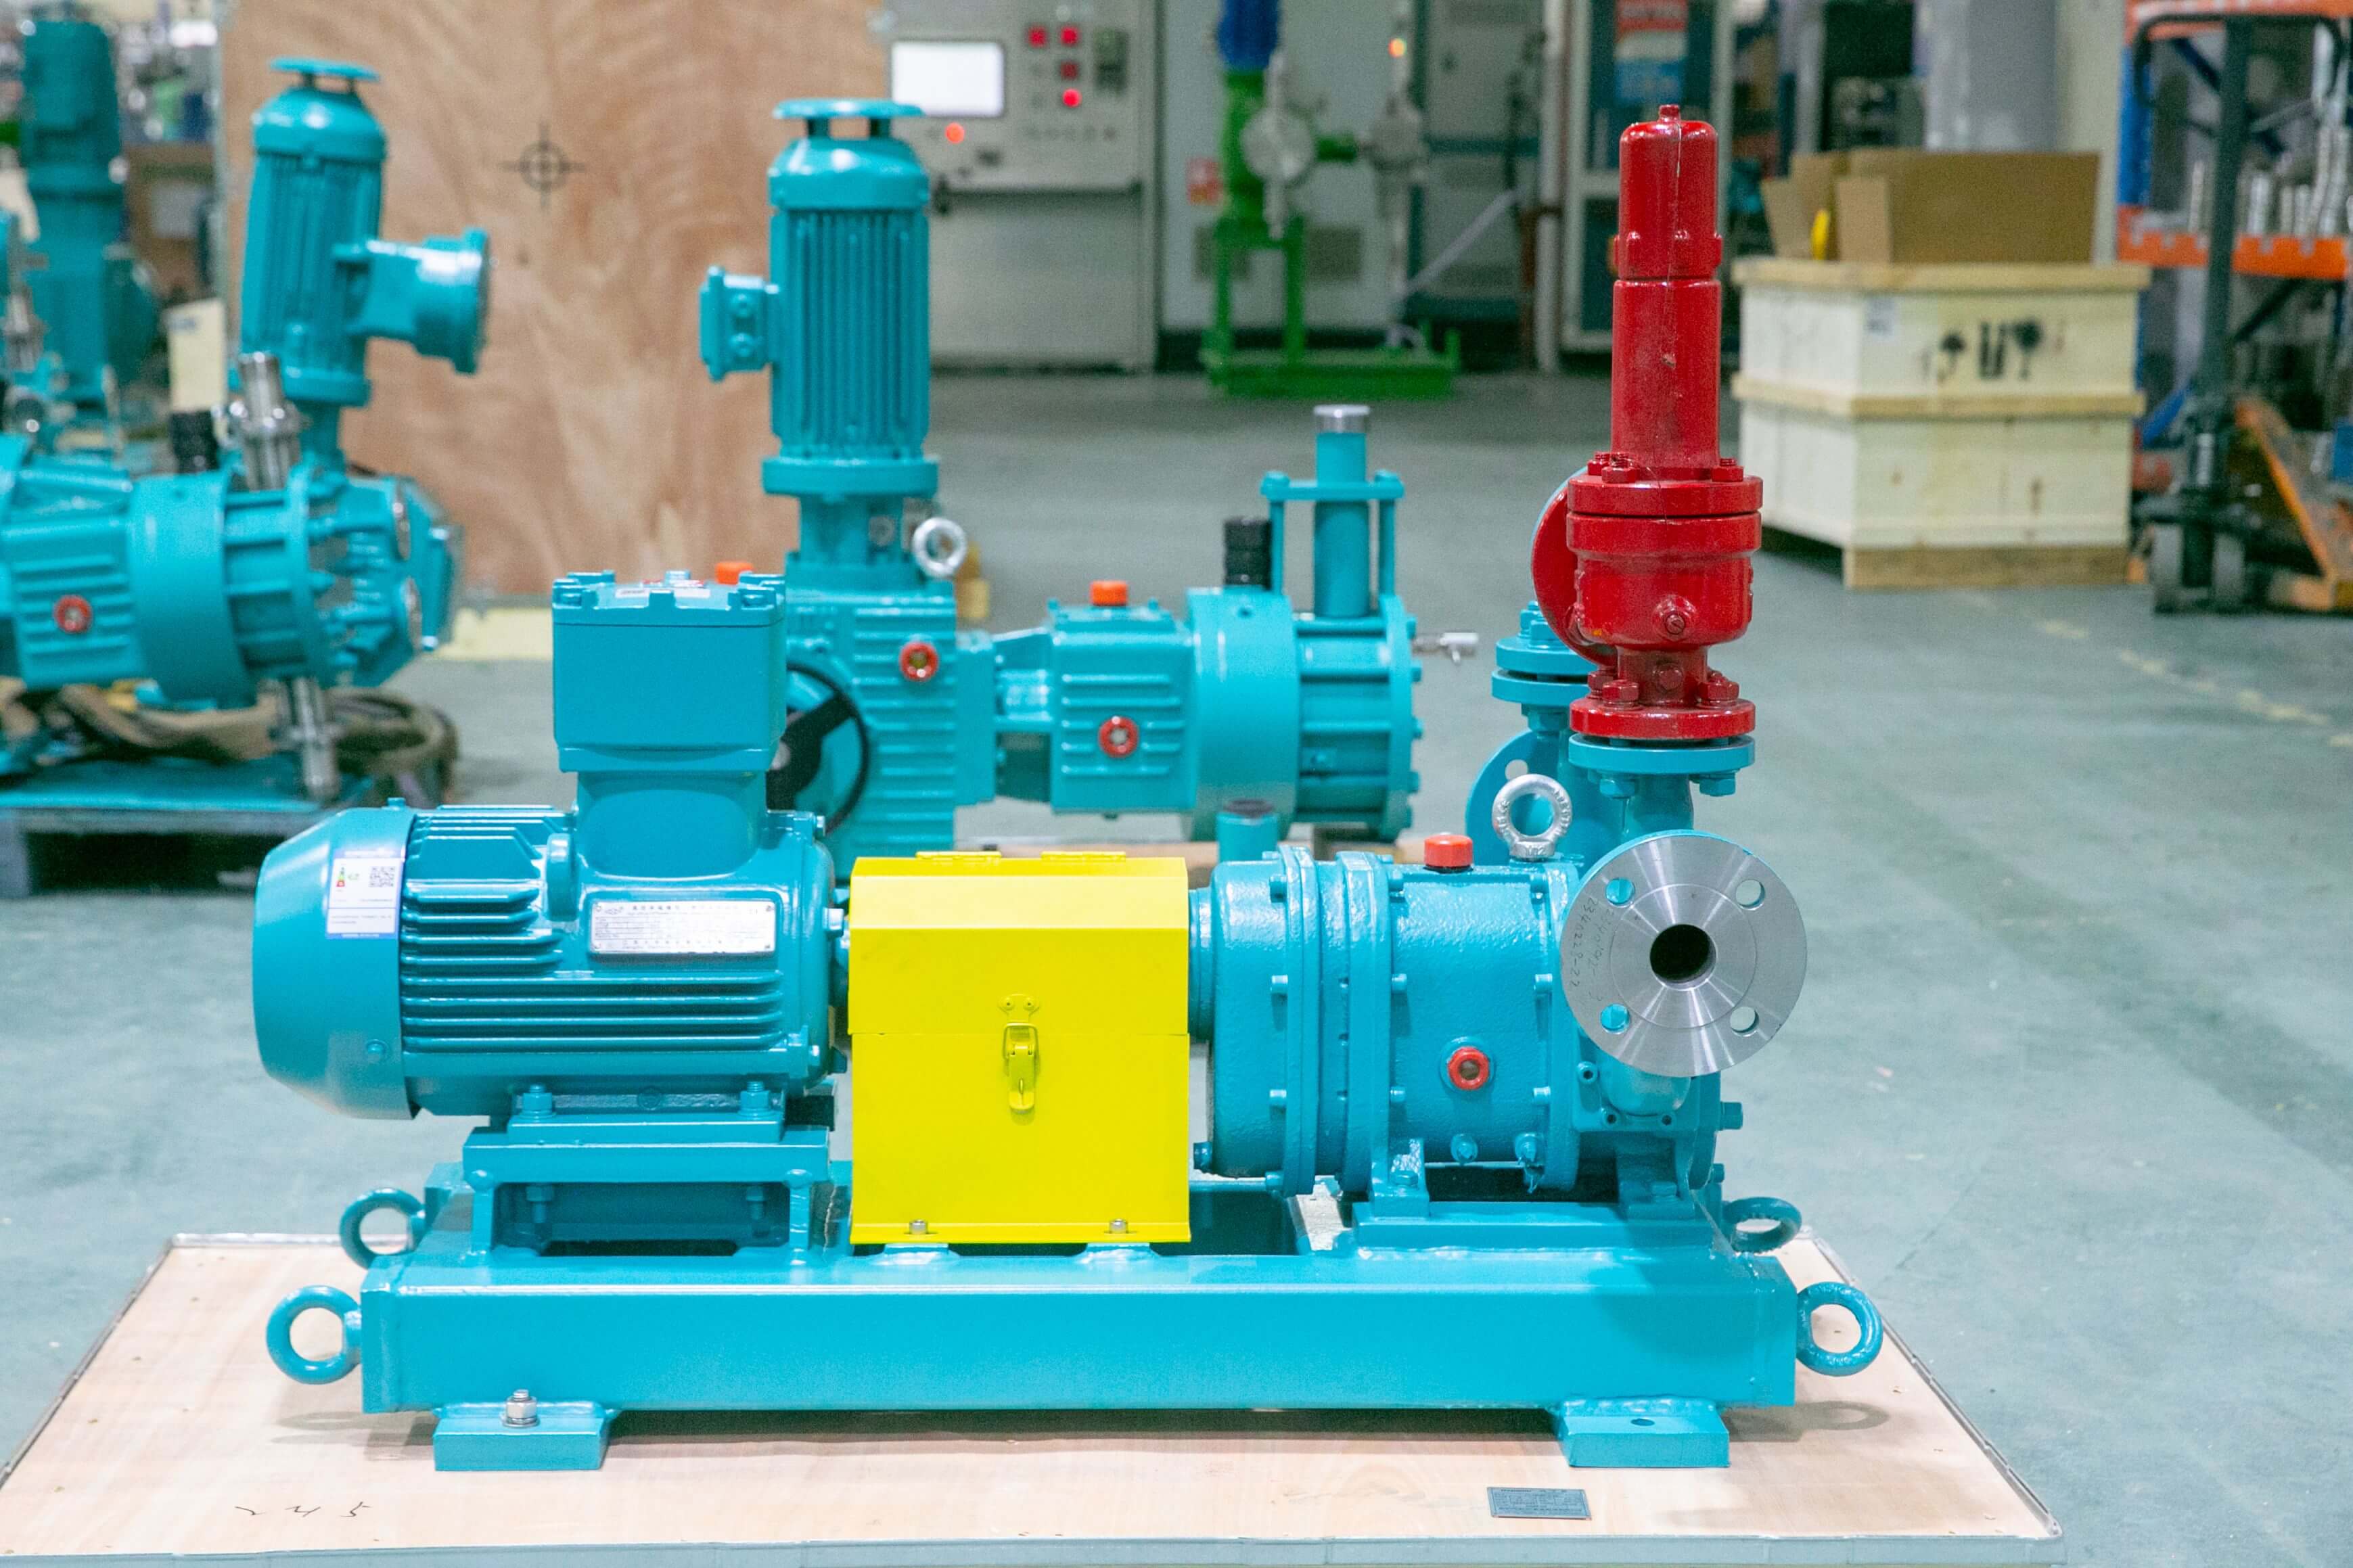
Nuclear Power Industry
Safety is paramount in nuclear facilities, and our rotary lobe pumps meet the stringent requirements for radioactive fluid handling. The all-metal construction with no elastomeric parts eliminates potential contamination risks. Our pumps are used for primary coolant transfer, boron solution injection, and waste processing applications.
Food & Beverage Production
In hygienic applications, we offer rotary lobe pumps with sanitary designs that comply with 3A, EHEDG, and FDA standards. The smooth internal surfaces prevent bacterial growth, while the gentle pumping action preserves product integrity. These pumps are used for transferring milk, yogurt, syrups, and other viscous food products.
Key Features of Depamp Rotary Lobe Pumps
When you choose Depamp as your rotary lobe pump supplier, you benefit from several advanced features that enhance performance and reliability:
- Precision-engineered lobes: Our proprietary manufacturing process ensures consistent lobe profiles for optimal volumetric efficiency
- Multiple lobe configurations: Choose from bi-lobe, tri-lobe, or multi-lobe designs based on your specific application requirements
- Advanced sealing systems:
- Corrosion-resistant materials: Pumps constructed from stainless steel, duplex steel, or special alloys for harsh chemical environments
- Variable speed drives: Optional VFD packages allow precise flow control and energy savings
- Easy maintenance design: Front-loading seal cartridges and quick-access covers simplify service procedures
Mechanical seals, packing glands, or magnetic couplings available to prevent leaks in various operating conditions
Technical Specifications Comparison
Our rotary lobe pumps come in various sizes and configurations to match your specific needs. Here’s a comparison of key technical parameters:
| Parameter | Standard Range | High-Pressure Variant | Sanitary Version |
|---|---|---|---|
| Flow Rate | 0.5-2000 m³/h | 1-500 m³/h | 0.2-300 m³/h |
| Pressure | Up to 12 bar | Up to 35 bar | Up to 8 bar |
| Temperature | -40°C to +200°C | -20°C to +350°C | -10°C to +150°C |
| Viscosity | Up to 1,000,000 cP | Up to 500,000 cP | Up to 200,000 cP |
FAQ
What makes Depamp’s rotary lobe pumps different from other manufacturers?
Our competitive edge comes from three key factors: First, our vertical integration allows complete control over the manufacturing process from raw materials to final assembly. Second, we invest heavily in R&D to continuously improve pump efficiency and reliability. Third, our customization capability ensures we can adapt pumps to specific customer requirements rather than offering one-size-fits-all solutions.
How do I select the right rotary lobe pump for my application?
The selection process involves evaluating several parameters: fluid properties (viscosity, temperature, corrosiveness), required flow rate and pressure, suction conditions, and any special requirements like ATEX certification or sanitary design. Our application engineers can guide you through this process and recommend the optimal pump configuration based on your specific needs.
What maintenance is required for rotary lobe pumps?
Regular maintenance includes checking and replacing seals as needed, monitoring bearing condition, and verifying lobe clearance. Our pumps are designed for easy maintenance with front-loading seal cartridges and quick-access covers. We provide detailed maintenance manuals and can train your personnel on proper service procedures. Many customers report service intervals of 12-24 months under normal operating conditions.
Can rotary lobe pumps handle abrasive fluids?
Yes, our pumps can be configured for abrasive service by selecting appropriate materials for lobes and casings (such as hardened stainless steel or special alloys), optimizing lobe clearance, and using robust sealing systems. For extremely abrasive applications, we may recommend a reduced operating speed to extend component life.
What are the advantages of rotary lobe pumps over other positive displacement pumps?
Compared to gear pumps, rotary lobe pumps offer smoother flow with less pulsation and can handle larger solids. Unlike peristaltic pumps, they don’t require frequent tube replacements and can achieve higher pressures. Compared to diaphragm pumps, they provide continuous flow (rather than pulsating) and can handle higher viscosities. The non-contacting lobe design also means less wear and longer service life in most applications.
Summary
Choosing the right rotary lobe pump manufacturer is crucial for ensuring reliable operation and minimizing lifecycle costs in your industrial processes. Depamp (Hangzhou) Pump Technology Co., Ltd. combines decades of experience with continuous innovation to deliver pumping solutions that meet the most demanding requirements across various industries. Our state-of-the-art manufacturing facility, comprehensive quality control system, and customer-centric approach make us the preferred partner for companies seeking high-performance, customized rotary lobe pumps.
Whether you need a standard pump for general industrial use or a specialized solution for challenging applications in chemical processing, oil & gas, nuclear power, or food production, we have the expertise and capabilities to deliver. Contact our technical sales team today to discuss your specific requirements and discover how our rotary lobe pumps can optimize your fluid handling operations.