
When it comes to industrial fluid handling, lobe pumps stand out as versatile, reliable solutions for challenging applications. As a leading manufacturer with over two decades of expertise, Depamump (Hangzhou) Pump Technology Co., Ltd. has established itself as a global innovator in lobe pump technology. This comprehensive guide explores our lobe pump capabilities, applications, and why we’re the preferred choice for industries worldwide.
Understanding Lobe Pump Technology
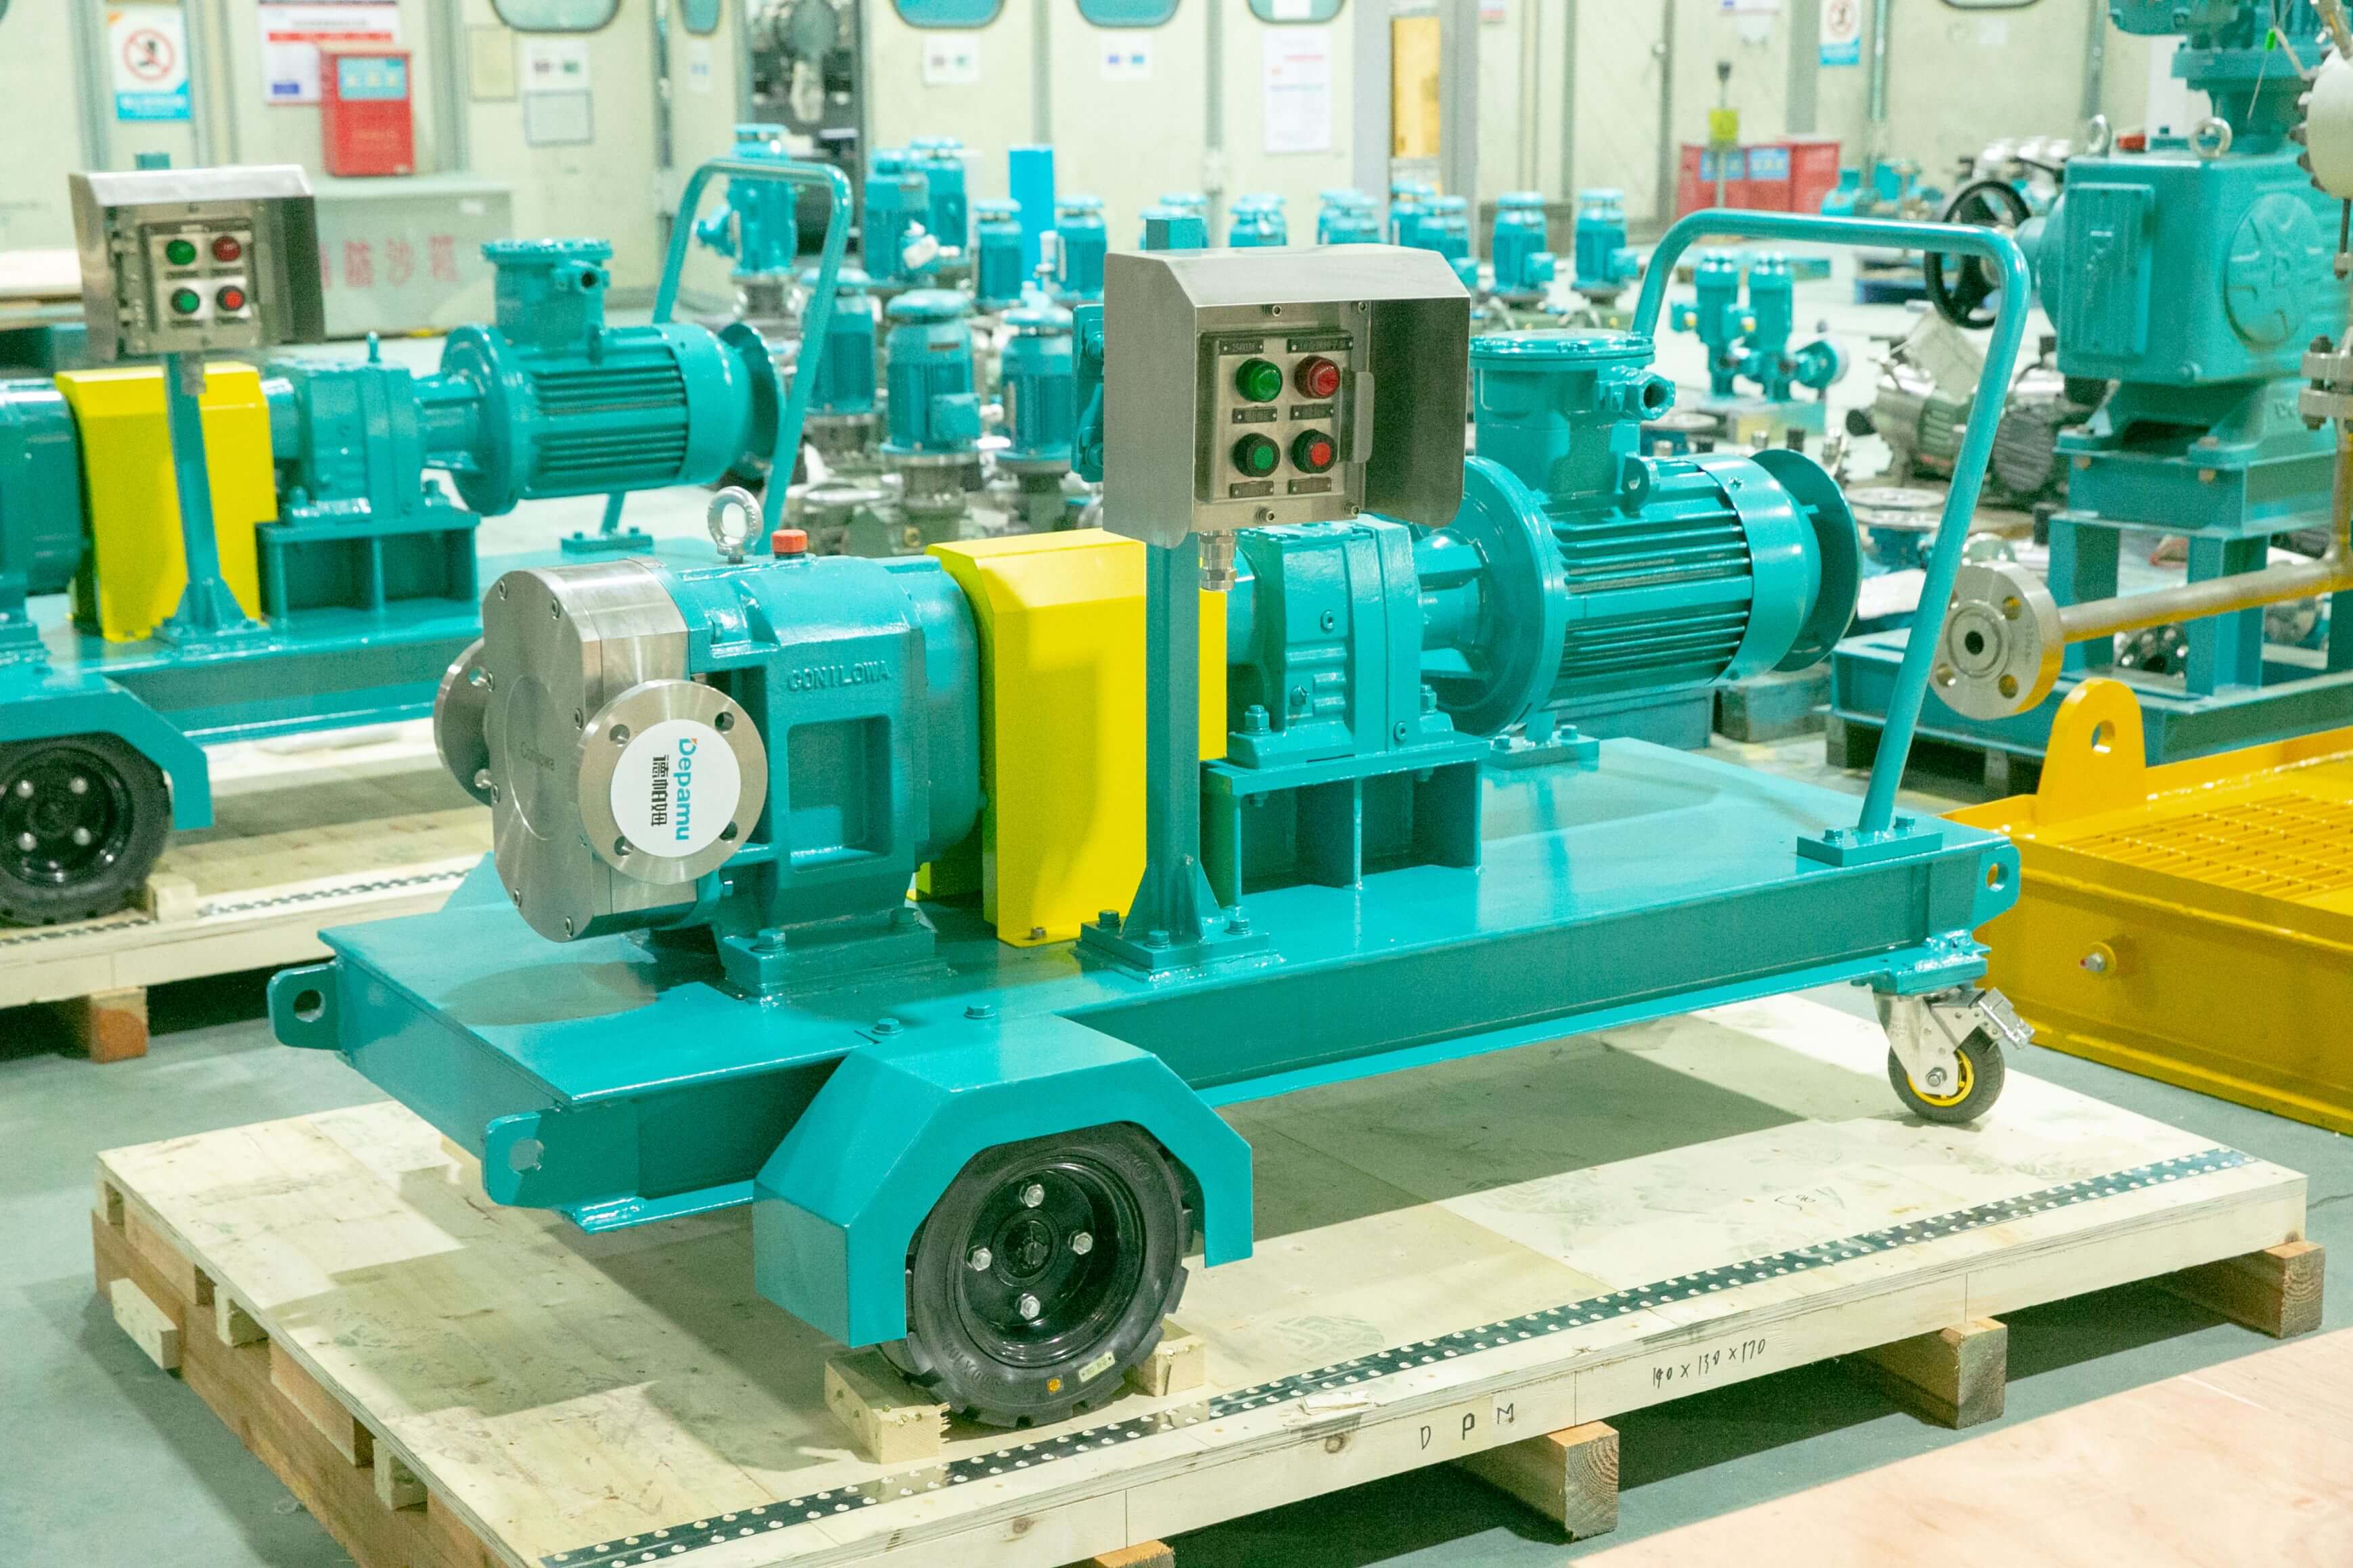
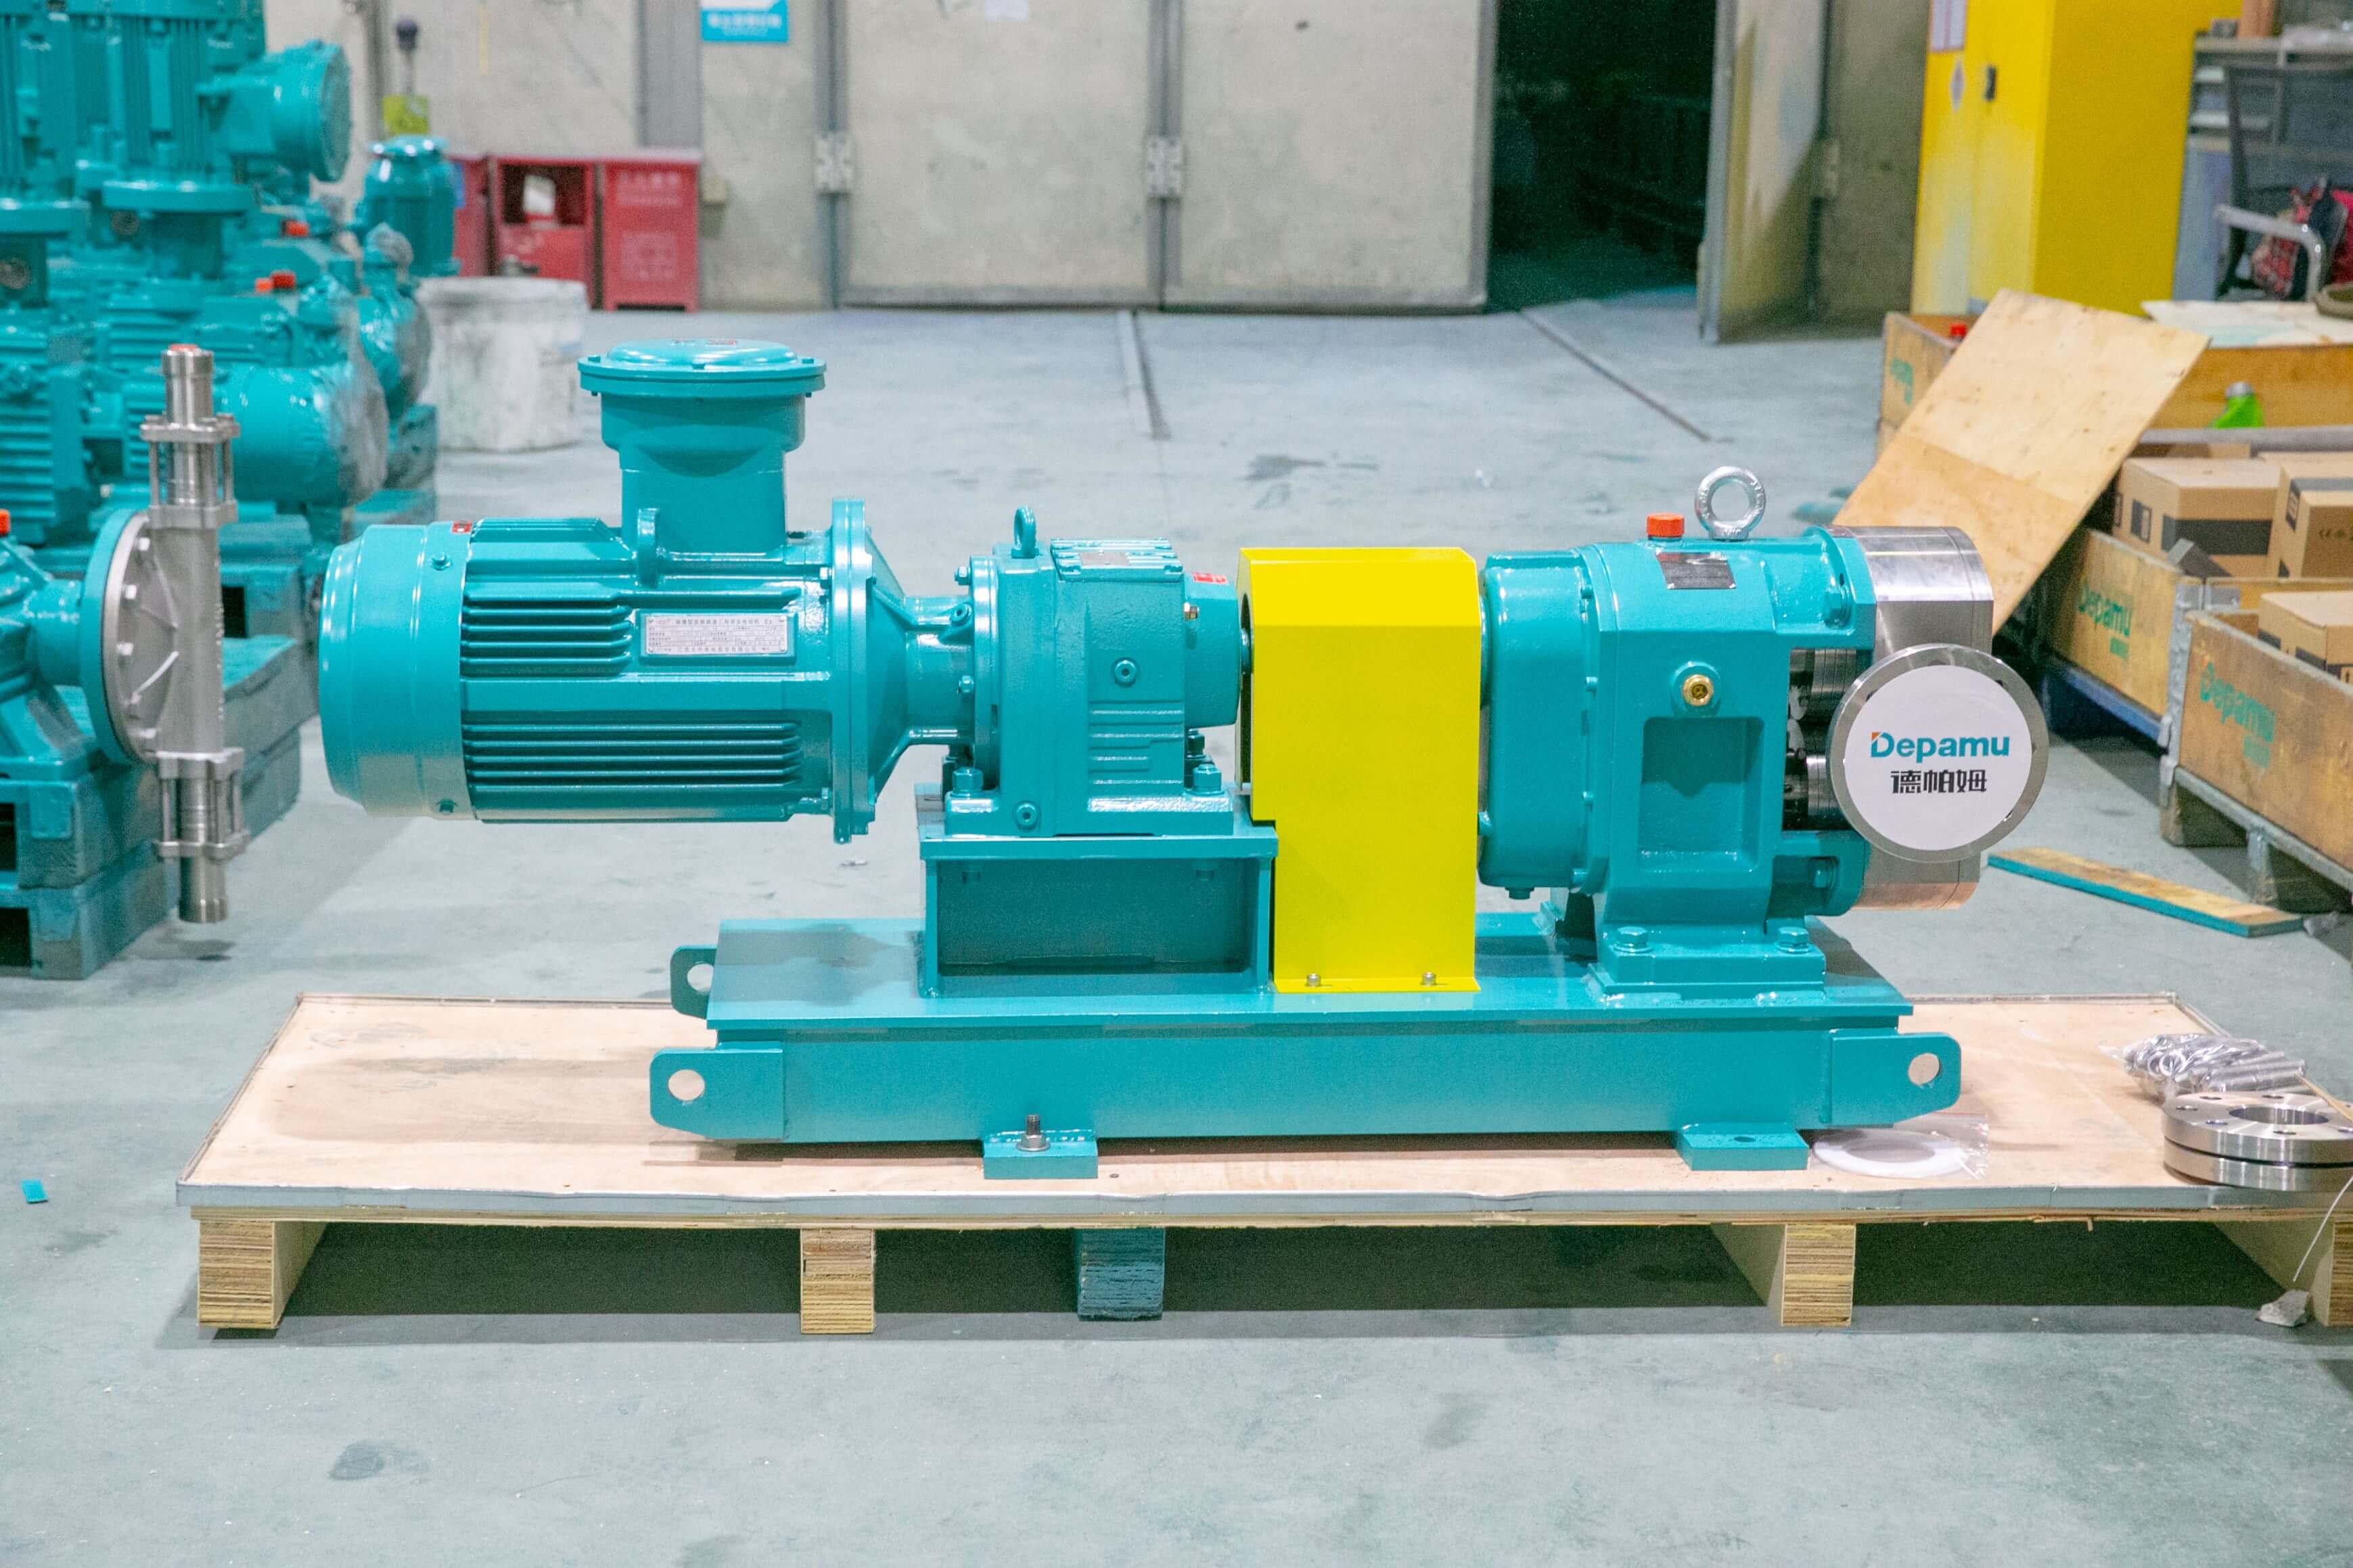
Lobe pumps belong to the positive displacement pump family, operating through the rotation of two or more lobes that mesh together without touching. This design creates a consistent volume displacement with each rotation, making lobe pumps ideal for applications requiring precise flow control and gentle product handling. Our lobe pumps feature:
- High efficiency across varying viscosities (from thin liquids to 1,000,000 cSt)
- Gentle pumping action that preserves product integrity
- Self-priming capabilities up to 9 meters
- Dry running tolerance for short periods
- Reversible flow direction
- CIP (Clean-in-Place) compatible designs
The core advantage of lobe pumps lies in their ability to handle complex fluids without damage or degradation. This makes them invaluable in industries where product quality must be maintained throughout the pumping process.
Industrial Applications of Lobe Pumps
Our lobe pumps serve diverse industries with specialized requirements:
Petrochemical & Refining
In petrochemical plants, lobe pumps transfer viscous crude oil, bitumen, and various chemical additives with precision. Their ability to maintain consistent flow under high pressure conditions makes them essential for catalyst loading and unloading operations.
Food & Beverage Processing
The food industry demands sanitary pumping solutions that won’t compromise product quality. Our lobe pumps feature FDA-compliant materials and crevice-free designs that prevent bacterial growth, making them perfect for:
- Yogurt and dairy product transfer
- Tomato paste and fruit concentrate handling
- Chocolate and confectionery production
- Meat emulsions and pet food processing
Pharmaceutical Manufacturing
Pharmaceutical applications require pumps that can handle sensitive formulations without contamination. Our lobe pumps provide sterile transfer solutions for:
- Active pharmaceutical ingredients (APIs)
- Ointments and creams
- Vaccine production
- Biotech process fluids
Wastewater Treatment
Municipal and industrial wastewater facilities rely on lobe pumps for their ability to handle sludge, screenings, and various chemicals. The robust construction withstands abrasive particles while maintaining reliable performance.
Custom Lobe Pump Solutions
At Depamump, we understand that one size doesn’t fit all. Our engineering team specializes in creating customized lobe pump solutions tailored to your specific requirements:
| Customization Option | Available Features |
|---|---|
| Materials of Construction | Stainless steel 304/316, Duplex steel, Hastelloy, PTFE lined, etc. |
| Sealing Options | Mechanical seals, lip seals, magnetic drive, gland packing |
| Port Configurations | Side, top, or bottom inlet/outlet; multiple ports available |
| Heating/Cooling Jackets | Steam, thermal oil, or electric heating options |
| Drive Options | Electric motor, diesel engine, hydraulic, or pneumatic drives |
| Control Systems | Variable frequency drives (VFD), PLC integration, remote monitoring |
Our customization process begins with a thorough analysis of your application parameters including fluid properties, process conditions, and operational requirements. This ensures we deliver a lobe pump that optimizes performance while minimizing maintenance needs.
Why Choose Depamump for Lobe Pumps?
Several factors distinguish us as a premier lobe pump manufacturer:
1. Engineering Excellence
With 400+ employees including 50+ dedicated R&D professionals, we maintain cutting-edge manufacturing facilities spanning 35,000 square meters. Our annual production capacity exceeds 20,000 units, ensuring timely delivery even for large-scale projects.
2. Quality Assurance
We adhere to stringent international standards including ISO 9001, ISO 14001, and OHSAS 18001. Each lobe pump undergoes rigorous testing before shipment, including:
- Hydrostatic pressure testing up to 1.5x maximum working pressure
- Performance testing for flow rate, pressure, and power consumption
- Noise and vibration analysis
- Material composition verification
3. Global Reach
Our products serve clients in 60+ countries across petrochemical, chemical, power, metallurgy, new energy, environmental protection, new materials, and food industries. This international presence gives us unique insights into diverse application requirements.
4. Comprehensive Support
We provide more than just equipment – we offer complete solutions. Our services include:
- On-site installation and commissioning
- Operator training programs
- Preventive maintenance schedules
- 24/7 technical support hotline
- Spare parts inventory management
FAQ
What makes lobe pumps suitable for high-viscosity applications?
Lobe pumps excel with viscous fluids because their positive displacement design maintains consistent flow regardless of viscosity changes. The clearances between lobes and casing can be precisely engineered to handle fluids up to 1,000,000 cSt without slippage or degradation.
How do lobe pumps compare to gear pumps for chemical processing?
While both are positive displacement pumps, lobe pumps offer several advantages for chemical applications: they generate lower shear forces, handle solids better, and have simpler maintenance requirements. The non-contacting lobe design also eliminates metal-to-metal contact, reducing contamination risks.
Can lobe pumps handle abrasive slurries?
Yes, when properly specified. We offer hardened materials like duplex stainless steel or ceramic-lined lobes for abrasive applications. Proper speed selection and consideration of particle size distribution are critical for maximizing pump life in these conditions.
What maintenance is required for industrial lobe pumps?
Regular maintenance includes checking and replacing mechanical seals as needed, inspecting lobes and casing for wear, verifying alignment, and lubricating bearings. Our pumps are designed for easy disassembly, reducing downtime during maintenance. We recommend establishing a preventive maintenance schedule based on your specific operating conditions.
Summary
Depamump’s lobe pumps represent the pinnacle of industrial fluid handling technology, combining precision engineering with robust construction. Whether you require standard models or fully customized solutions, our team delivers pumps that optimize performance, reliability, and total cost of ownership across diverse applications. With over two decades of expertise and a global client base, we’re positioned to solve your most challenging pumping requirements while providing exceptional support throughout the equipment lifecycle.