
When it comes to industrial fluid handling, rotary lobe pumps stand out as versatile workhorses capable of managing a wide range of challenging applications. As a key product in Depamump’s comprehensive portfolio of positive displacement pumps, our rotary lobe pumps have earned global recognition for their reliability, precision, and ability to handle complex media under demanding conditions. This comprehensive guide explores everything you need to know about rotary lobe pumps – from their working principles to selection criteria, application scenarios, and how to identify the most reliable manufacturers.
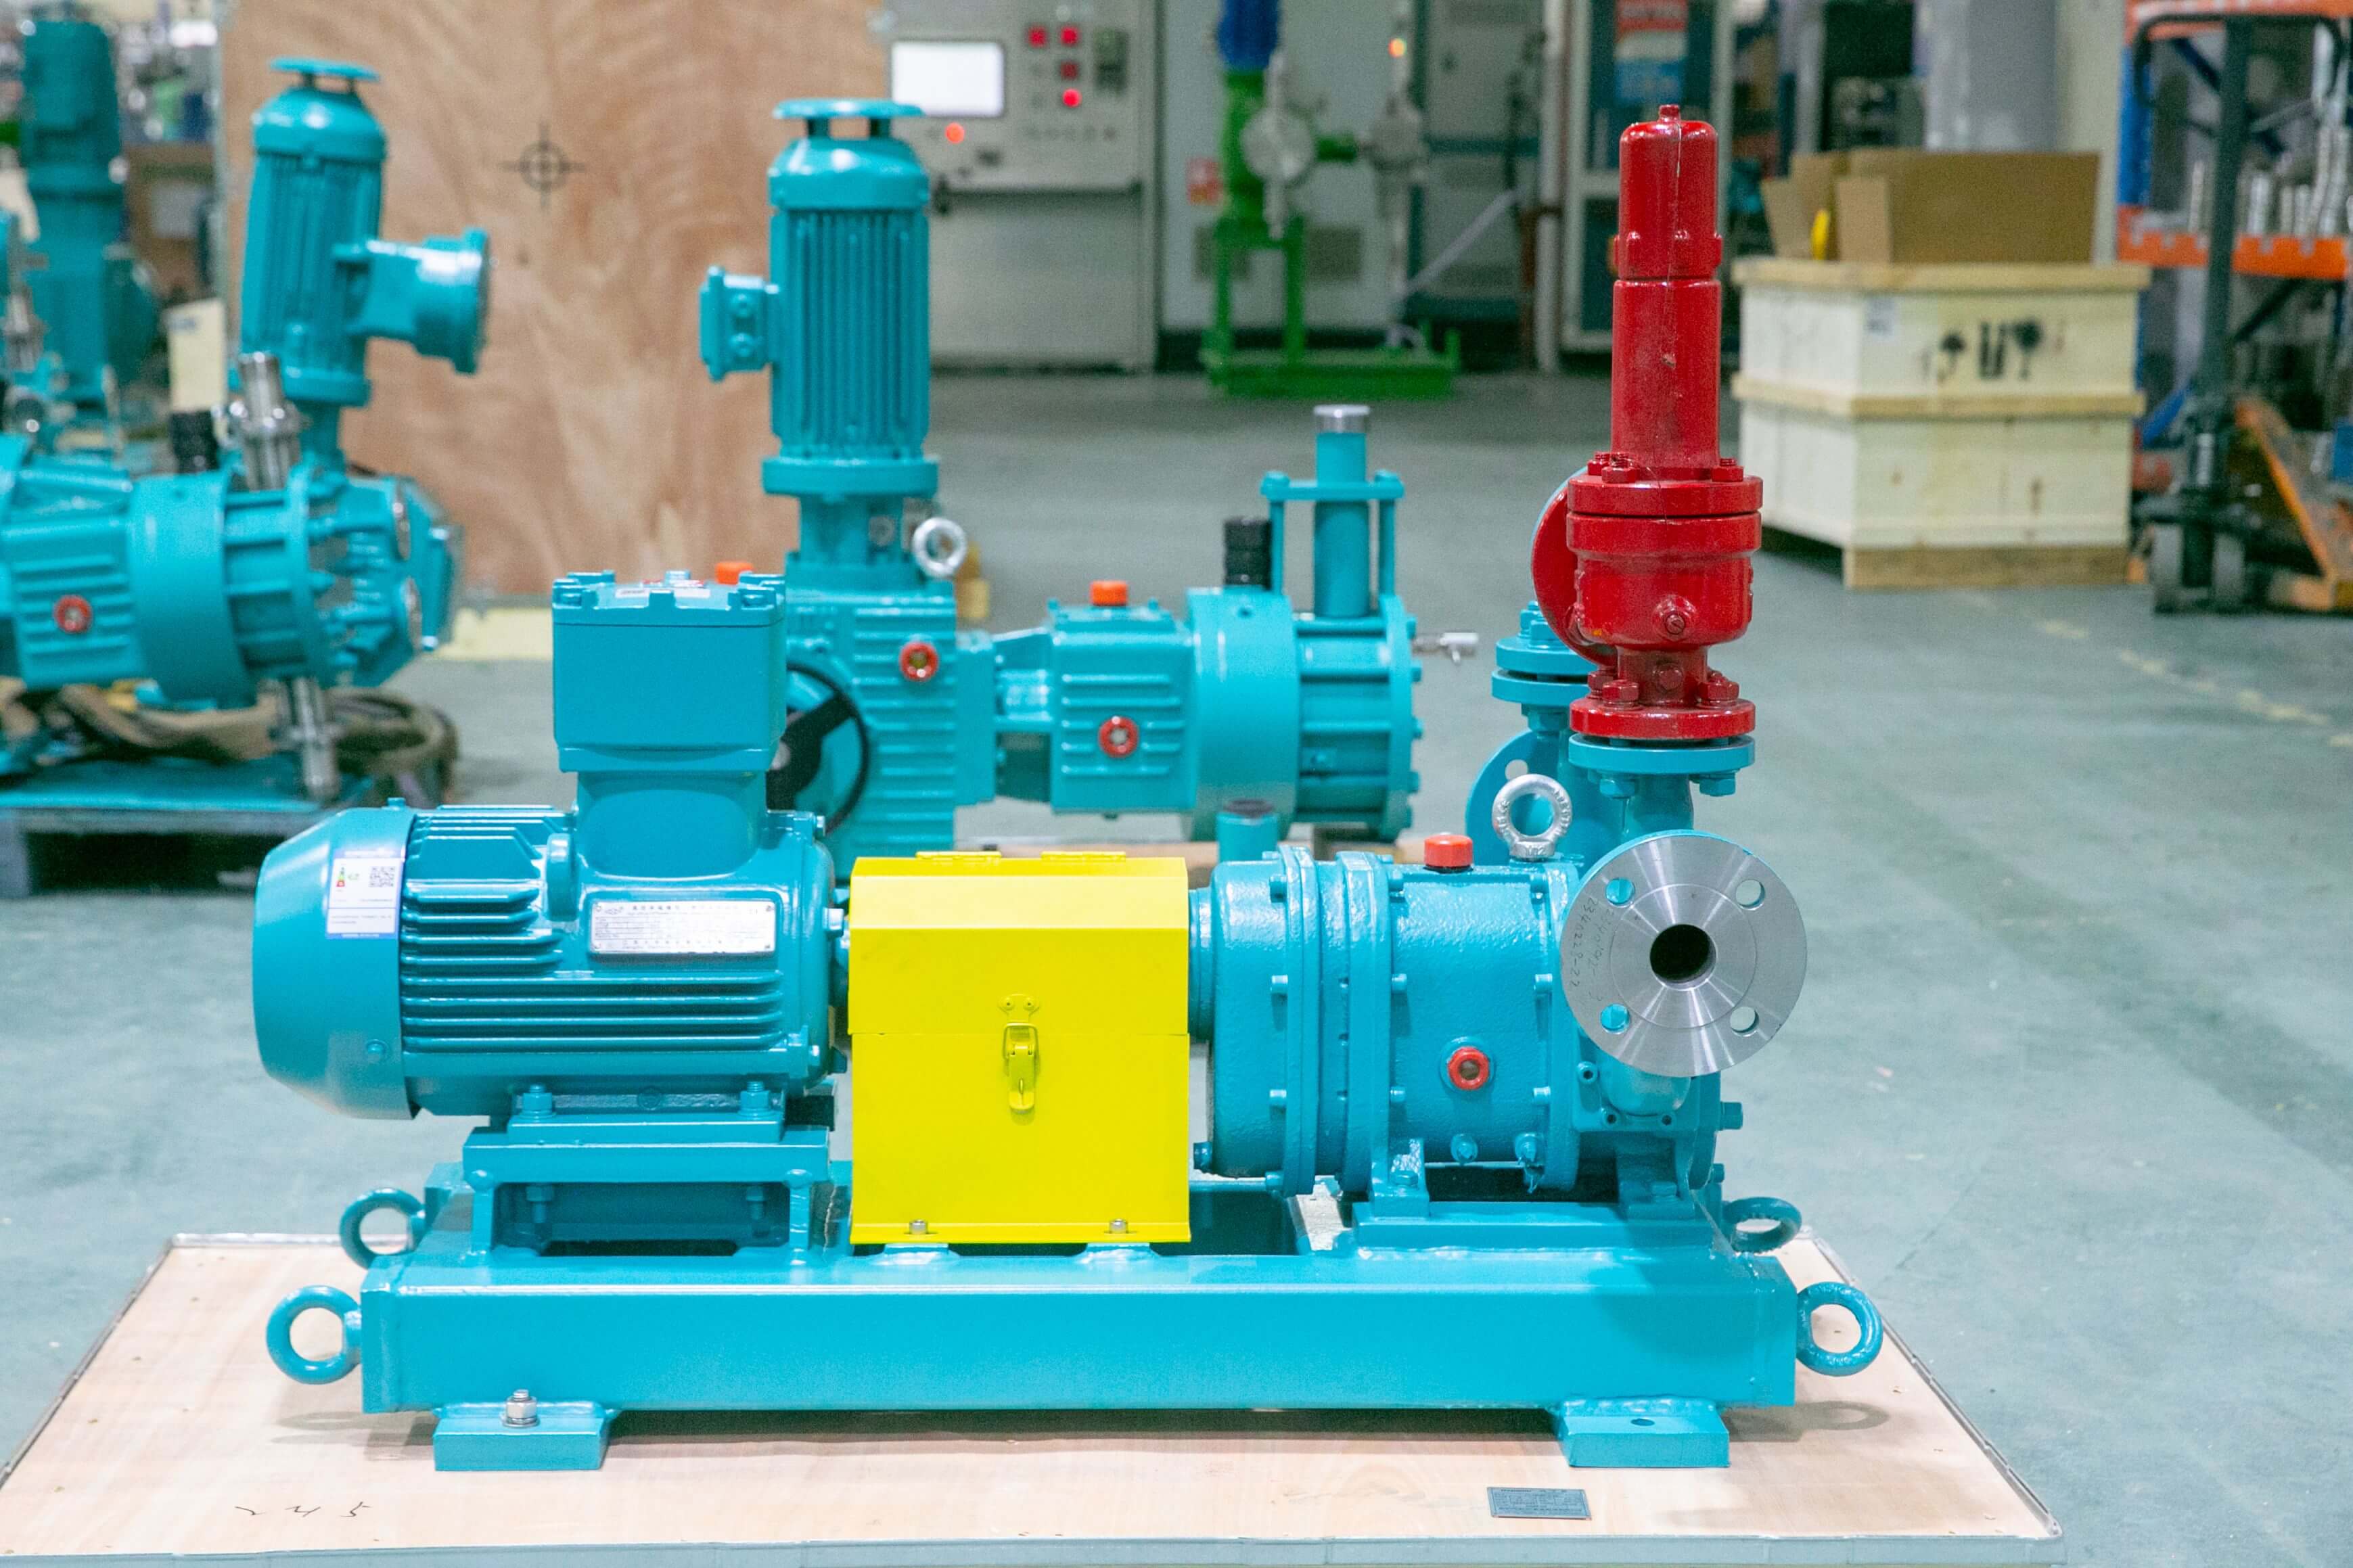
Understanding Rotary Lobe Pump Technology
Rotary lobe pumps belong to the positive displacement pump family, operating through the synchronized rotation of two or more lobed rotors within a pump casing. As the rotors turn, they create expanding chambers on the suction side that draw in fluid, then transport it to the discharge side where the chambers collapse, forcing the fluid out. This design enables several key advantages:
First, the non-contacting operation between rotors and between rotors and casing means minimal wear and tear, resulting in extended service life even with abrasive media. Second, the gentle pumping action makes them ideal for shear-sensitive fluids like food products, cosmetics, and pharmaceuticals. Third, their ability to handle viscous fluids up to several million centipoois (cP) sets them apart from many other pump types.
At Depamump, we’ve enhanced this basic design through continuous innovation. Our rotary lobe pumps feature precision-engineered lobes with optimized profiles to maximize volumetric efficiency while minimizing pulsation. The robust casing design withstands high pressures, and our selection of materials – from stainless steel to specialized alloys and elastomers – ensures compatibility with virtually any industrial fluid.
Key Applications of Rotary Lobe Pumps
The versatility of rotary lobe pumps makes them indispensable across numerous industries. In the chemical processing sector, they excel at transferring aggressive chemicals, solvents, and polymers with consistent flow rates. The food and beverage industry relies on them for pumping everything from yogurt and peanut butter to chocolate and tomato paste, where product integrity is paramount.
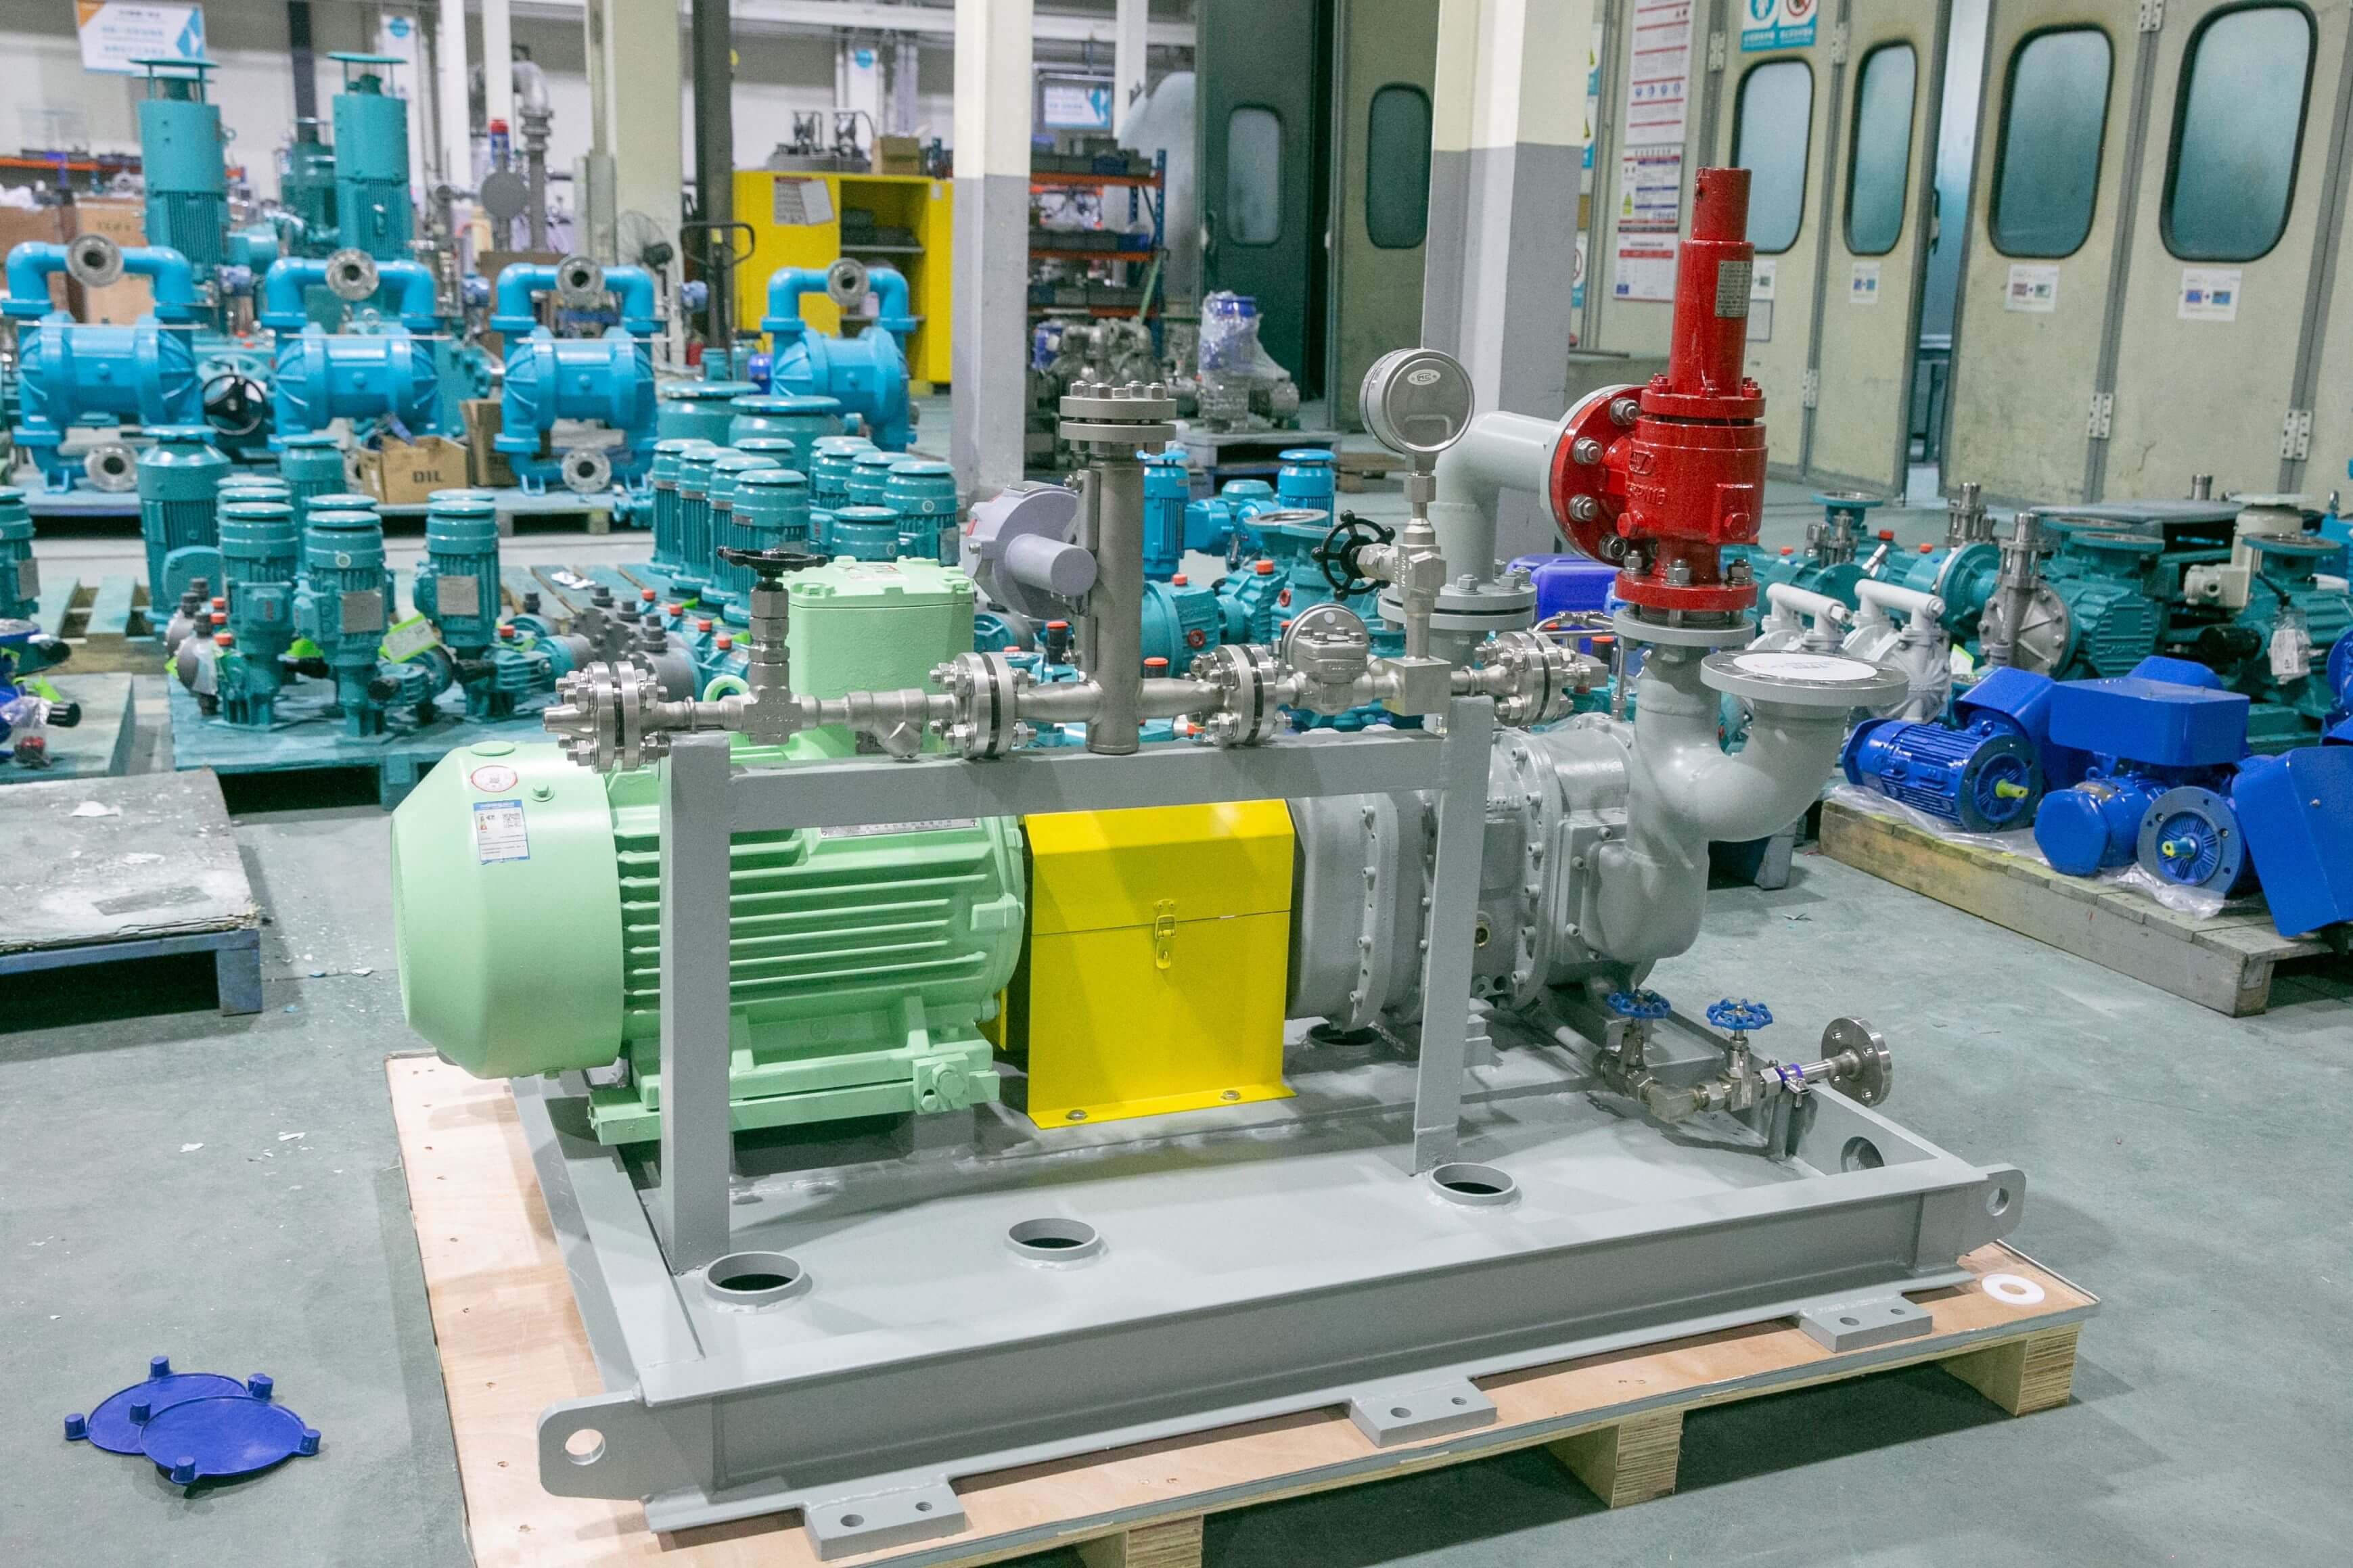
In the oil and gas sector, our rotary lobe pumps demonstrate their strength in crude oil transfer, sludge pumping, and wastewater treatment. The wastewater treatment industry benefits from their ability to handle slurries, activated sludge, and chemicals with suspended solids. Even in pharmaceutical manufacturing, where hygiene standards are stringent, our sanitary-grade rotary lobe pumps meet all regulatory requirements while maintaining precise dosing capabilities.
One notable application is in the pulp and paper industry, where our pumps transfer thick stock, black liquor, and other viscous materials with ease. The mining sector utilizes them for pumping tailings and other abrasive slurries, thanks to our wear-resistant materials and robust construction. In the dairy industry, our pumps gently handle milk, cream, and whey without causing product degradation.
Comparative Advantages Over Other Pump Types
When compared to gear pumps, rotary lobe pumps offer several distinct benefits. While both handle viscous fluids well, rotary lobe pumps generate less shear, making them preferable for shear-sensitive products. They also typically produce lower pulsation levels, resulting in smoother flow and reduced stress on piping systems.
Against centrifugal pumps, rotary lobe pumps maintain consistent flow rates regardless of pressure variations, making them ideal for dosing applications. Their ability to handle fluids with high solid content or gas entrainment gives them an edge in many industrial processes where centrifugal pumps would struggle.
Compared to peristaltic pumps, rotary lobe pumps offer higher flow rates and better energy efficiency for comparable applications. They also require less frequent maintenance as the pumping elements don’t need replacement as often as peristaltic tubing.
- Consistent flow rates independent of pressure
- Ability to handle viscous fluids up to 1,000,000 cP
- Gentle pumping action preserves product integrity
- Non-clogging design handles solids and slurries
- Reversible flow direction for operational flexibility
- Dry running capability for short periods
Selecting the Right Rotary Lobe Pump Manufacturer
Choosing a reliable rotary lobe pump supplier requires careful consideration of several factors. First, evaluate the manufacturer’s experience in your specific industry. Depamump, with over two decades of expertise in fluid handling solutions, has developed specialized knowledge across multiple sectors, enabling us to anticipate and address industry-specific challenges.
Material selection capabilities are crucial, as different applications demand different construction materials. Our comprehensive material portfolio includes stainless steel for corrosive environments, duplex stainless steel for enhanced strength, and various elastomers for seal compatibility. For food applications, we offer FDA-compliant materials and sanitary finishes.
Customization options separate premium manufacturers from standard suppliers. At Depamump, we understand that no two applications are identical. Our engineering team works closely with clients to design pumps that meet exact specifications for flow rate, pressure, temperature, and media characteristics. This includes custom port configurations, heating/cooling jackets, and specialized sealing arrangements.
After-sales support is another critical consideration. Our global service network ensures prompt assistance wherever your operations are located. We stock a comprehensive range of spare parts and offer preventive maintenance programs to maximize pump uptime and extend service life.
Quality Assurance and Certifications
When evaluating potential suppliers, certifications provide important validation of quality standards. Depamump holds ISO 9001 certification for our quality management system, ensuring consistent product quality and reliable performance. For applications in hazardous environments, our pumps comply with ATEX and IECEx standards for explosion-proof equipment.
In food and pharmaceutical applications, our sanitary pumps meet 3-A Sanitary Standards and EHEDG guidelines, ensuring they can be easily cleaned and sanitized to prevent contamination. We also provide material certificates and traceability for all critical components, giving you complete confidence in the integrity of our products.
Our commitment to quality extends beyond certification. Every Depamump rotary lobe pump undergoes rigorous testing before shipment, including performance testing, leakage testing, and noise level measurement. This comprehensive testing protocol ensures that your pump arrives ready for immediate installation and operation.
| Feature | Depamump Advantage |
|---|---|
| Material Options | Stainless steel, duplex stainless steel, specialized alloys, FDA-compliant elastomers |
| Customization | Tailored designs for specific flow rates, pressures, and media requirements |
| Certifications | ISO 9001, ATEX, IECEx, 3-A Sanitary Standards, EHEDG |
| Testing Protocol | Comprehensive performance, leakage, and noise testing before shipment |
| Global Support | Worldwide service network with prompt spare parts availability |
FAQ
What makes Depamump rotary lobe pumps suitable for food processing applications?
Our food-grade rotary lobe pumps feature FDA-compliant materials, sanitary finishes, and crevice-free designs that prevent bacterial growth. They’re designed for easy cleaning in place (CIP) and sterilization in place (SIP), meeting all major food safety standards while maintaining gentle product handling.
How do you ensure compatibility with corrosive chemicals in chemical processing applications?
We conduct thorough material compatibility analysis for each application, selecting from our extensive range of corrosion-resistant materials including various stainless steels, Hastelloy, and specialized coatings. Our engineering team also considers factors like temperature and concentration when specifying materials.
What maintenance is required for optimal performance of rotary lobe pumps?
Regular maintenance includes checking and replacing wear parts like rotors, seals, and bushings according to your operating conditions. We recommend establishing a preventive maintenance schedule based on our guidelines, which typically includes lubrication checks, vibration analysis, and performance monitoring.
Can Depamump provide customized rotary lobe pump solutions for unique applications?
Absolutely. Customization is one of our core strengths. Our engineering team works closely with clients to design pumps that meet exact specifications for flow rate, pressure, temperature, and media characteristics, including special port configurations, heating/cooling jackets, and unique sealing arrangements.
Summary
Rotary lobe pumps represent a versatile solution for industrial fluid handling challenges, offering consistent performance across a wide range of applications. When selecting a supplier, it’s essential to consider not just the pump itself but the manufacturer’s ability to provide customized solutions, comprehensive support, and proven reliability in your specific industry.
Depamump stands out as a premier rotary lobe pump manufacturer with over two decades of experience in developing innovative fluid handling solutions. Our commitment to quality, extensive material options, and customization capabilities ensure we can meet even the most demanding application requirements. With global manufacturing facilities and a worldwide service network, we provide reliable support wherever your operations are located.
Whether you need a standard rotary lobe pump for general industrial use or a customized solution for a specialized application, Depamump has the expertise and resources to deliver. Contact us today to discuss your specific requirements and discover how our rotary lobe pumps can enhance your fluid handling operations.