
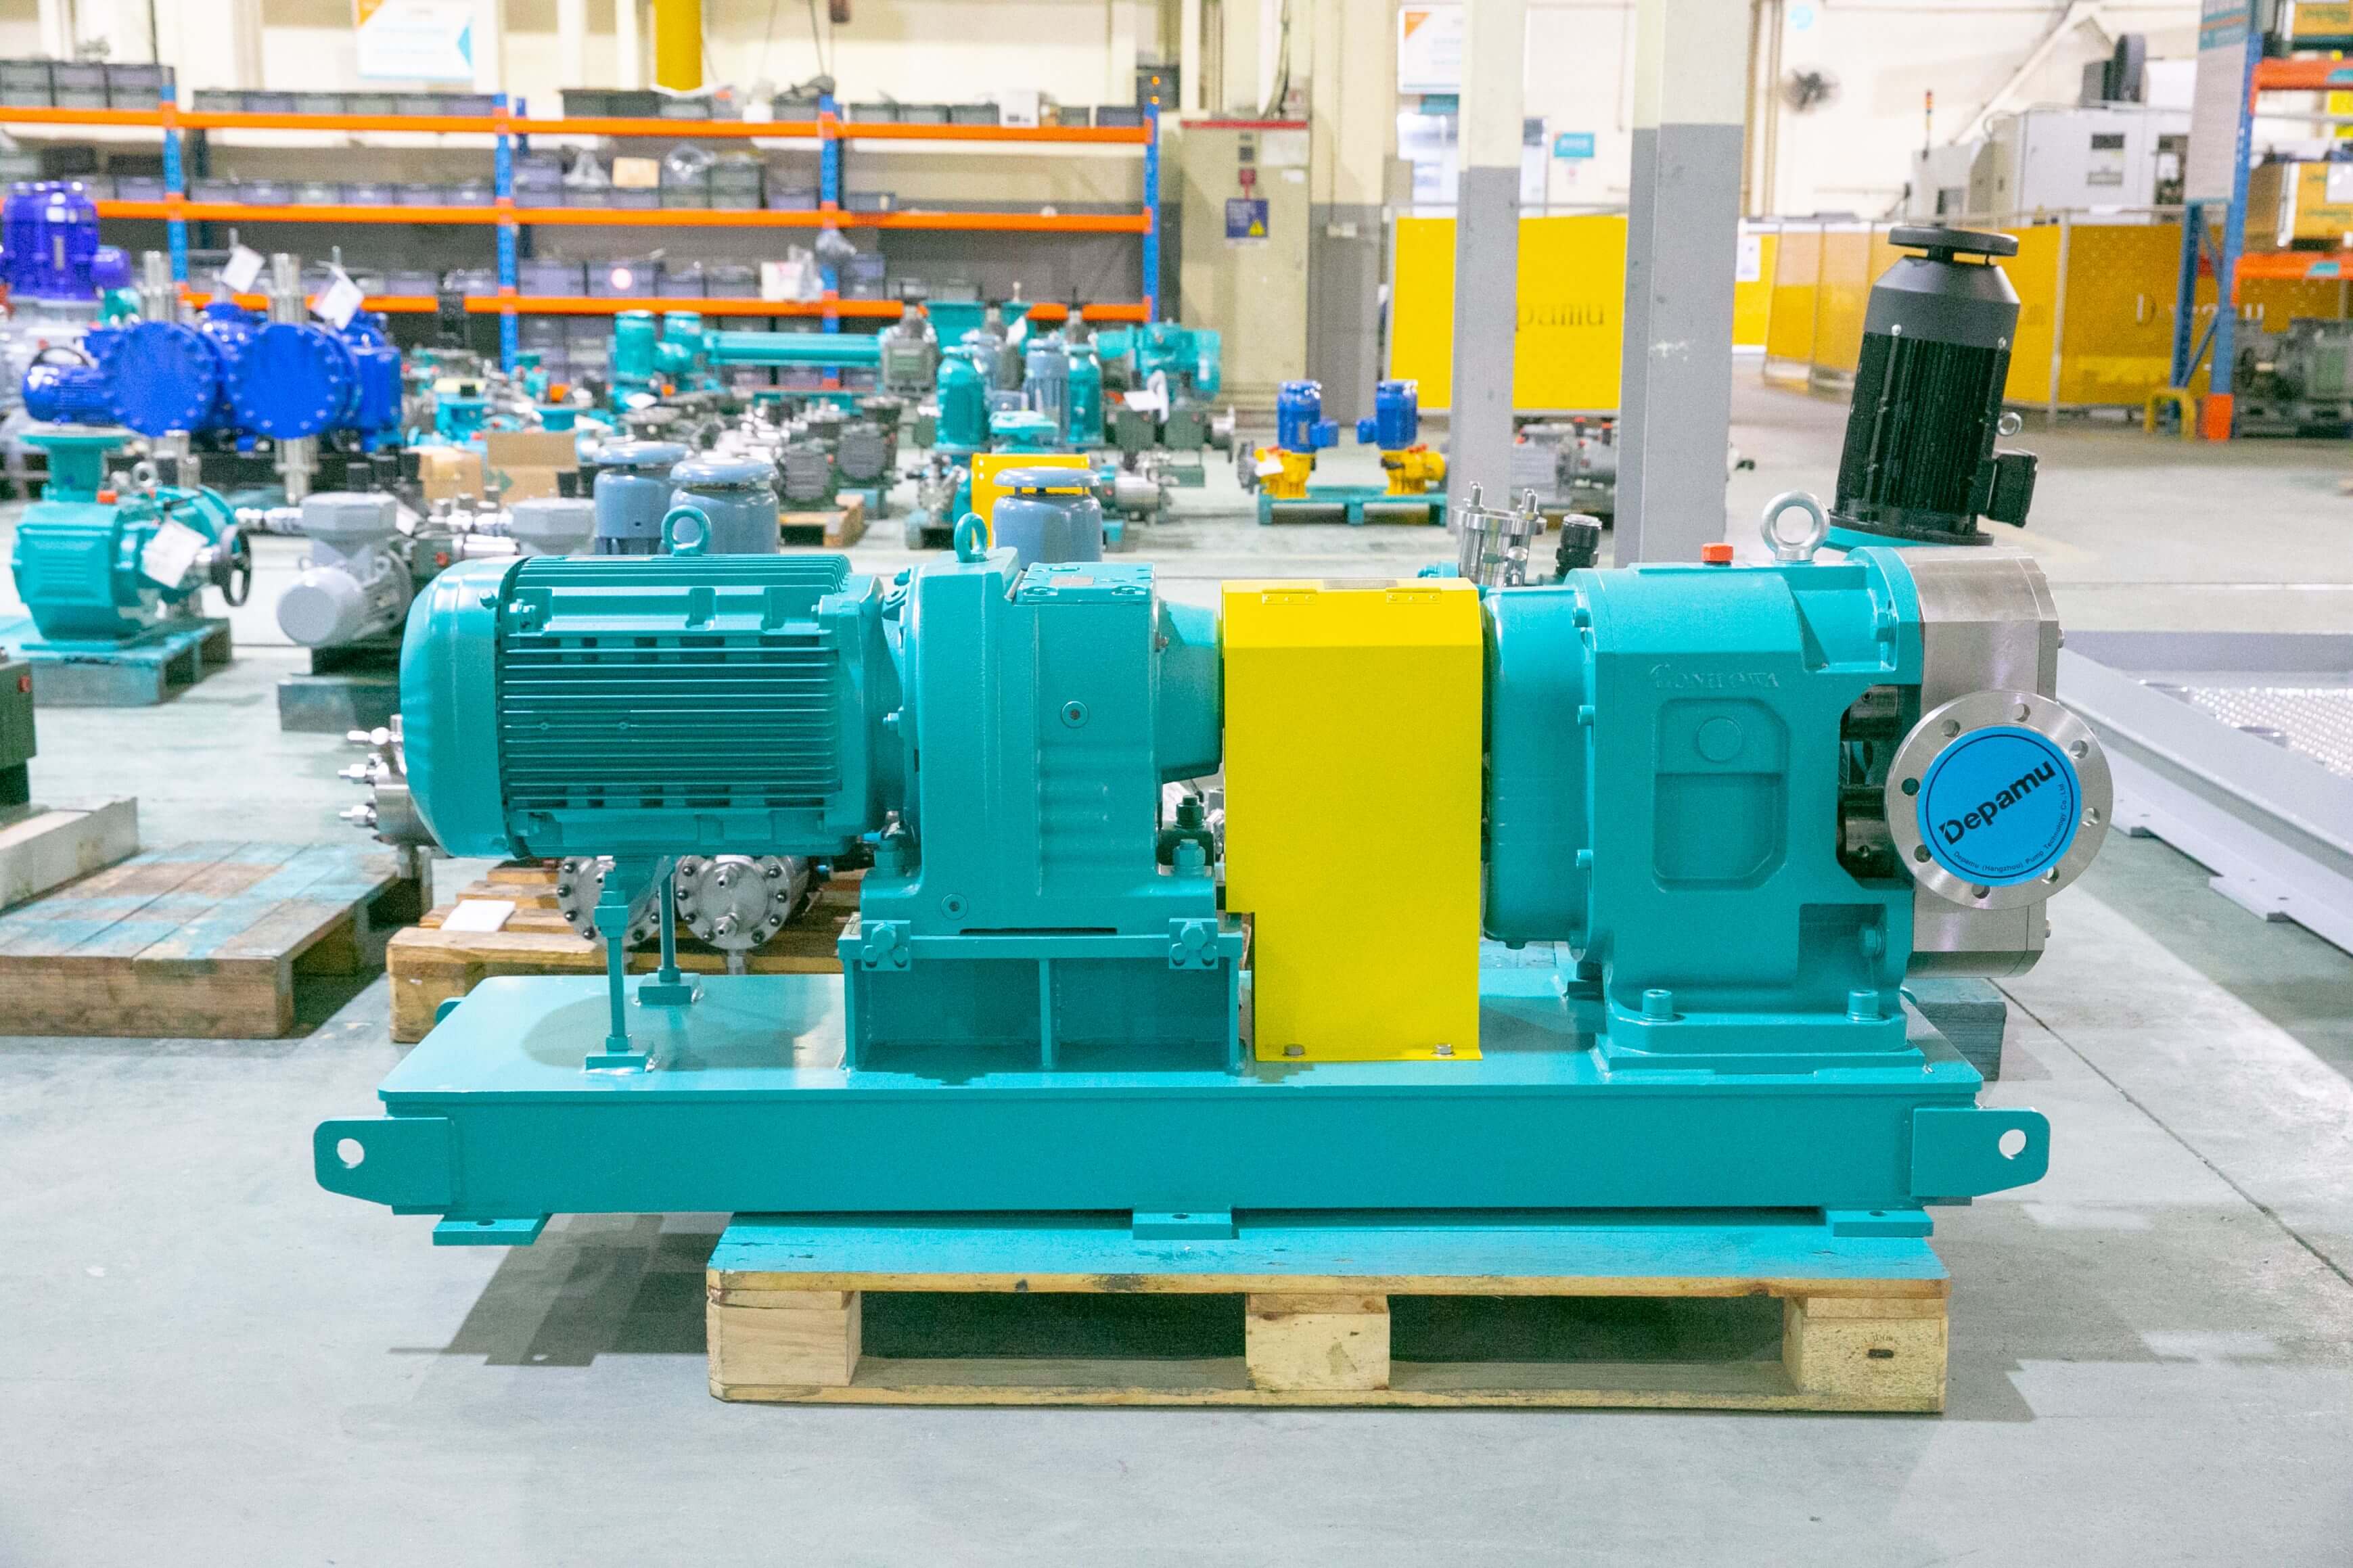
When it comes to industrial fluid handling, cam pumps (also known as rotary lobe pumps) play a crucial role in various applications requiring gentle product handling, high viscosity capabilities, and reliable performance. As a global leader in premium volumetric pumps and fluid equipment since 2003, Depamp (Hangzhou) Pump Technology Co., Ltd. has established itself as a trusted manufacturer and supplier of high-quality cam pumps and customized fluid solutions. This comprehensive guide explores everything industrial buyers need to know about cam pumps, from their working principles to selection criteria and application-specific solutions.
Understanding Cam Pump Technology and Applications
Cam pumps belong to the positive displacement pump family, featuring two or more rotating lobes (typically three) that create expanding chambers to move fluids through the pump. This design provides several key advantages for industrial applications:
First, the gentle pumping action makes cam pumps ideal for shear-sensitive products like food emulsions, pharmaceuticals, and personal care products. The non-contacting lobes prevent product degradation while maintaining consistent flow rates regardless of viscosity changes.
Second, cam pumps excel at handling high-viscosity fluids (up to 1,000,000 cP) that would challenge centrifugal pumps. This capability makes them indispensable in industries like petrochemicals, adhesives, and waste treatment where thick, abrasive slurries are common.
Third, the simple design with few moving parts ensures reliable operation with minimal maintenance requirements. When properly specified, cam pumps can run continuously for years with only periodic seal replacement.
At Depamp Pump Technology, we’ve engineered our cam pumps to meet the most demanding industrial requirements. Our product range includes standard models with flow rates from 0.5 to 500 m³/h and pressures up to 16 bar, along with custom-engineered solutions for specialized applications.
Key Selection Criteria for Industrial Cam Pumps
Choosing the right cam pump requires careful consideration of several critical factors that impact performance and longevity:
1. Material Compatibility
The pump construction materials must withstand your process fluids’ chemical properties. Depamp offers cam pumps in various materials including stainless steel (304/316), duplex steel, and special alloys for corrosive applications. For food-grade applications, we provide pumps compliant with FDA, 3A, and EHEDG standards.
2. Viscosity Handling
While all cam pumps handle viscous fluids better than centrifugal pumps, different models have varying viscosity limits. Our technical team helps customers select pumps with appropriate lobe geometry and speed ranges to ensure optimal performance with their specific fluid viscosities.
3. Temperature and Pressure Ratings
Process conditions dictate the required temperature and pressure capabilities. Depamp’s cam pumps operate reliably at temperatures from -40°C to +200°C and pressures up to 16 bar, with custom designs available for more extreme conditions.
4. Sealing Options
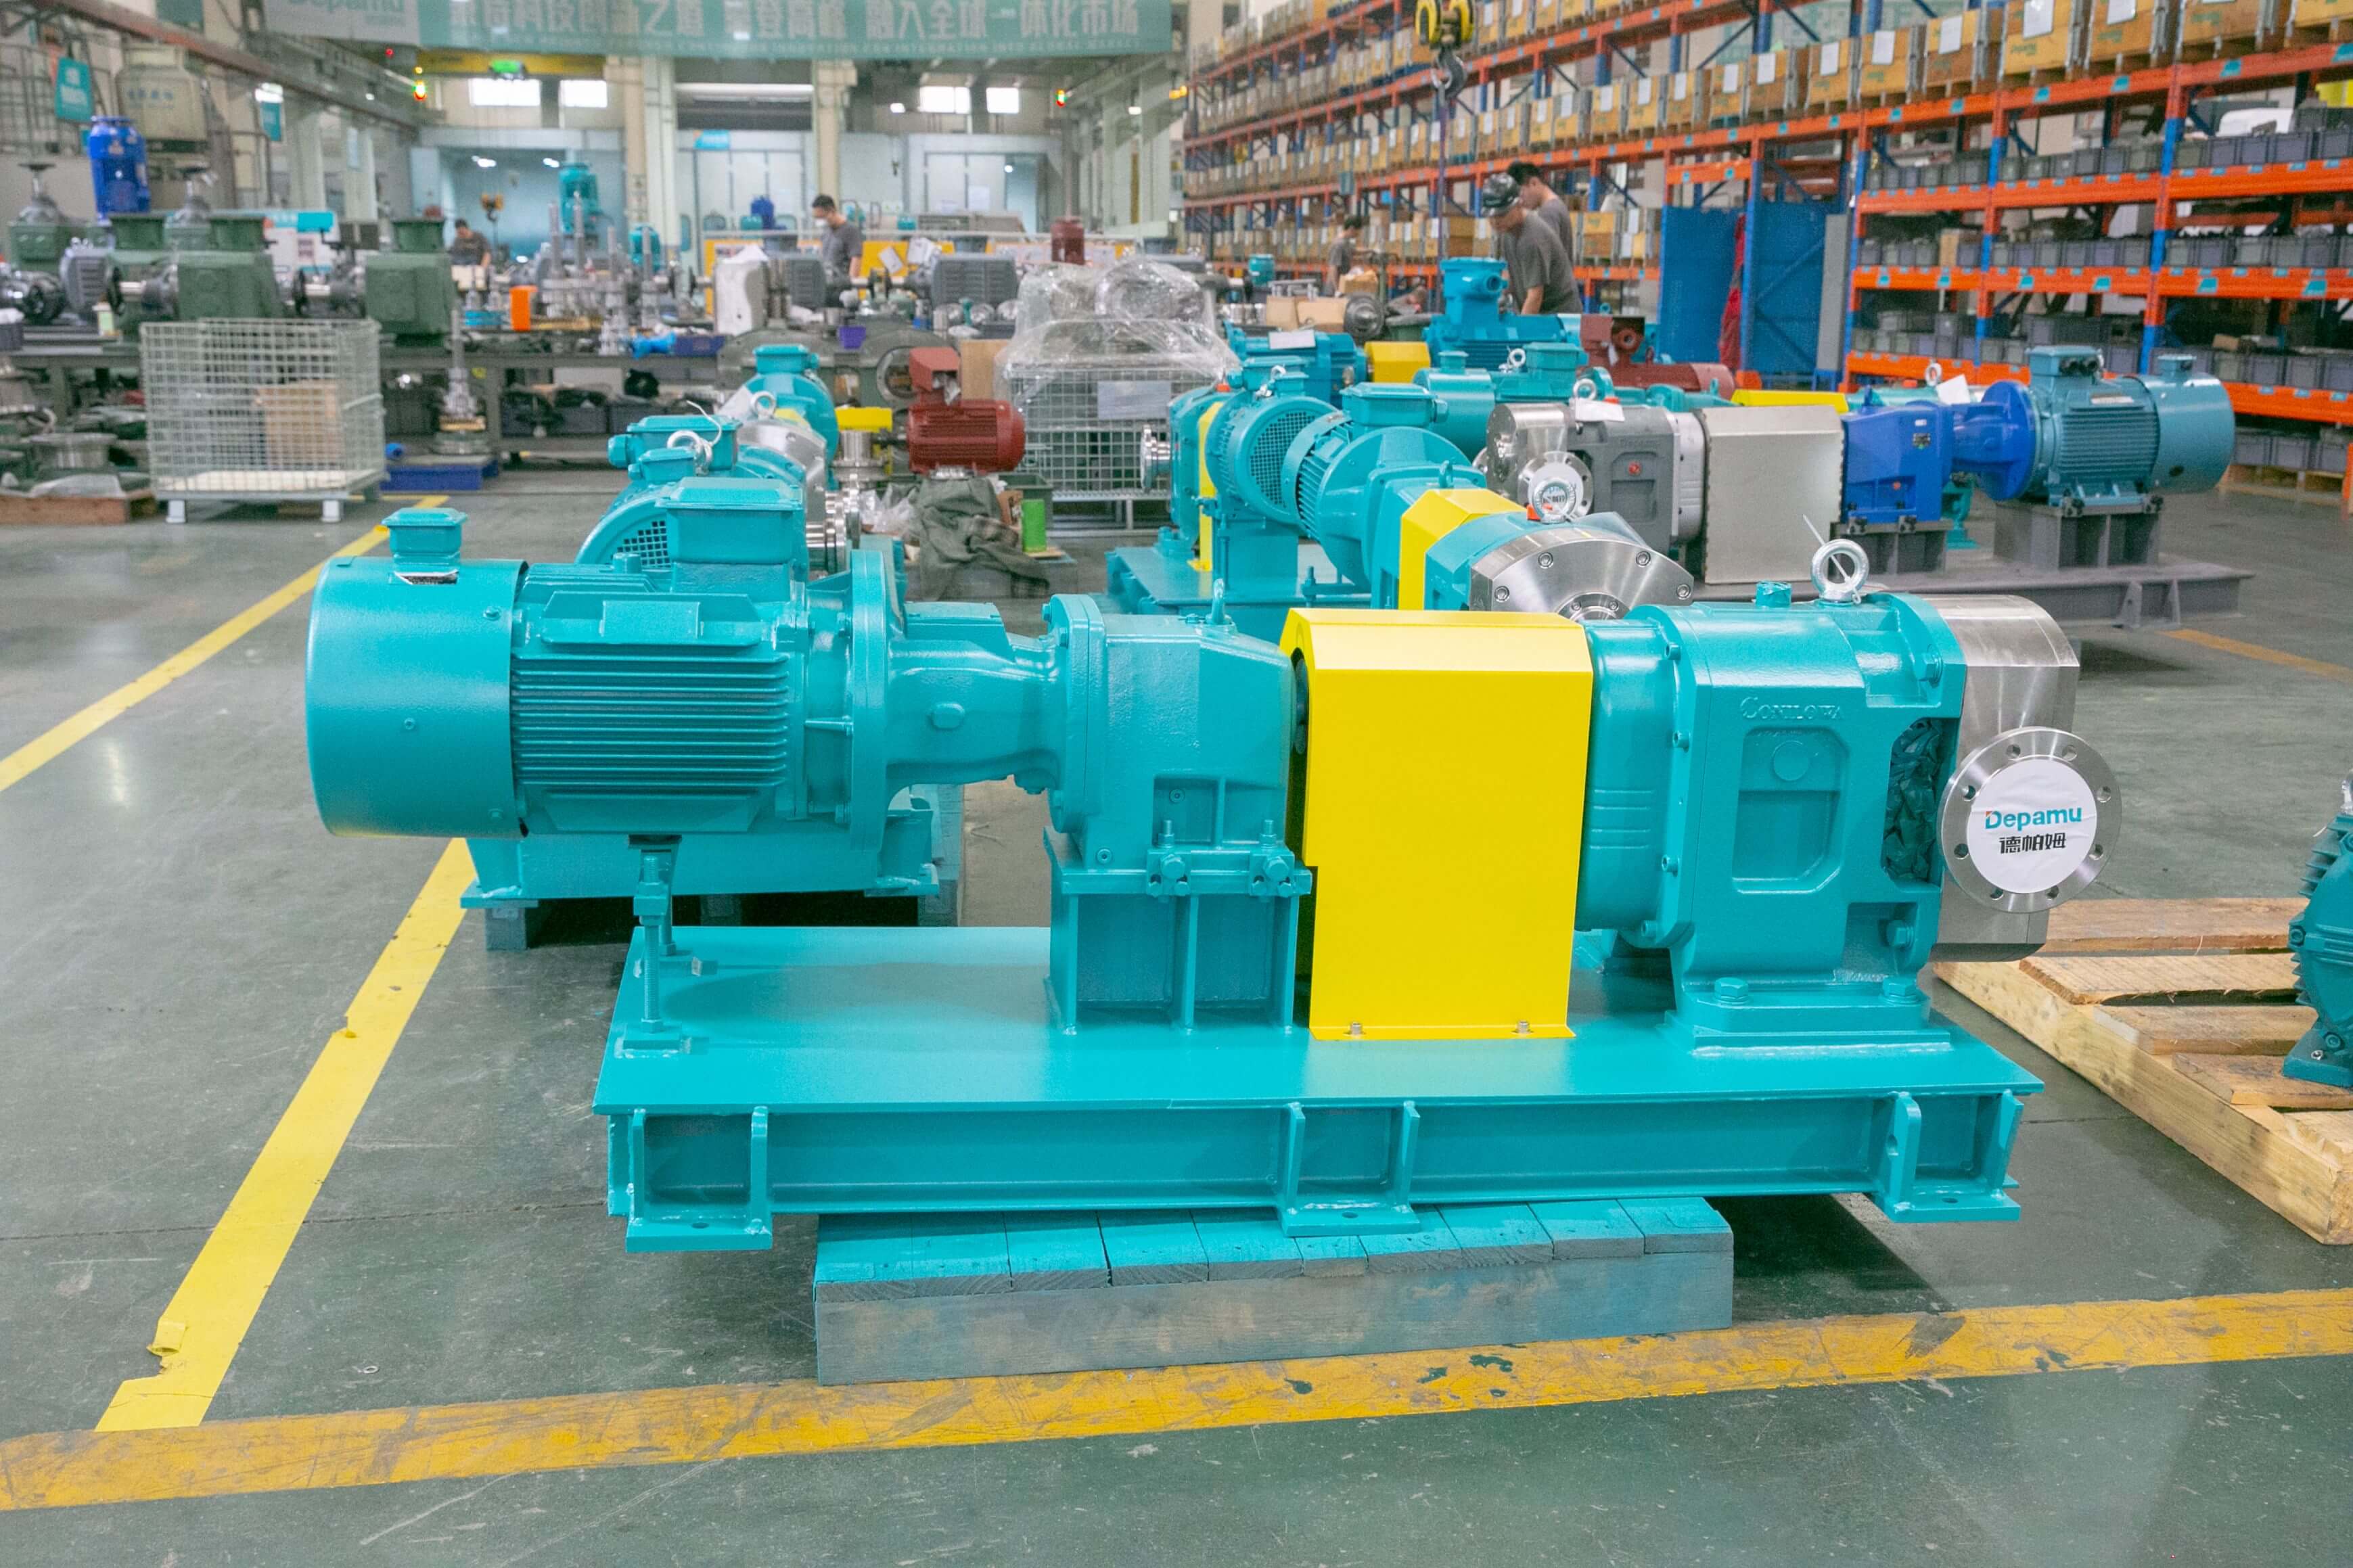
Proper sealing prevents leaks and protects pump components. Depamp provides multiple sealing solutions including mechanical seals, lip seals, and magnetic couplings, with materials selected based on your application’s requirements.
5. Drive Configuration
We offer both direct-driven and gear-reduced cam pumps to match your speed and torque requirements. Variable frequency drives (VFDs) are available for precise flow control and energy savings.
Application-Specific Cam Pump Solutions
Depamp’s cam pumps serve diverse industries with tailored solutions for each application’s unique challenges:
- Chemical Processing: Our corrosion-resistant cam pumps handle aggressive chemicals with precision dosing capabilities for reactor feeding and blend formulation.
- Oil & Gas: Heavy-duty cam pumps transfer drilling mud, cement slurries, and produced water with abrasion-resistant materials and high-pressure ratings.
- Food & Beverage: Sanitary cam pumps with CIP/SIP capabilities gently pump yogurt, mayonnaise, and other viscous food products without product degradation.
- Wastewater Treatment: Our sludge pumps efficiently transfer activated sludge, scum, and primary sludge with self-priming capabilities and resistance to clogging.
- Pharmaceutical: Cleanroom-compatible cam pumps with sterile design features handle active pharmaceutical ingredients (APIs) and biotech products.
One notable application is in the polymer industry, where our cam pumps transfer melted polymers at high temperatures without altering their molecular structure. The pumps’ gentle action maintains product quality while their robust construction withstands abrasive polymer additives.
| Application | Key Requirements | Depamp Solution |
|---|---|---|
| Chemical Dosing | Precise flow control, corrosion resistance | Stainless steel cam pumps with micro-metering adjustments |
| Viscous Product Transfer | High torque, gentle handling | Gear-reduced cam pumps with large clearance lobes |
| Slurry Handling | Abrasion resistance, solids handling | Hardened alloy cam pumps with replaceable liners |
Depamp’s Advantages as Your Cam Pump Supplier
Choosing Depamp as your cam pump supplier brings several competitive advantages:
Comprehensive Manufacturing Capabilities: With our 35,000 m² factory and 400+ skilled employees, we control every aspect of production from R&D to final assembly. This vertical integration ensures consistent quality and shorter lead times compared to traders or assemblers.
Customization Expertise: Our engineering team has developed hundreds of custom cam pump solutions for unique applications. Whether you need special materials, modified port configurations, or integration with existing systems, we have the capabilities to deliver.
Global Certifications: All our cam pumps comply with international standards including CE, ATEX, and API 676. For export markets, we provide documentation packages tailored to your region’s requirements.
After-Sales Support: Our global service network provides prompt technical support, spare parts delivery, and on-site maintenance services. We stock critical components at regional warehouses to minimize downtime.
Cost-Effective Solutions: By optimizing our manufacturing processes and maintaining high production volumes, we offer competitive pricing without compromising quality. Our pumps’ long service life and low maintenance requirements further reduce total cost of ownership.
FAQ
What makes cam pumps better than centrifugal pumps for viscous fluids?
Cam pumps generate consistent flow rates regardless of viscosity changes because they displace a fixed volume of fluid with each rotation. Centrifugal pumps rely on velocity to move fluids, making their performance drop significantly as viscosity increases. Additionally, cam pumps’ gentle pumping action prevents product degradation in shear-sensitive applications.
How do I select the right lobe material for my application?
The lobe material selection depends on your fluid’s chemical properties and operating temperature. For corrosive chemicals, we recommend stainless steel or special alloys. For abrasive slurries, hardened alloys with wear-resistant coatings work best. Our application engineers can analyze your process fluids and recommend the most cost-effective material that meets your performance requirements.
Can cam pumps handle fluids with solids content?
Yes, cam pumps excel at handling fluids containing solids up to 30% by volume, depending on the particle size and shape. The clearances between lobes and pump casing can be adjusted to accommodate specific solids sizes. For highly abrasive applications, we offer pumps with replaceable liners and hardened components to extend service life.
What maintenance is required for industrial cam pumps?
Regular maintenance includes checking and replacing mechanical seals or lip seals as needed, inspecting lobes for wear, and verifying proper alignment. With proper maintenance, our cam pumps typically operate for 5-10 years between major overhauls. We provide detailed maintenance manuals with each pump and offer training programs for your maintenance personnel.
Summary
Selecting the right cam pump supplier requires evaluating not just the pump specifications but also the manufacturer’s capabilities to support your application over its entire lifecycle. Depamp (Hangzhou) Pump Technology Co., Ltd. stands out as a global leader with over two decades of experience in premium volumetric pump manufacturing. Our comprehensive product range, customization expertise, and commitment to quality make us the preferred choice for industrial buyers seeking reliable cam pump solutions.
Whether you need standard cam pumps for general industrial use or customized solutions for challenging applications, our technical team is ready to collaborate with you. Contact us today to discuss your specific requirements and discover how Depamp can help optimize your fluid handling processes with our advanced cam pump technology.