
In the complex landscape of industrial fluid handling, selecting the right pump manufacturer is crucial for ensuring operational efficiency, product quality, and system reliability. Depamump (Hangzhou) Pump Technology Co., Ltd., established in 2003, has emerged as a global leader in high-end positive displacement pumps and fluid equipment solutions. With over 400 employees, a 35,000m² production facility, and annual output exceeding 500 million RMB, the company specializes in developing customized pumping systems that meet the most demanding industrial requirements across petrochemical, nuclear power, oil and gas, and environmental protection sectors.
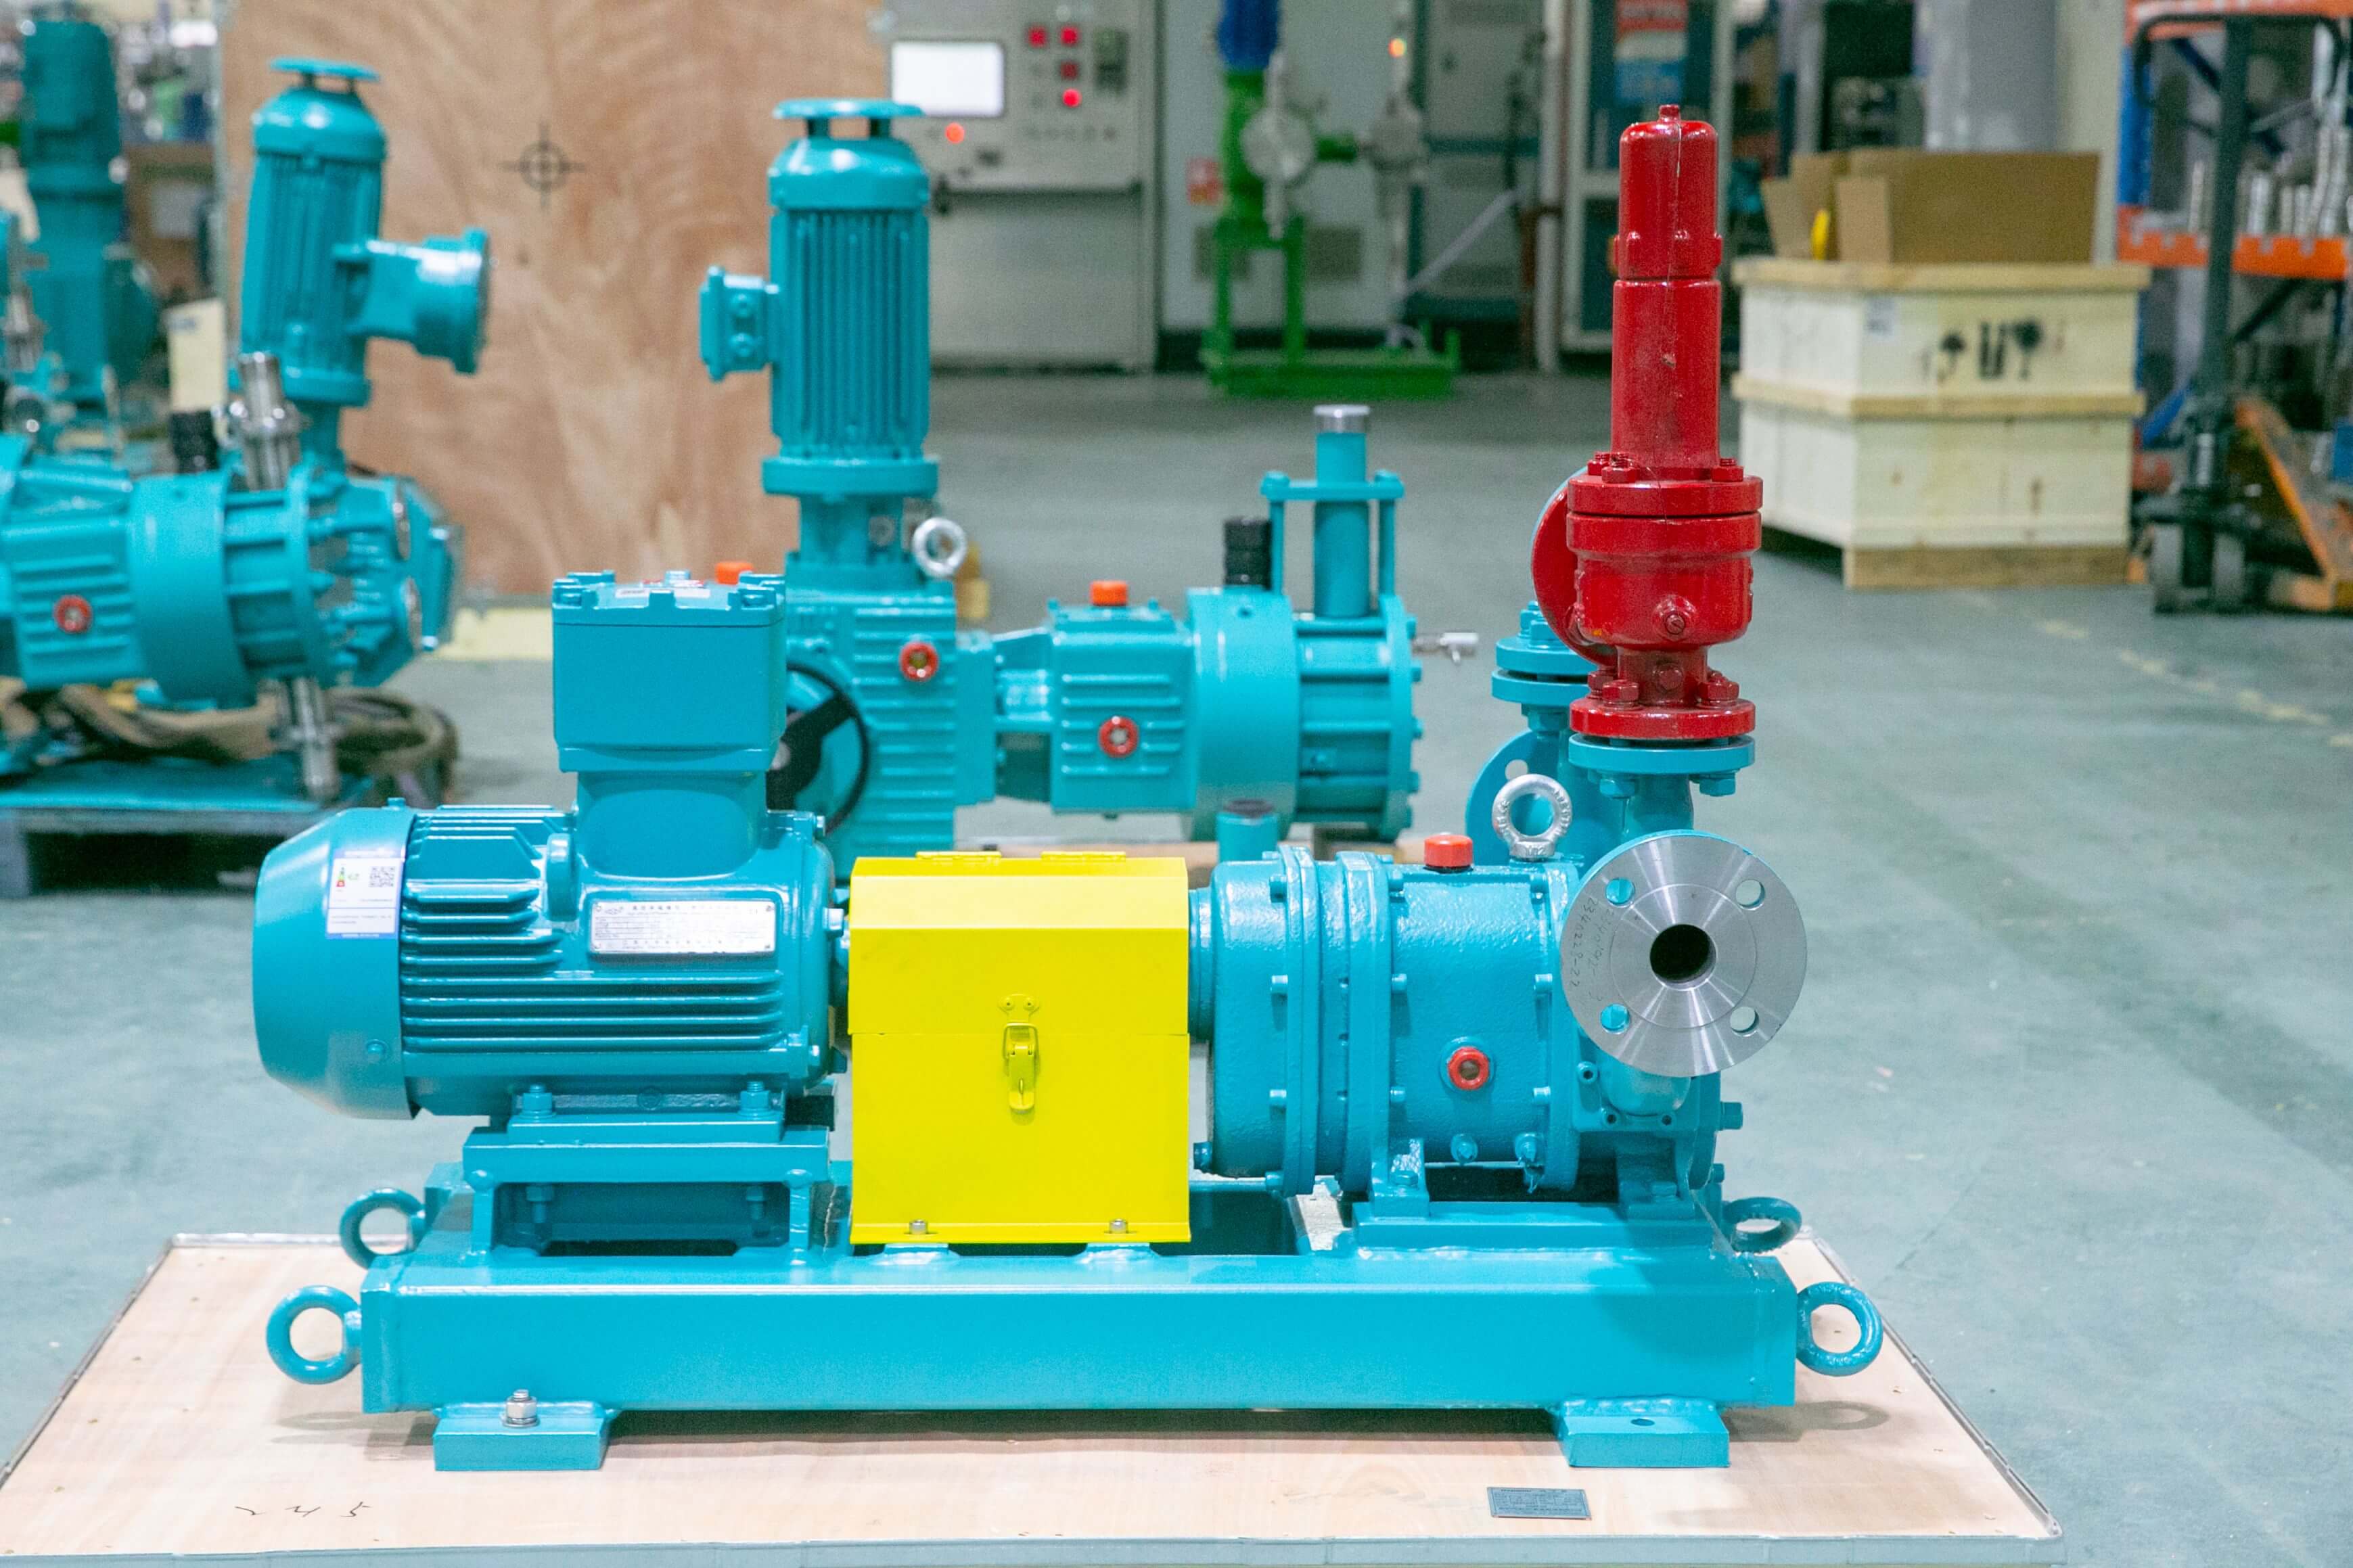
Core Product Expertise: Elastic Rotor Lobe Pumps
As a specialized elastic rotor lobe pump manufacturer, Depamump has developed proprietary technology that combines German engineering precision with continuous innovation. The company’s elastic rotor lobe pumps feature a unique elastomer-lined rotor design that provides exceptional resistance to corrosion, abrasion, and chemical attack while maintaining precise volumetric accuracy. This makes them ideal for handling complex media including:
- Corrosive chemicals in petrochemical processing
- High-temperature fluids in nuclear power plants
- Viscous slurries in wastewater treatment
- Abrasive mixtures in mining operations
- Food-grade liquids in pharmaceutical production
The pumps’ modular design allows for easy maintenance and component replacement, while their hermetic sealing system prevents leakage of hazardous substances. With pressure ratings up to 35MPa and flow capacities from 0.5 to 200m³/h, these pumps can be customized to meet specific process requirements across diverse industrial applications.
Technological Advantages in Pump Manufacturing
Depamump’s competitive edge stems from its vertically integrated manufacturing capabilities and advanced R&D infrastructure. The company operates three specialized production bases equipped with CNC machining centers, dynamic balancing machines, and computerized testing systems that ensure each pump meets stringent quality standards. Key technological advantages include:
1. Precision Metering Pump Technology
The company’s hydraulic diaphragm metering pumps represent the pinnacle of precision dosing technology. By adjusting stroke length and operating frequency, these pumps achieve dosing accuracy within ±1% while handling media with viscosities up to 20,000cP and temperatures ranging from -30°C to +180°C. The hydraulic drive mechanism ensures complete isolation between the process fluid and drive components, eliminating contamination risks and enabling reliable operation with even the most aggressive chemicals.
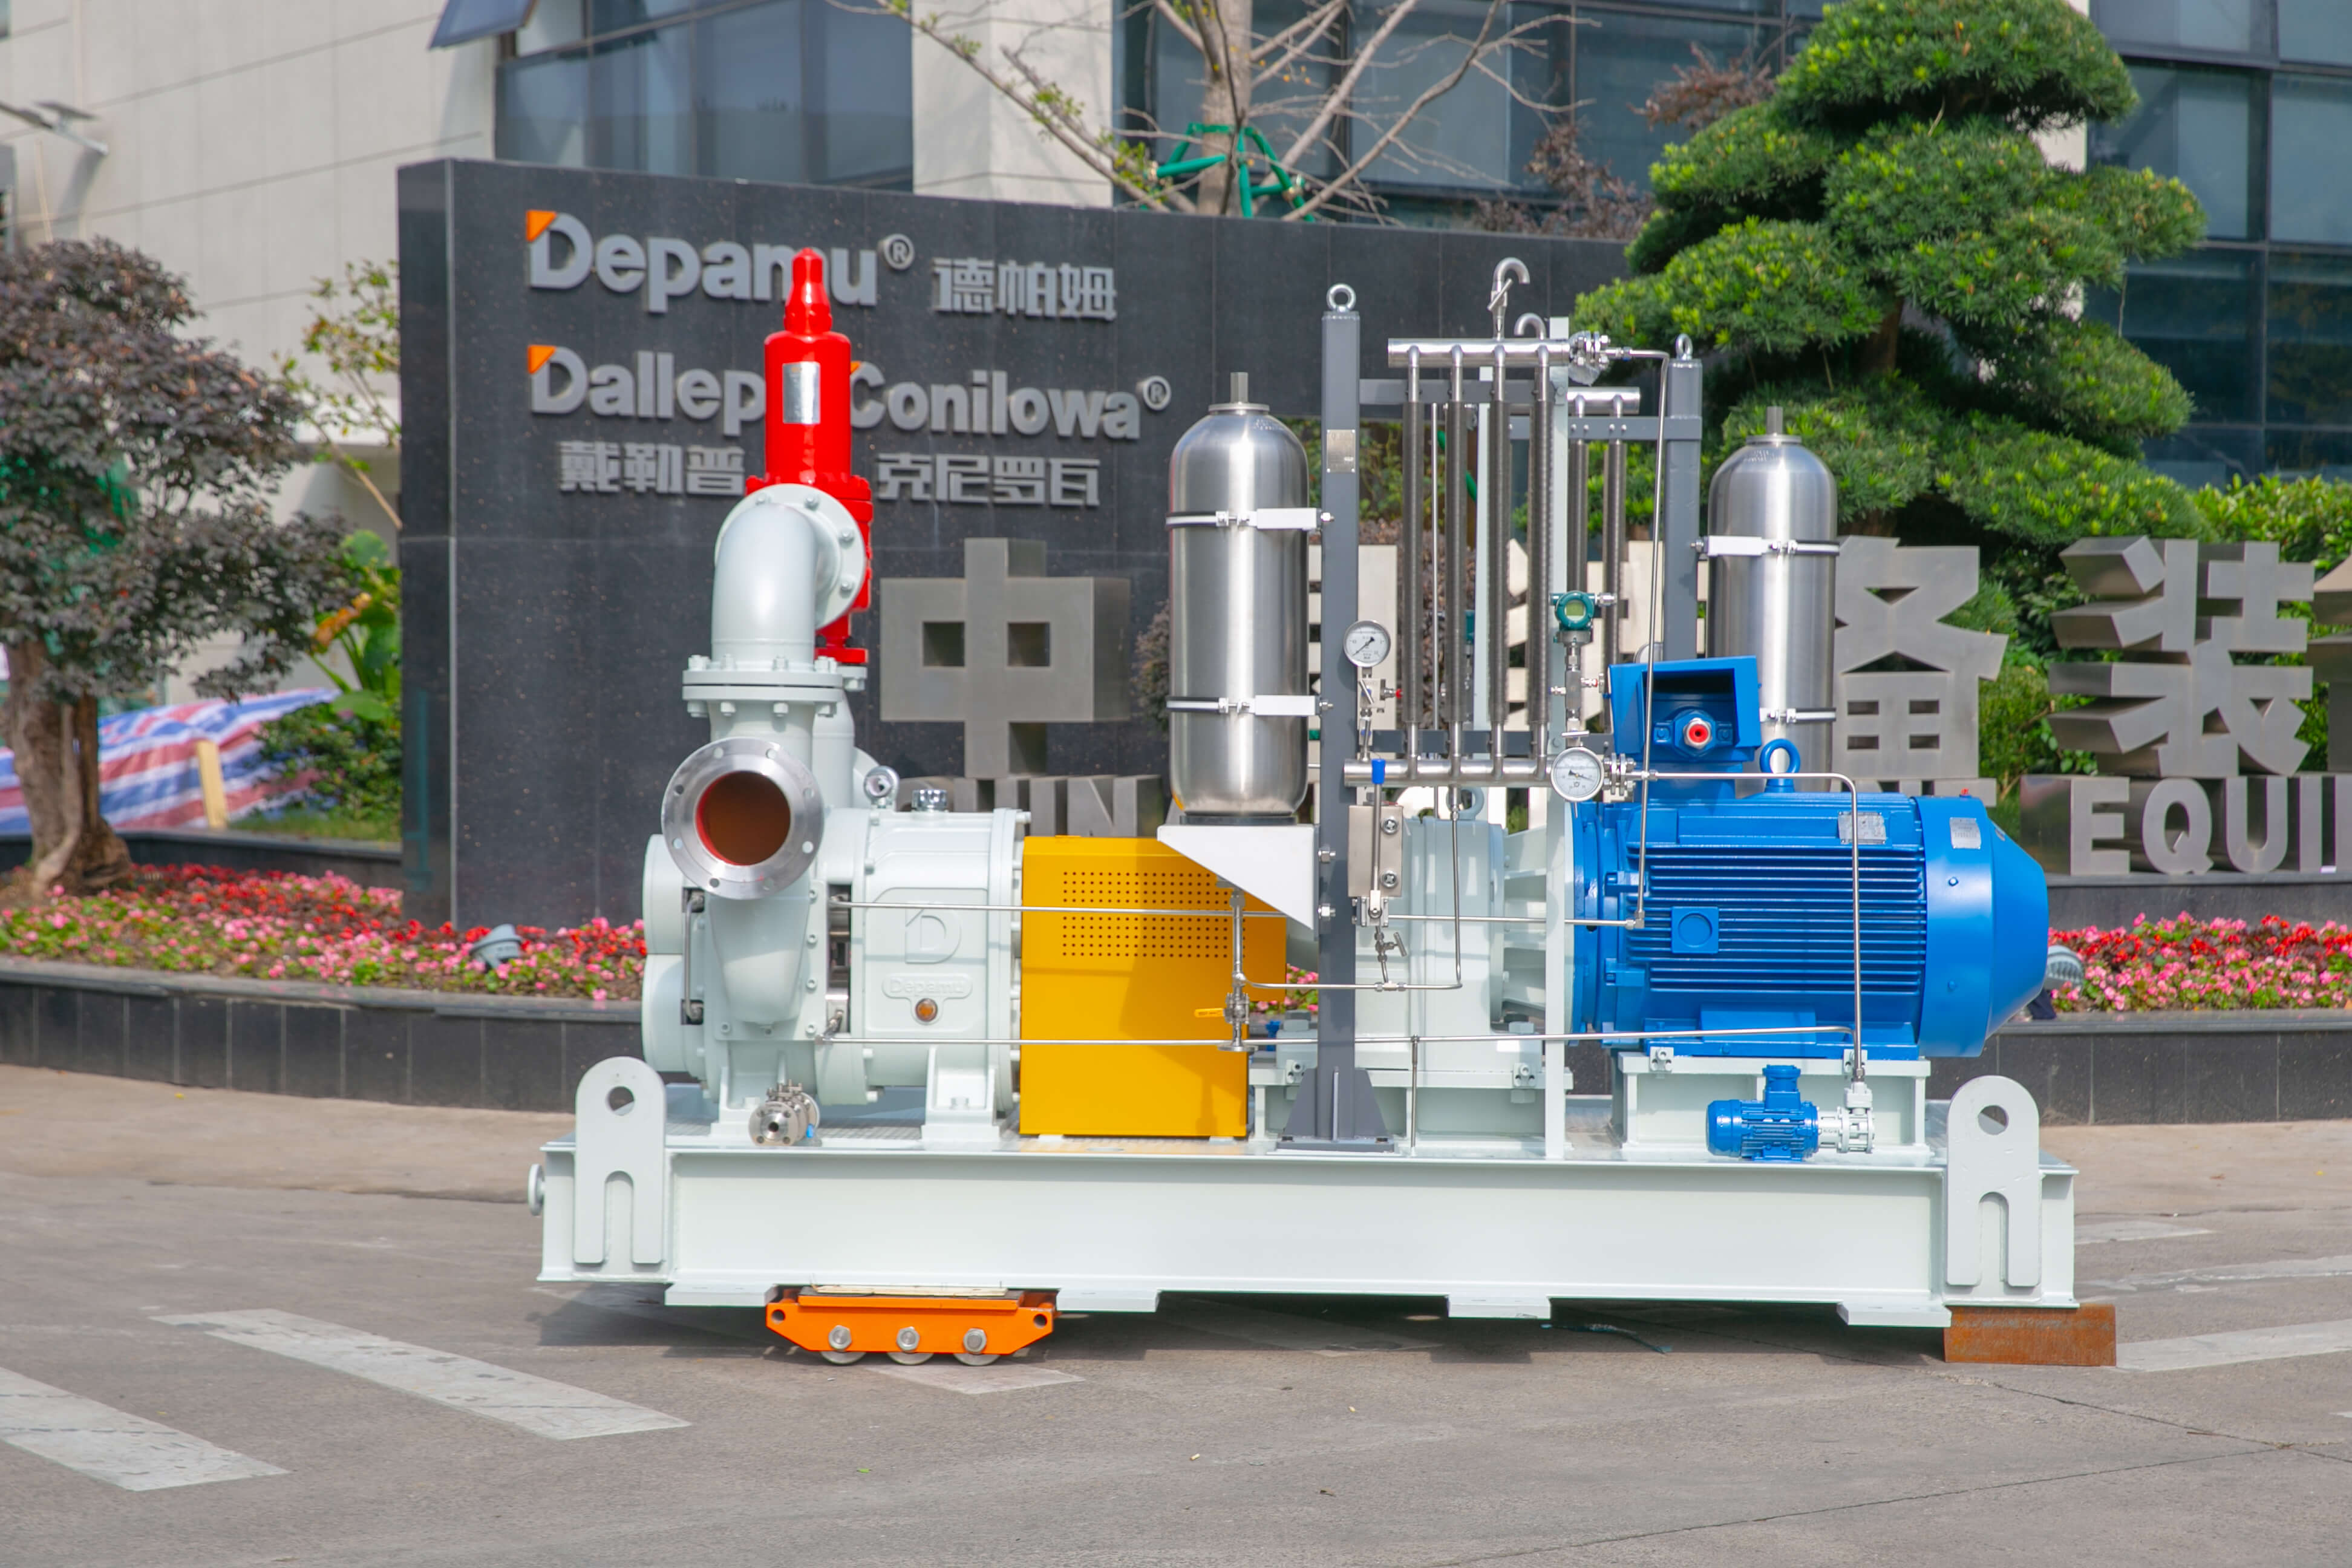
2. High-Pressure Process Reciprocating Pumps
For applications requiring extreme pressure capabilities, Depamump’s reciprocating pumps deliver unmatched performance. Using triplex or quintuplex configurations with hardened stainless steel plungers, these pumps generate pressures exceeding 35MPa while maintaining stable flow rates. Specialized materials including duplex stainless steel, Hastelloy, and titanium enable them to handle corrosive media in offshore oil production, chemical processing, and high-pressure water jetting applications.
3. Fully Integrated Chemical Dosing Systems
Understanding that modern industrial processes demand turnkey solutions, Depamump offers complete chemical dosing systems that integrate storage, dissolution, mixing, metering, and control functions. These skid-mounted systems feature:
| Component | Function |
|---|---|
| Metering Pump | Precise chemical dosing with variable speed control |
| Solution Tank | Chemical storage with level monitoring |
| Agitator | Uniform mixing of powder/liquid chemicals |
| Control Panel | PLC-based automation with remote monitoring |
These systems come pre-assembled and factory-tested, reducing installation time by up to 70% compared to traditional field-assembled solutions. The modular design allows for easy expansion or reconfiguration as process requirements evolve.
Industry-Specific Solutions
Depamump’s engineering team works closely with clients to develop tailored solutions for specific industry challenges. This approach has resulted in specialized pump designs for:
- Petrochemical Industry: Explosion-proof pumps with ATEX certification for handling volatile hydrocarbons in refinery applications
- Nuclear Power: Seismic-resistant pumps meeting RCC-M standards for primary and secondary circuit systems
- Offshore Oil: Subsea pumps with deep-water pressure ratings and corrosion-resistant coatings for FPSO operations
- Food Processing:
Sanitary pumps with 3A certification and CIP/SIP capabilities for hygienic applications
The company’s ability to combine standard product platforms with custom engineering modifications enables it to address 98% of client requirements through existing designs, while maintaining the flexibility to develop entirely new solutions for unique challenges. This balance of standardization and customization has made Depamump the preferred supplier for major international projects including Sinopec refinery expansions, CNOOC offshore platforms, and CNNC nuclear power plant construction.
Quality Assurance and Certification
Quality control permeates every stage of Depamump’s manufacturing process. From raw material inspection to final product testing, the company implements a comprehensive quality management system that complies with ISO 9001, ISO 14001, and ISO 45001 standards. Key quality measures include:
- 100% material traceability using ERP system
- Dimensional inspection with CMM machines
- Hydrostatic pressure testing up to 1.5x rated pressure
- Performance testing per API 675 standards
- NDT inspection using ultrasonic and magnetic particle methods
For critical applications, Depamump can provide pumps with additional certifications including ATEX, CE, EAC, and ASME U stamps. The company’s in-house laboratory enables it to conduct material compatibility testing for over 2,000 different chemicals, ensuring optimal pump selection for each application.
Global Service Network
Understanding that reliable operation extends beyond product quality, Depamump has established a global service network spanning 32 countries. This network includes:
- Regional warehouses stocking critical spare parts
- Certified service engineers trained on all product lines
- 24/7 technical support hotline
- Remote monitoring capabilities for predictive maintenance
- On-site commissioning and training services
The company’s “DepaCare” maintenance program offers customized service contracts that can reduce total lifecycle costs by up to 30% through proactive component replacement and system optimization. For major projects, Depamump provides dedicated project managers who coordinate all aspects of delivery, installation, and commissioning to ensure on-time, within-budget completion.
FAQ
What makes elastic rotor lobe pumps suitable for corrosive applications?
Elastic rotor lobe pumps feature an elastomer-lined rotor that provides excellent chemical resistance while maintaining precise volumetric accuracy. The elastomer material acts as a protective barrier between the process fluid and metal components, preventing corrosion and extending pump life. Depamump uses specialized elastomer compounds rated for continuous operation at temperatures up to 180°C and with pH ranges from 0-14.
How do you ensure compatibility with specific chemicals?
Our in-house chemical compatibility laboratory maintains an extensive database of over 2,000 chemicals and their interactions with different pump materials. For new applications, we conduct controlled exposure tests to verify material performance under actual operating conditions. This data-driven approach ensures we select the most appropriate elastomer lining, seal materials, and wetted parts for each chemical process.
What maintenance is required for elastic rotor lobe pumps?
These pumps require minimal maintenance compared to other positive displacement designs. Typical maintenance includes: 1) Monthly inspection of elastomer linings for wear 2) Quarterly replacement of mechanical seals if needed 3) Annual replacement of wear plates in high-abrasion applications. The modular design allows for quick component replacement without specialized tools, reducing downtime.
Can you provide pumps for explosive environments?
Yes, we offer explosion-proof pump models certified to ATEX Zone 1/21 and Class I, Division 1 standards. These pumps feature: 1) Flameproof enclosures for electrical components 2) Static grounding systems 3) Specialized seals to prevent vapor ingress 4) Temperature monitoring sensors. We can also provide pneumatic-driven pumps for areas where electrical power cannot be used safely.
What is the lead time for custom pump orders?
Standard models ship within 4-6 weeks of order confirmation. For custom designs requiring engineering modifications, lead times typically range from 8-12 weeks depending on complexity. We maintain strategic inventory of common components to expedite custom orders, and our modular design approach allows us to incorporate most modifications without complete re-engineering.
Summary
As a specialized elastic rotor lobe pump manufacturer, Depamump combines German engineering heritage with Chinese manufacturing efficiency to deliver world-class fluid handling solutions. The company’s comprehensive product range, from precision metering pumps to high-pressure reciprocating systems, addresses the full spectrum of industrial pumping requirements. With a focus on customization, quality, and service, Depamump has established itself as the preferred supplier for multinational corporations operating in demanding sectors including petrochemical, nuclear power, and offshore oil and gas. The company’s commitment to continuous innovation ensures it remains at the forefront of pump technology development, providing clients with reliable, efficient, and cost-effective solutions for their most critical fluid handling challenges.