
When selecting industrial fluid handling equipment, precision, reliability, and adaptability are critical factors that determine operational efficiency and safety. Depamp (Hangzhou) Pump Technology Co., Ltd., established in 2003, has positioned itself as a global leader in the development and manufacturing of high-performance fluid equipment, including the specialized double helix parallel pump. With over 400 employees, a 35,000-square-meter production facility, and annual revenue exceeding 500 million RMB, our company combines German engineering expertise with continuous innovation to deliver solutions that meet the most demanding industrial requirements.
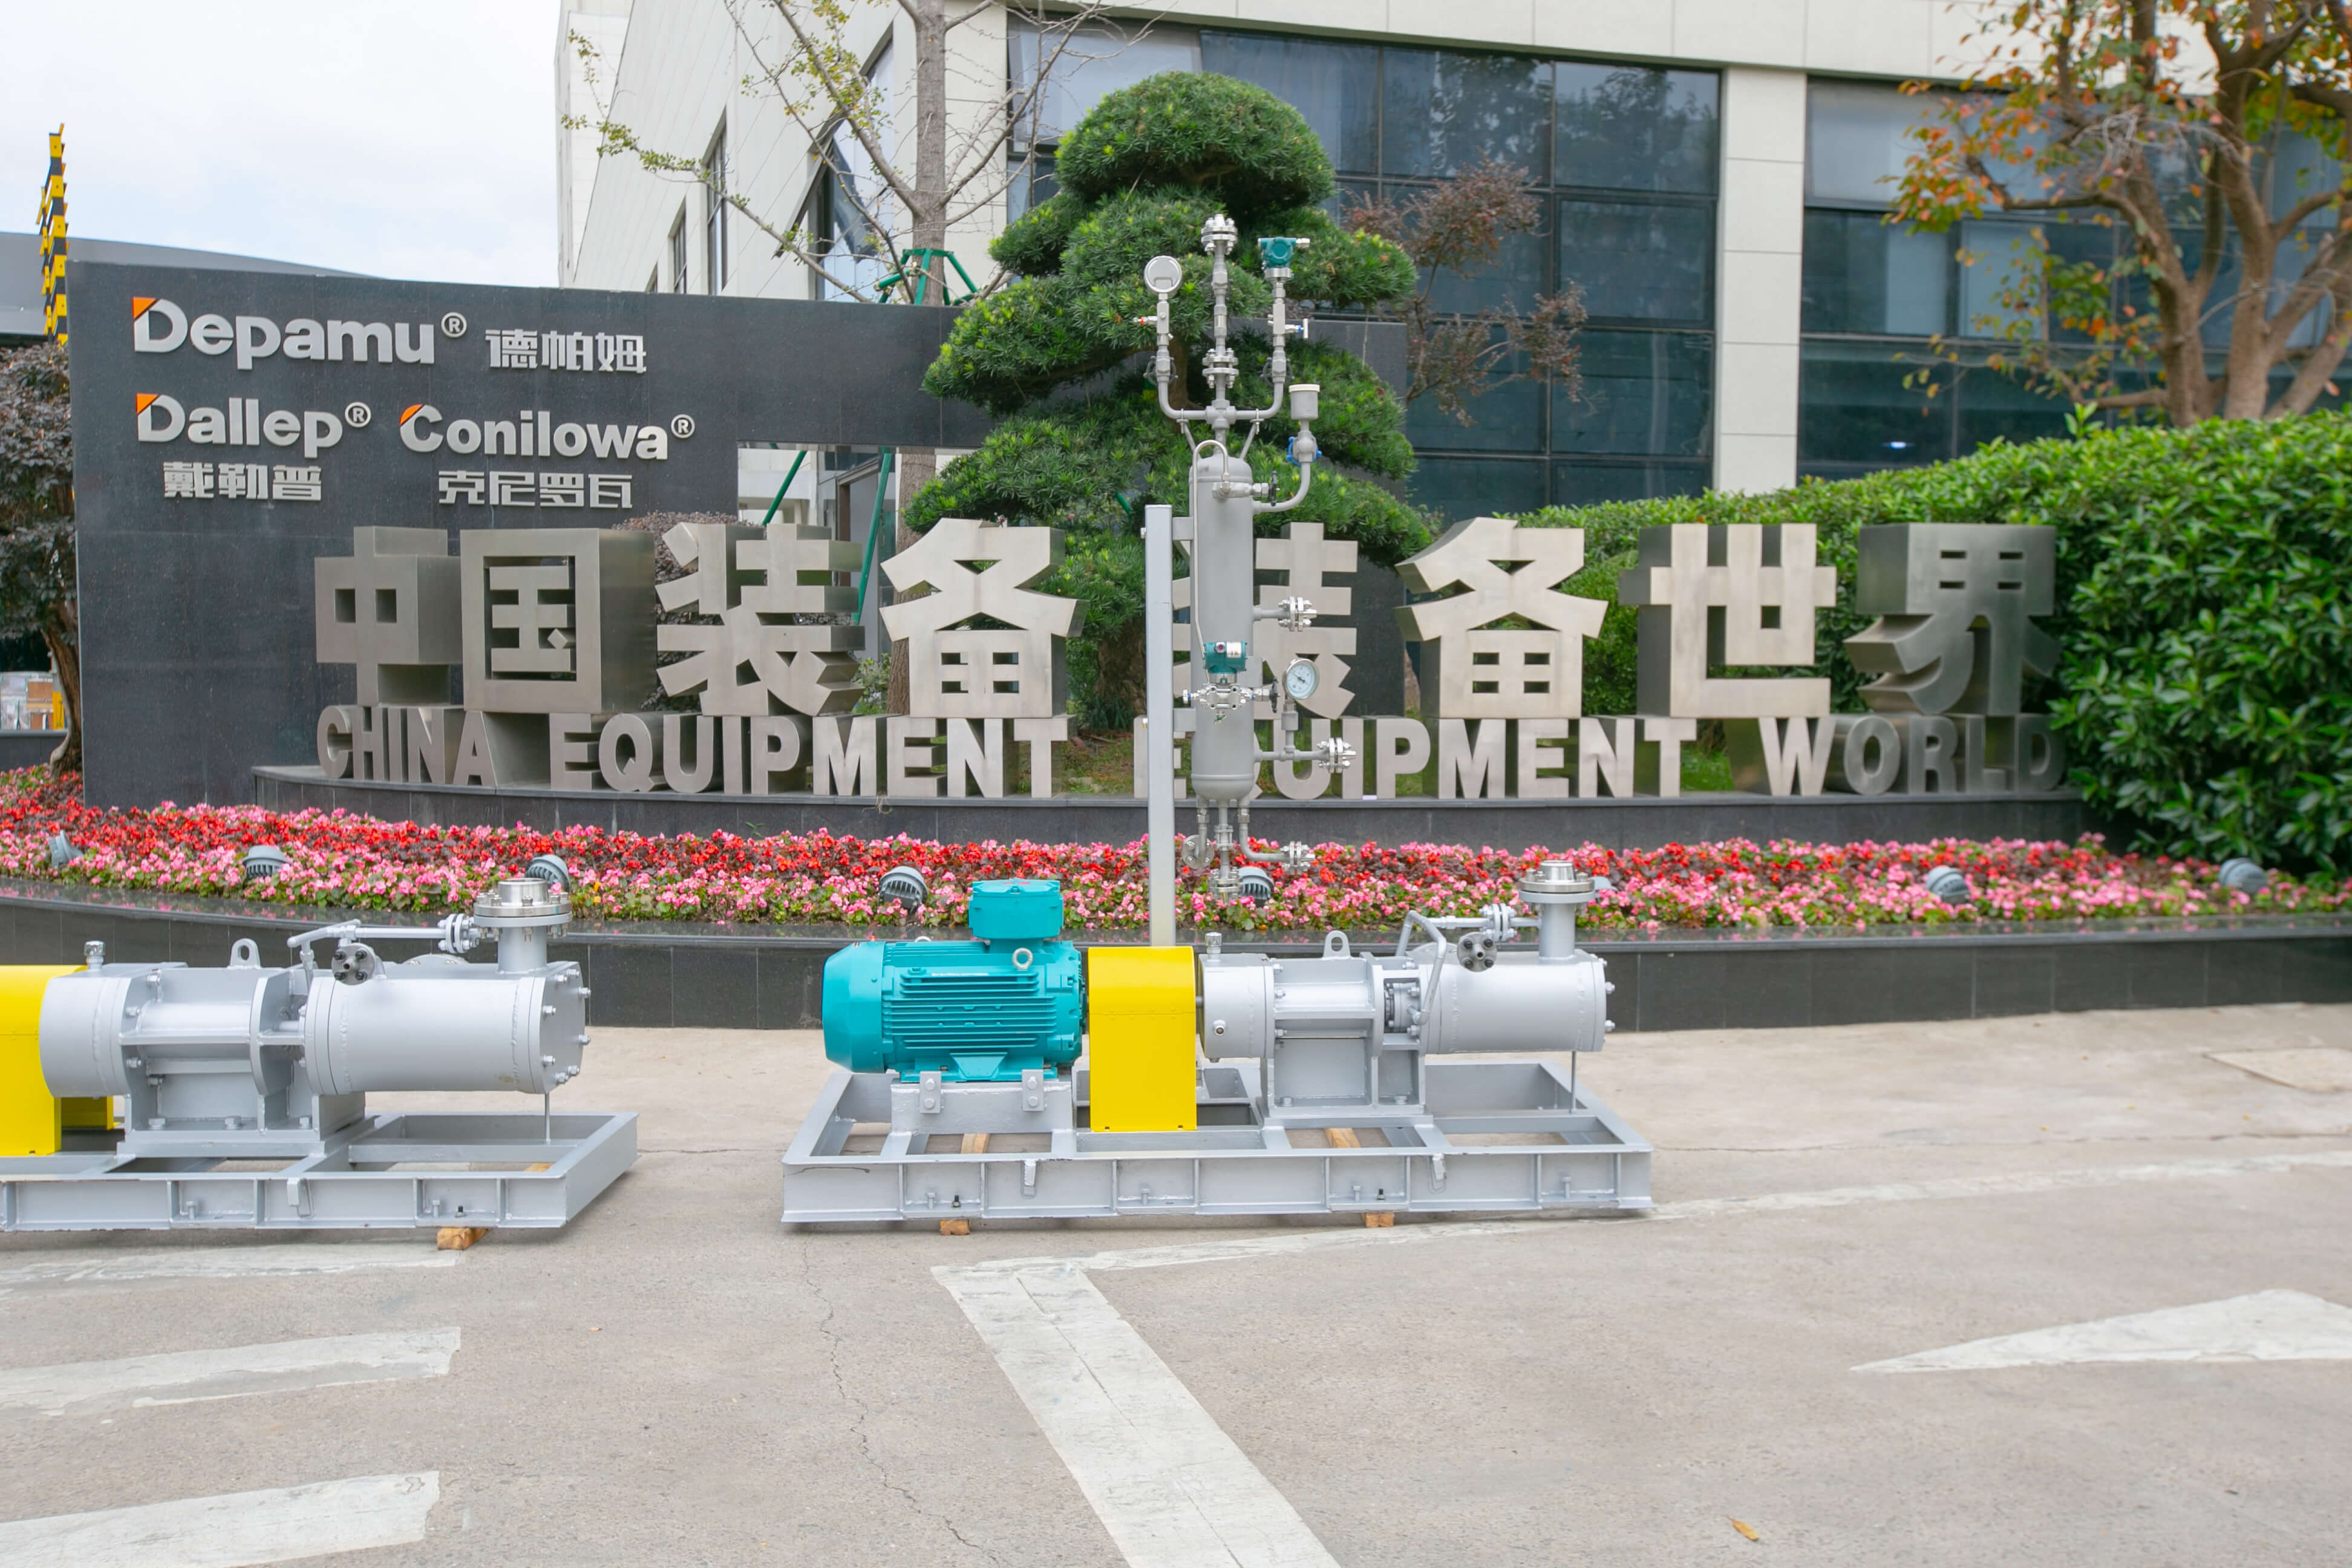
Understanding Double Helix Parallel Pump Technology
The double helix parallel pump represents a breakthrough in fluid handling technology, designed specifically for applications requiring precise metering, high-pressure transfer, and reliable operation with complex media. Unlike conventional pumps, this innovative design features twin helical rotors that rotate in parallel, creating a consistent flow path with minimal pulsation. This configuration enables exceptional accuracy in chemical dosing applications while maintaining stable performance even when handling viscous, abrasive, or shear-sensitive fluids.
Our engineering team has optimized the double helix parallel pump’s geometry to achieve optimal volumetric efficiency and mechanical reliability. The pump’s casing and rotor materials are carefully selected based on the specific media characteristics, with options including stainless steel, duplex steel, and specialized alloys for corrosive environments. This material flexibility ensures compatibility with a wide range of industrial chemicals used in petrochemical processing, water treatment, and power generation applications.
Key Applications Across Industries
The versatility of our double helix parallel pumps makes them indispensable in several critical industries. In the petrochemical sector, these pumps play a vital role in catalyst injection systems, where precise dosing of chemical additives directly impacts reaction efficiency and product quality. The pumps’ ability to maintain consistent flow rates under varying pressure conditions ensures optimal process control and reduces material waste.
For oil and gas applications, our double helix parallel pumps excel in well stimulation and chemical injection operations. The robust construction withstands harsh operating environments, while the precise metering capability supports effective scale inhibition, corrosion protection, and enhanced oil recovery processes. In nuclear power facilities, these pumps provide reliable service for boron injection systems, where safety and accuracy are paramount.
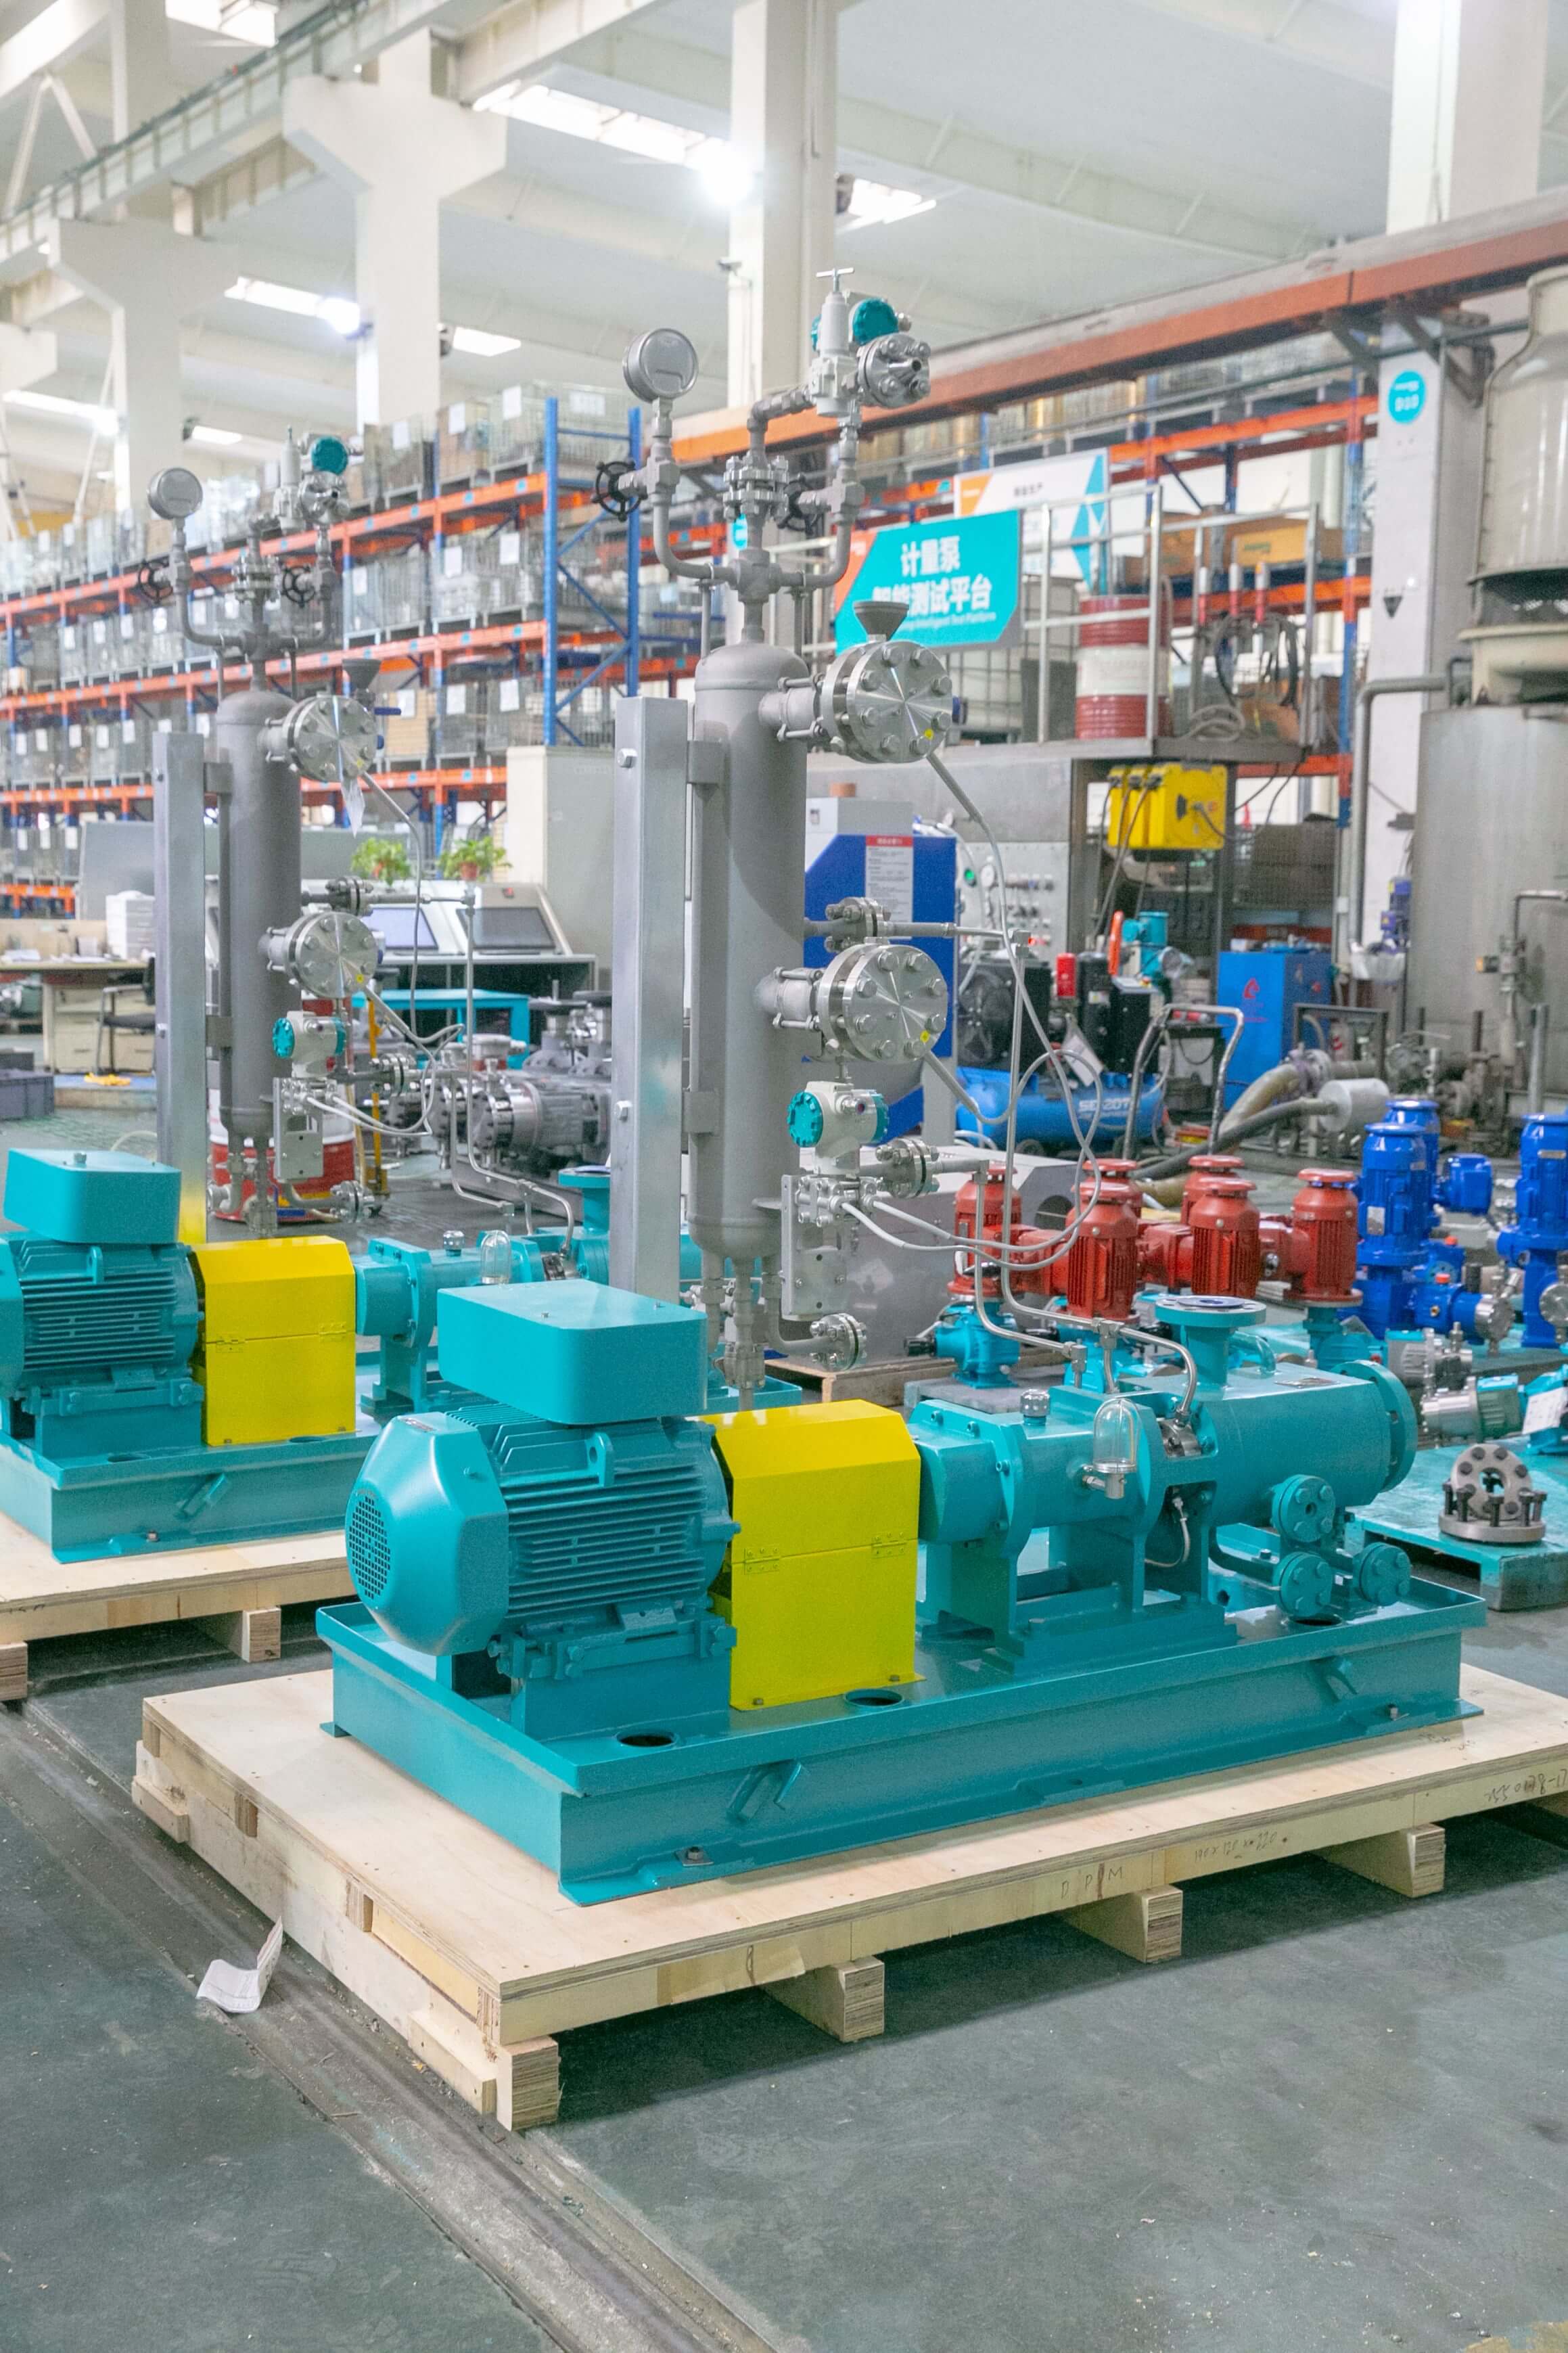
Technical Specifications and Performance Advantages
Our double helix parallel pumps are engineered to deliver exceptional performance across a wide operating range. Standard models offer flow capacities from 0.5 to 500 L/h with pressure ratings up to 400 bar, while custom designs can accommodate even more demanding specifications. The pumps’ modular construction allows for easy maintenance and component replacement, minimizing downtime during service intervals.
One of the most significant advantages of our double helix parallel pump technology is its energy efficiency. The optimized rotor profile reduces internal friction, resulting in lower power consumption compared to traditional gear or lobe pumps. This efficiency translates to measurable cost savings over the pump’s operational lifecycle, particularly in continuous-duty applications.
| Parameter | Specification Range |
|---|---|
| Flow Rate | 0.5 – 500 L/h (customizable) |
| Pressure Rating | Up to 400 bar |
| Viscosity Range | 1 – 1,000,000 cSt |
| Temperature Range | -40°C to +350°C |
| Material Options | SS304, SS316, Duplex, Hastelloy, etc. |
Comprehensive Product Range for Diverse Needs
While the double helix parallel pump represents our flagship technology, Depamp offers a complete portfolio of fluid handling solutions to address various industrial challenges. Our metering pump range includes hydraulic diaphragm models capable of handling corrosive chemicals with zero leakage, making them ideal for pharmaceutical and food processing applications. The high-pressure process reciprocating pumps deliver exceptional performance in oilfield injection and pipeline transfer operations, with pressure capabilities exceeding 35 MPa.
For complete system solutions, our automatic chemical dosing units integrate storage, dissolution, mixing, metering, and control functions into a single skid-mounted package. These turnkey systems simplify installation and commissioning while ensuring precise chemical delivery in boiler water treatment, wastewater processing, and petrochemical applications. The intelligent control systems support remote monitoring and automatic adjustment based on process parameters, enhancing operational reliability.
Customization Capabilities and Engineering Support
What truly sets Depamp apart is our commitment to providing tailored solutions that align perfectly with each customer’s unique requirements. Our engineering team works closely with clients to analyze process conditions, media characteristics, and performance objectives before recommending the most suitable pump configuration or system design.
For complex applications involving non-standard media or extreme operating conditions, we offer complete customization services. This includes specialized materials selection, unique sealing arrangements, and custom control interfaces to ensure seamless integration with existing process systems. Our state-of-the-art manufacturing facilities and quality management system (ISO 9001 certified) guarantee that every customized solution meets the highest standards of reliability and performance.
FAQ
What makes double helix parallel pumps different from other positive displacement pumps?
Double helix parallel pumps feature twin helical rotors that rotate in parallel, creating a smooth, consistent flow path with minimal pulsation. This design offers superior metering accuracy compared to gear pumps and better handling of viscous fluids than lobe pumps, while maintaining mechanical reliability under high-pressure conditions.
Can your pumps handle abrasive or corrosive media?
Yes, our pumps are designed with material flexibility to accommodate various media types. We offer construction materials ranging from standard stainless steels to specialized alloys like Hastelloy and duplex steel, depending on the chemical composition and operating conditions of your application.
What pressure ratings are available for your industrial pumps?
Our product range includes pumps with pressure ratings from vacuum conditions up to 400 bar, depending on the specific model and configuration. The high-pressure process reciprocating pumps in our portfolio are particularly well-suited for applications requiring pressures above 35 MPa.
How do you ensure the accuracy of chemical dosing systems?
Our chemical dosing systems incorporate precision metering pumps with adjustable stroke length and frequency control, allowing for fine-tuning of dosage rates. The integrated control systems continuously monitor process parameters and automatically adjust pump output to maintain consistent chemical concentration, even with varying flow conditions.
Summary
Depamp (Hangzhou) Pump Technology Co., Ltd. stands as a trusted partner for industrial fluid handling solutions, combining advanced engineering with practical expertise to deliver equipment that enhances process efficiency and reliability. Our double helix parallel pumps represent the pinnacle of precision metering technology, while our comprehensive product range addresses virtually every fluid transfer and dosing requirement across multiple industries. With a strong focus on customization and customer support, we continue to push the boundaries of what’s possible in industrial pump technology, helping our clients achieve their operational objectives while maintaining the highest standards of safety and environmental responsibility.