
Selecting the right industrial pump for your specific application requires careful consideration of multiple factors including fluid characteristics, operating conditions, and system requirements. As a leading manufacturer of high-end positive displacement pumps and fluid equipment since 2003, Depamp (Hangzhou) Pump Technology Co., Ltd. has helped thousands of clients across petrochemical, nuclear power, metallurgy, and environmental protection industries solve their most challenging fluid handling problems. This comprehensive guide will walk you through the key considerations for elastic rotor lobe pump selection while introducing our complete range of industrial pump solutions.
Understanding Elastic Rotor Lobe Pump Technology
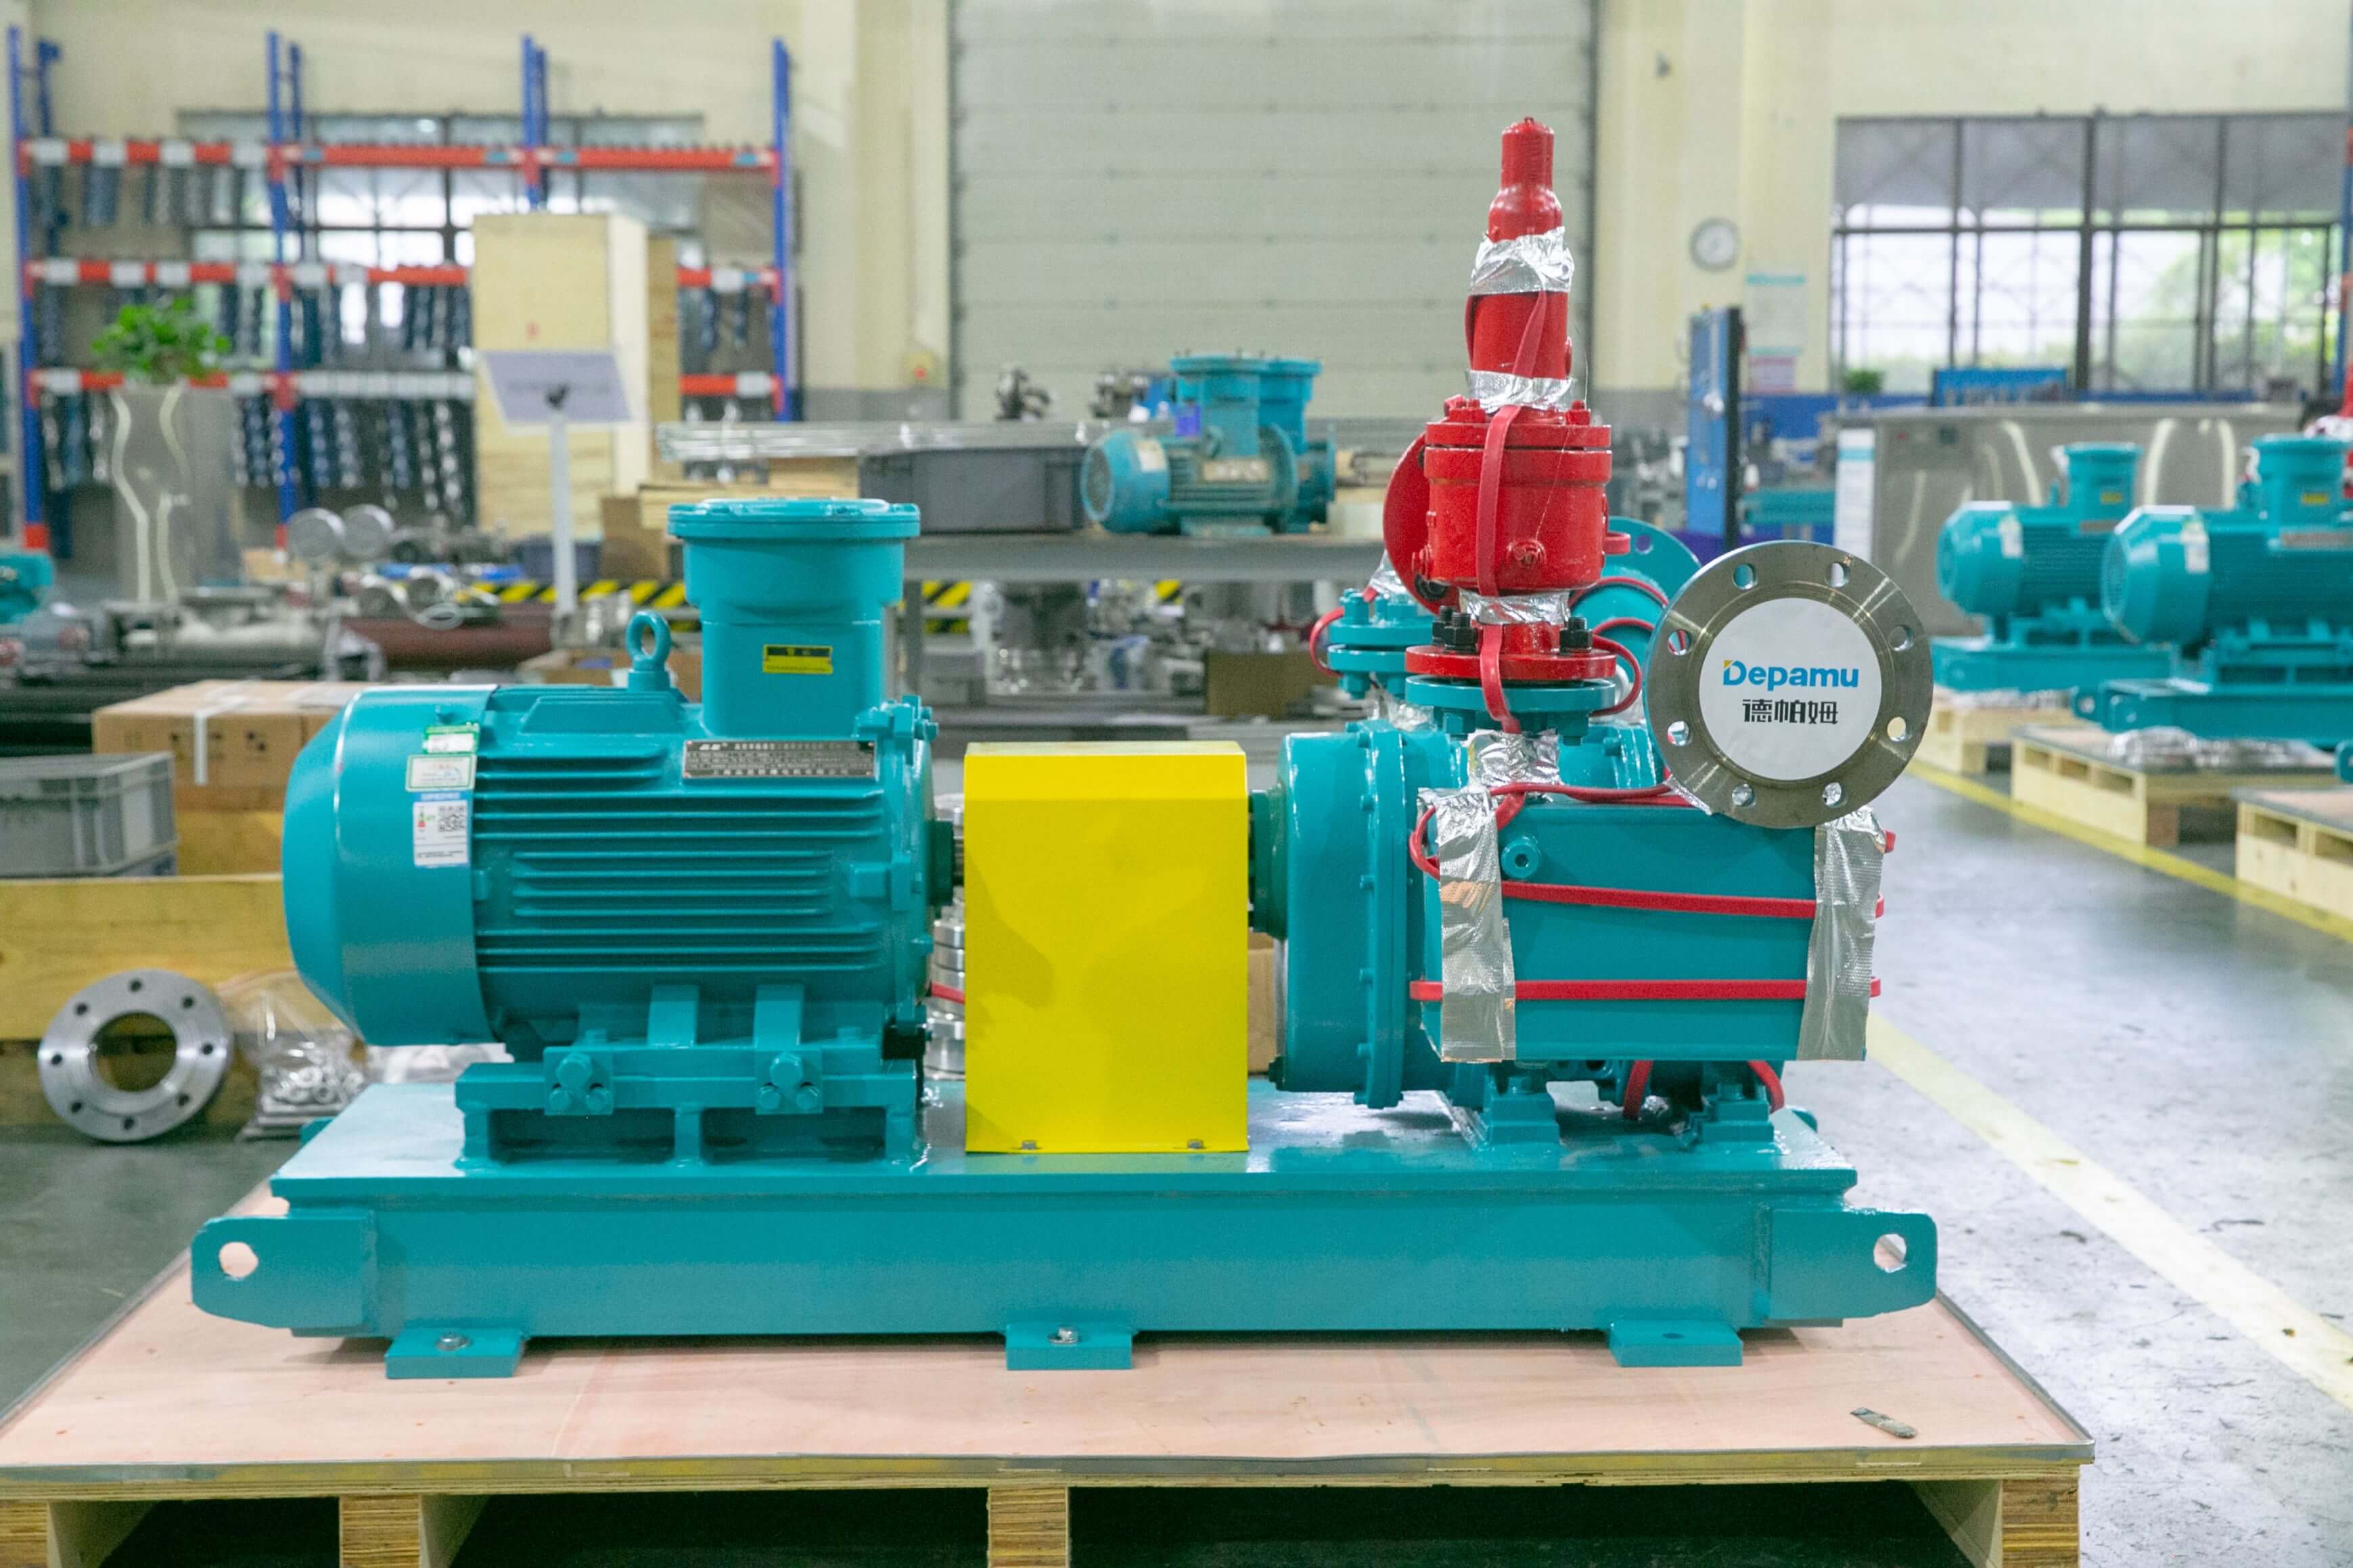
Elastic rotor lobe pumps, also known as rotary piston pumps, belong to the positive displacement pump family that uses rotating lobes to move fluids through the pump chamber. Unlike traditional gear pumps or screw pumps, our elastic rotor lobe pumps feature specially designed rubber-coated rotors that provide exceptional performance in handling:
- Corrosive chemicals and acids
- Viscous fluids up to 1,000,000 cP
- Solids-laden slurries with up to 30% solids content
- Shear-sensitive products like food emulsions
- Abrasive slurries in mining applications
The key advantage of our elastic rotor lobe pumps lies in their self-priming capability (up to 9 meters), reversible flow direction, and gentle pumping action that minimizes product degradation. With flow rates ranging from 0.5 to 200 m³/h and pressure capabilities up to 1.6 MPa, these pumps serve as ideal solutions for chemical transfer, wastewater treatment, food processing, and pulp & paper industries.
Critical Selection Criteria for Rotary Piston Pumps
When evaluating different rotary piston pump options, consider these essential parameters to ensure optimal performance and reliability:
1. Fluid Compatibility Analysis
The chemical composition of your process fluid directly impacts material selection for pump components. Our engineering team conducts comprehensive compatibility tests to determine the most suitable elastomer materials (NBR, FKM, EPDM, etc.) and metallurgical options (stainless steel 304/316, duplex steel, Hastelloy) for your specific application. For example, our food-grade pumps feature FDA-compliant materials and sanitary finishes for dairy processing applications.
2. Viscosity Handling Capacity
Viscosity significantly affects pump performance and energy consumption. Our elastic rotor lobe pumps maintain consistent flow rates across viscosity ranges from 1 cP to 1,000,000 cP without requiring speed adjustments. For high-viscosity applications like asphalt transfer, we recommend pumps with larger rotor chambers and reduced operating speeds to minimize shear forces.
3. Solids Handling Requirements
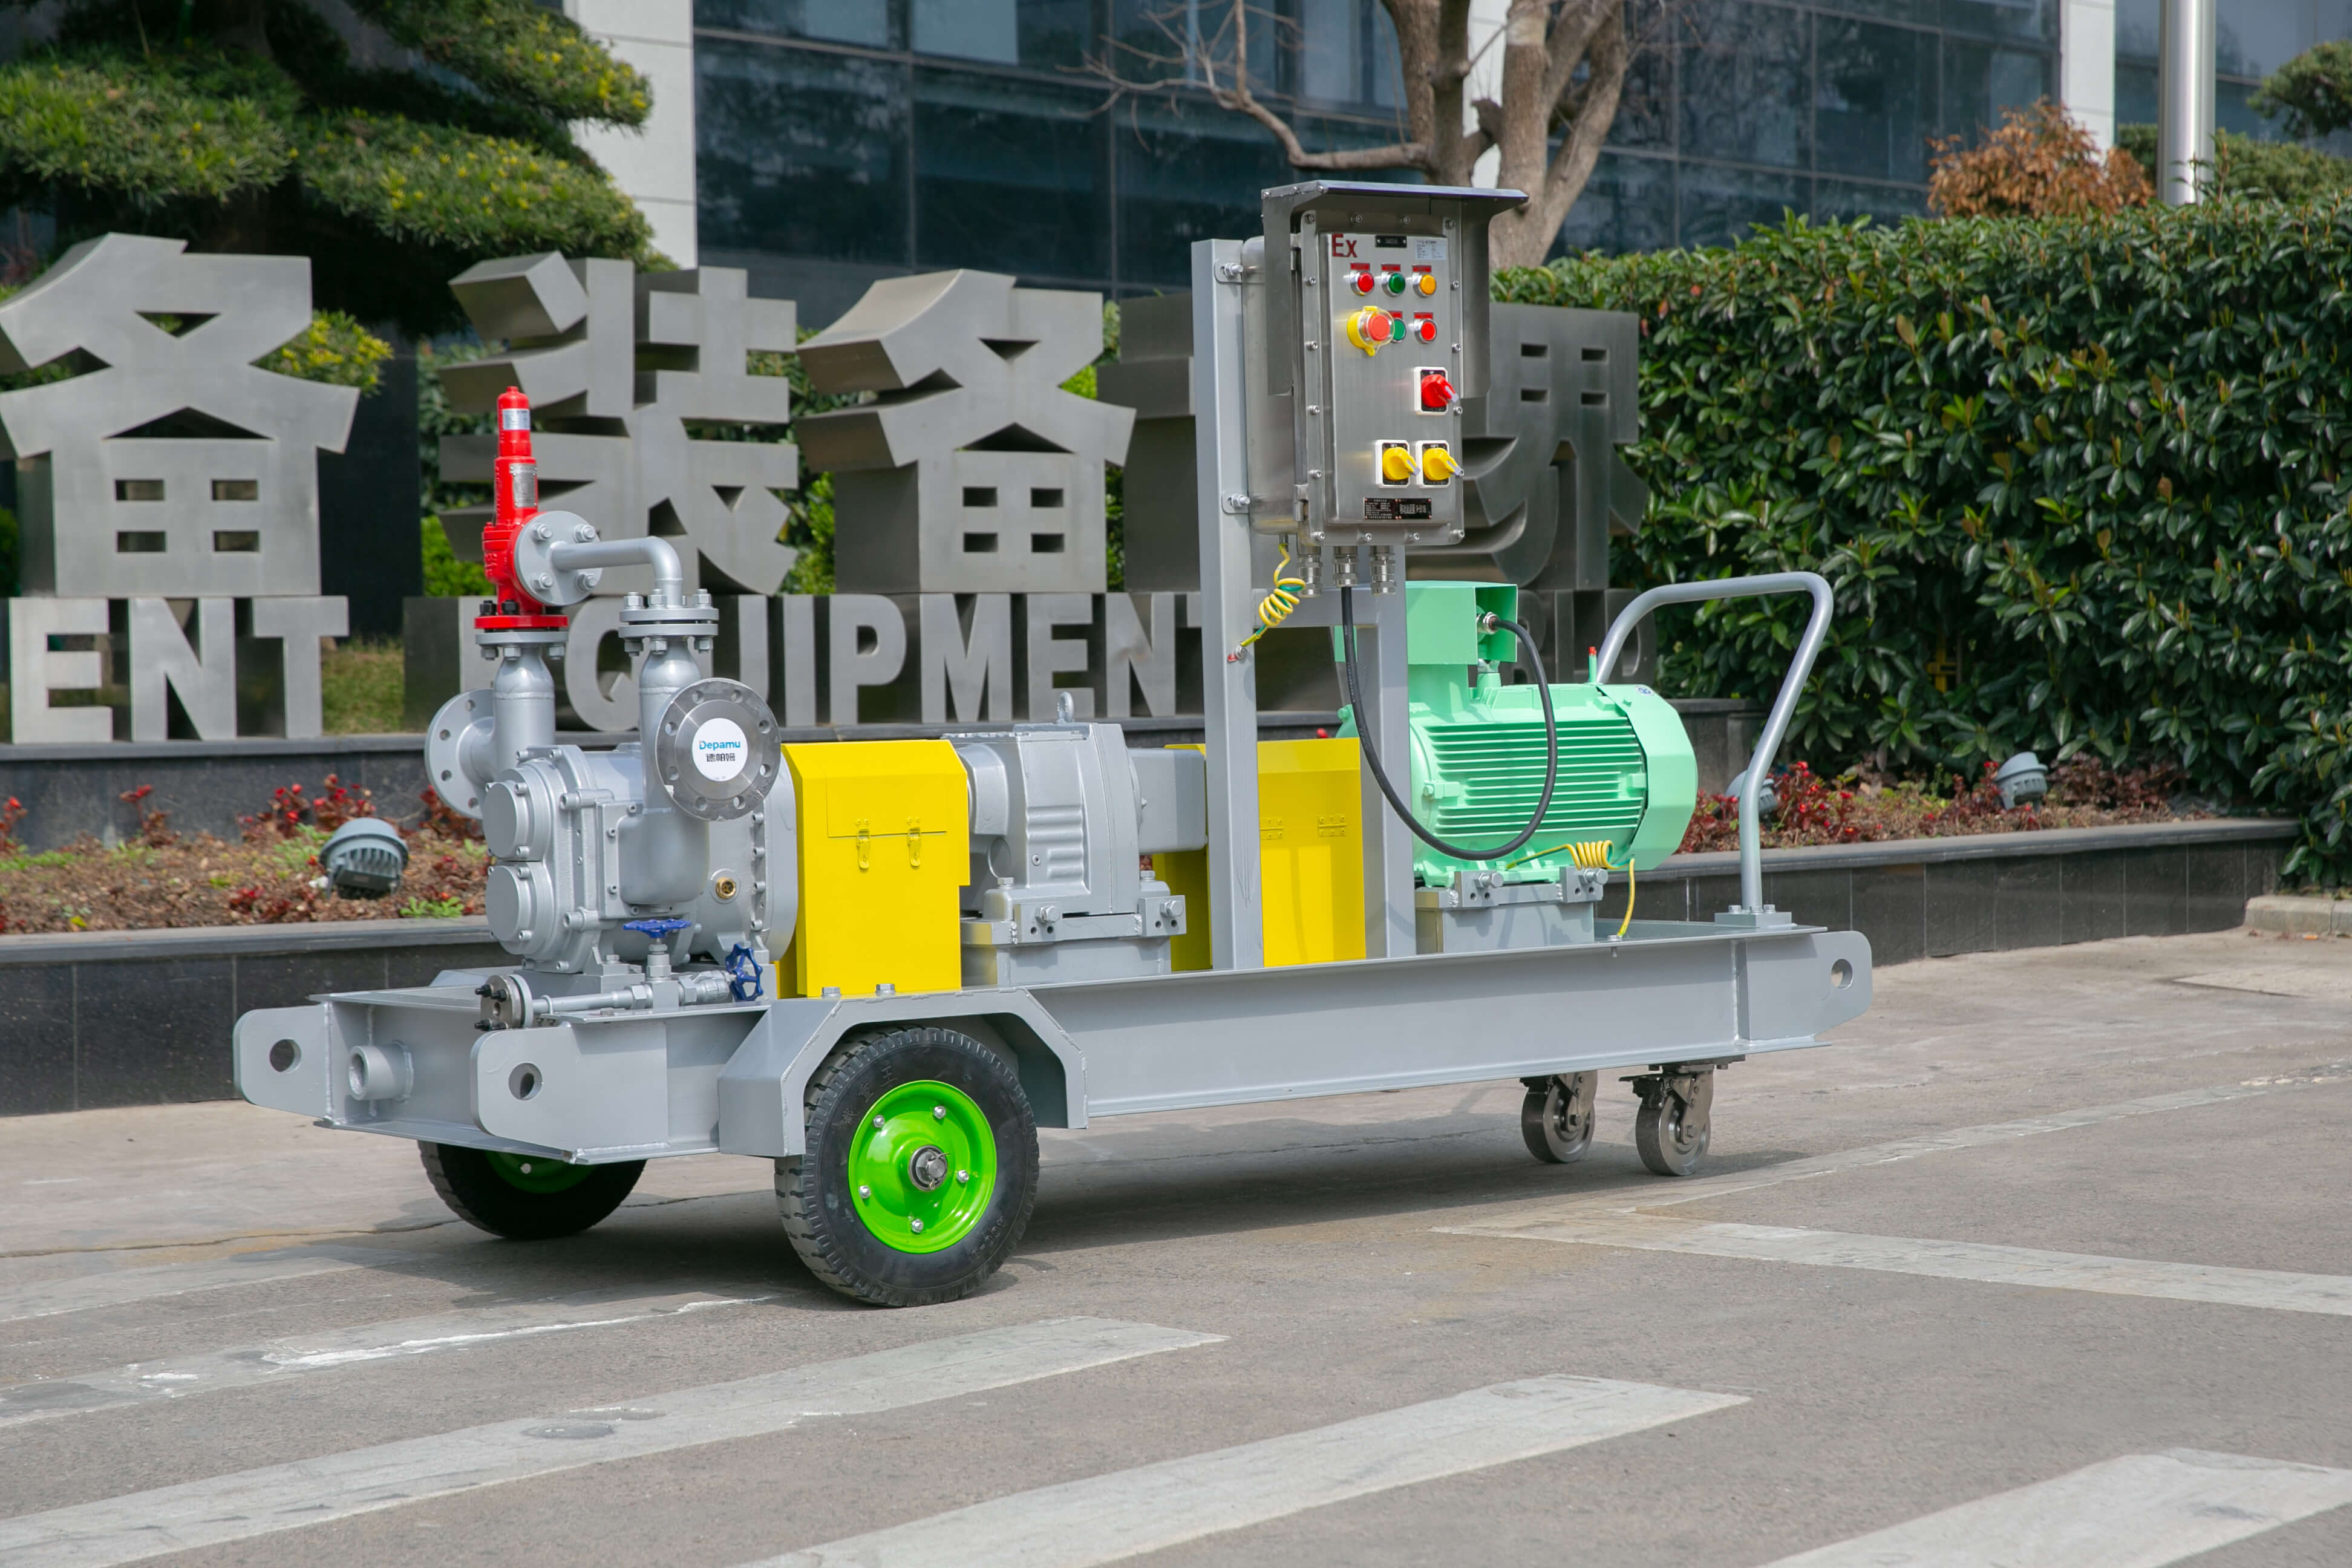
The presence of solids in your process fluid necessitates special design considerations. Our heavy-duty rotary piston pumps feature oversized rotor chambers and hardened liners to handle abrasive slurries with up to 30% solids by volume. For applications involving large particles (up to 15mm), we offer pumps with specially contoured rotors that prevent clogging while maintaining volumetric efficiency.
4. Temperature and Pressure Ratings
Process conditions determine the required construction materials and sealing solutions. Our standard pumps handle temperatures from -30°C to +150°C, with custom options available for cryogenic or high-temperature applications up to +200°C. For high-pressure systems, we offer multi-stage pump configurations capable of generating pressures exceeding 4.0 MPa while maintaining leak-free operation through our proprietary mechanical seal designs.
| Parameter | Standard Range | Custom Options |
|---|---|---|
| Flow Rate | 0.5-200 m³/h | Up to 500 m³/h |
| Pressure | Up to 1.6 MPa | Up to 4.0 MPa |
| Temperature | -30°C to +150°C | -50°C to +200°C |
| Viscosity | 1-1,000,000 cP | Special designs available |
Complete Industrial Pump Solutions Portfolio
Beyond our elastic rotor lobe pumps, Depamp offers a comprehensive range of industrial pump solutions tailored to diverse applications:
1. Metering Pumps for Precise Chemical Dosing
Our hydraulic diaphragm metering pumps achieve ±1% accuracy through adjustable stroke length and frequency control. With pressure capabilities up to 400 bar and flow rates from 0.03 to 50,000 L/h, these pumps serve as the “precise injectors” in water treatment, pharmaceutical, and oilfield chemical injection applications. The double diaphragm design with leak detection ensures completely leak-free operation even with corrosive or toxic media.
2. High-Pressure Process Reciprocating Pumps
Designed as industrial pipeline “power boosters”, our reciprocating pumps generate pressures exceeding 35 MPa while maintaining stable flow rates. The triplex plunger design with hardened stainless steel plungers and ceramic-lined cylinders enables continuous operation with high-temperature, high-viscosity, and solids-laden fluids. Typical applications include oilfield fracturing, pipeline pressure testing, and desalination plant operation.
3. Automated Chemical Dosing Systems
Our skid-mounted dosing systems integrate storage tanks, mixing units, metering pumps, and PLC control panels into complete “chemical preparation stations”. These turnkey solutions support multiple dosing points, dry/liquid feed options, and automatic pH/ORP control. Pre-assembled and factory-tested units reduce installation time by 70% while ensuring reliable operation in boiler water treatment, cooling tower management, and wastewater neutralization applications.
FAQ
What makes elastic rotor lobe pumps different from other positive displacement pumps?
Elastic rotor lobe pumps feature rubber-coated rotors that create a gentle pumping action ideal for shear-sensitive products. Unlike gear pumps that generate high shear forces or screw pumps that require precise alignment, our rotary piston pumps offer superior solids handling capacity (up to 30% solids) and corrosion resistance through their elastomer-lined chambers. The self-priming capability (up to 9m) and reversible flow direction provide operational flexibility not found in traditional PD pumps.
How do you ensure chemical compatibility with our process fluids?
Our material selection process involves three critical steps: 1) Analyzing your fluid’s chemical composition and operating conditions; 2) Conducting compatibility tests per ASTM D543 standards; 3) Selecting from 12 different elastomer formulations (NBR, FKM, EPDM, etc.) and 8 metallurgical options. For complex mixtures, we create custom compound formulations that maintain physical properties under prolonged exposure to aggressive chemicals at elevated temperatures.
What maintenance procedures are required for rotary piston pumps?
Regular maintenance includes: 1) Monthly inspection of mechanical seals and lubrication points; 2) Quarterly replacement of wear parts like rotors and liners (based on operating hours); 3) Annual overhaul of bearings and drive components. Our pumps feature quick-access covers that enable rotor replacement in under 30 minutes without special tools. We provide preventive maintenance kits containing all required spare parts for your specific operating conditions.
Can you provide customized pump solutions for unique applications?
Absolutely. Over 35% of our annual production comprises custom-engineered solutions. Our R&D team works closely with clients to develop pumps for: 1) Cryogenic applications (-196°C) using special lubricants and materials; 2) High-temperature processes (200°C) with cooling jackets and heat-resistant seals; 3) Aseptic processing with steam-in-place (SIP) capabilities; 4) Explosion-proof environments meeting ATEX Zone 1/21 standards. Each custom design undergoes FEA simulation and prototype testing before production.
Summary
Selecting the right industrial pump requires balancing technical specifications with operational requirements and long-term costs. Depamp’s elastic rotor lobe pumps offer unmatched versatility in handling corrosive, viscous, and solids-laden fluids while our complete pump portfolio addresses every fluid handling challenge from precise metering to high-pressure transfer. With 22 years of manufacturing expertise, 400+ skilled employees, and 35,000㎡ production facilities, we deliver reliable, customized solutions that reduce total cost of ownership through energy efficiency, minimal maintenance, and extended service life. Contact our technical team today to discuss your specific application requirements.