
In industrial applications requiring precise fluid handling under challenging conditions, the right pumping solution makes all the difference. Depamp (Hangzhou) Pump Technology Co., Ltd. has established itself as a global leader in customized concentrate slurry pump manufacturing since 2003, serving diverse industries with innovative fluid transfer solutions. With 400+ employees across a 35,000m² production facility and annual output exceeding 500 million RMB, our company delivers comprehensive pump solutions tailored to your specific operational requirements.
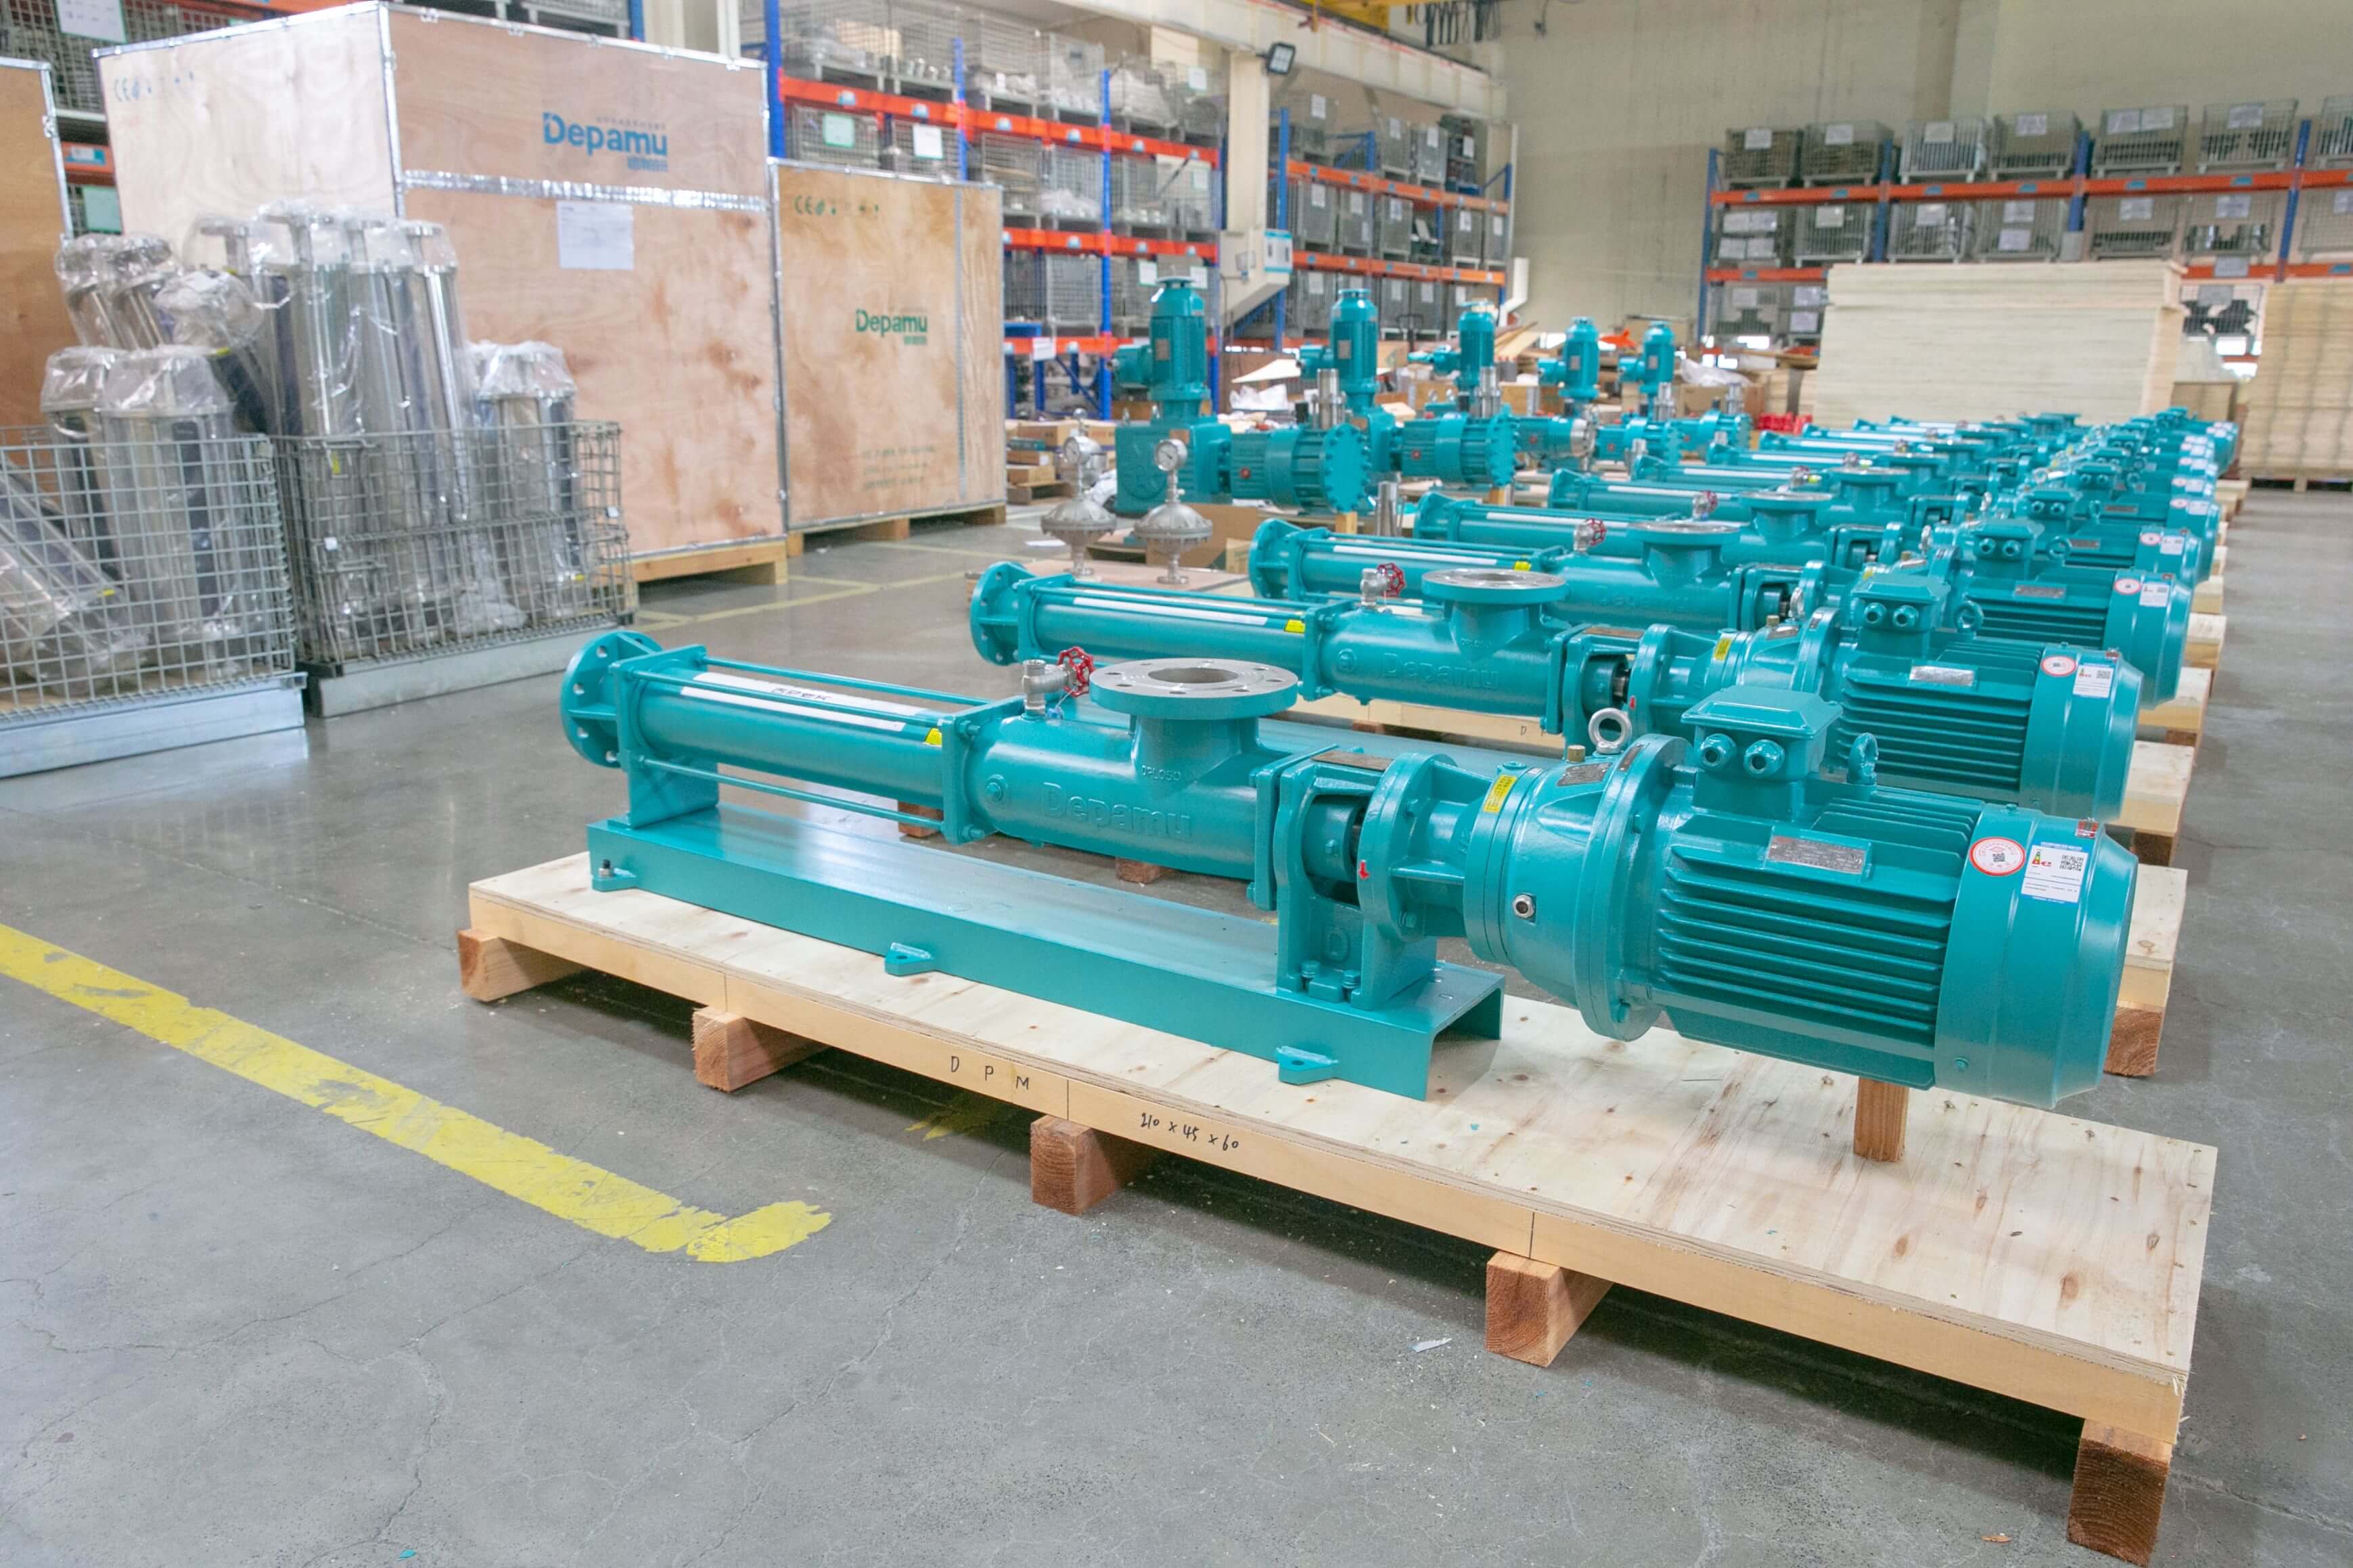
Understanding Concentrate Slurry Pump Applications
Concentrate slurry pumps represent specialized equipment designed to handle abrasive, corrosive, and high-density mixtures commonly found in mining operations, chemical processing, and industrial manufacturing. These heavy-duty pumps must withstand extreme conditions while maintaining precise flow control and operational reliability. Our engineering team develops customized solutions that address:
- Particle size and concentration variations
- Corrosive chemical compositions
- High-pressure transfer requirements
- Temperature extremes in processing environments
- Continuous operation demands
The petrochemical and refining sector accounts for 41% of our business, with oil and gas field applications contributing another 23%. This market dominance stems from our ability to engineer pumps that meet stringent industry standards while delivering exceptional performance in demanding environments. Our hydraulic diaphragm metering pumps, for example, achieve injection accuracy within ±1%, making them ideal for chemical dosing applications where precision is critical.
Custom Pump Manufacturing Capabilities
As a vertically integrated manufacturer, we control every aspect of the production process from initial design through final testing. Our customization capabilities include:
Material Selection: We offer multiple construction materials including stainless steel, duplex steel, Hastelloy, and titanium alloys to match your specific corrosion resistance requirements. For abrasive slurry applications, our pumps feature hardened wear components with specialized coatings that extend service life by up to 300% compared to standard materials.
Hydraulic Design: Our engineering team employs advanced computational fluid dynamics (CFD) modeling to optimize pump internals for your specific slurry characteristics. This includes customized impeller designs, volute configurations, and clearance settings that minimize wear while maintaining efficient operation.
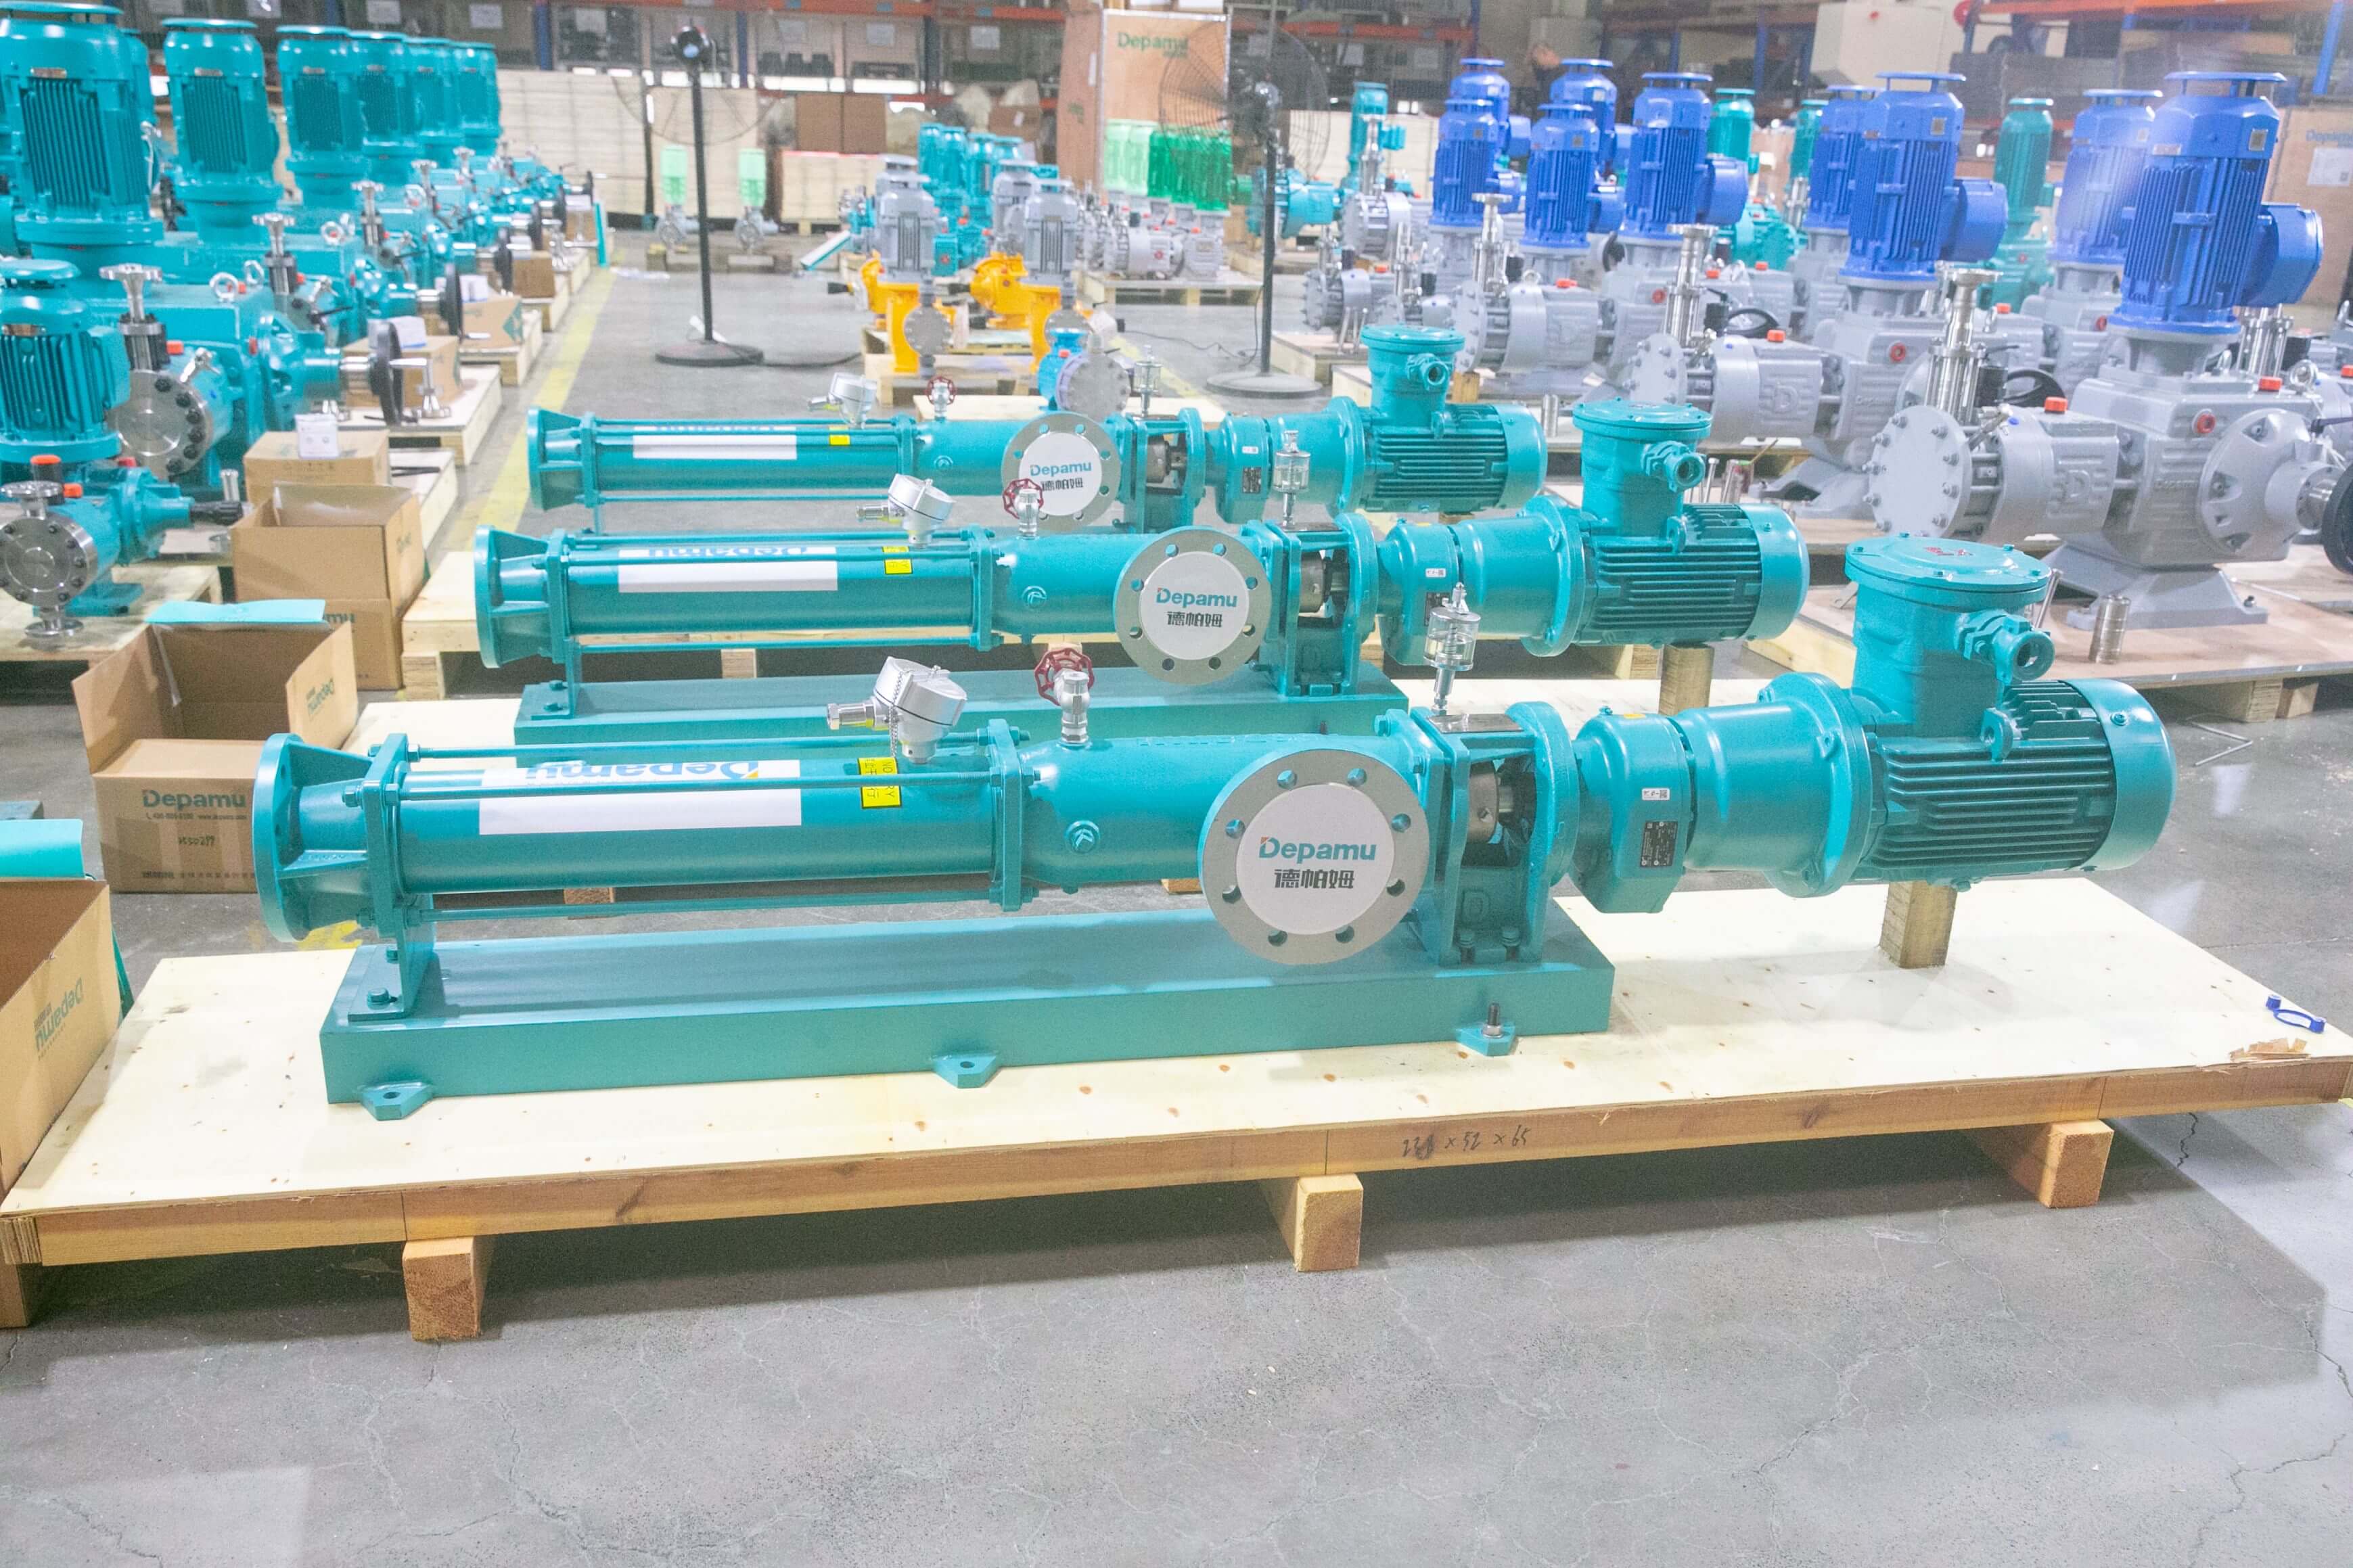
Sealing Solutions: We offer multiple sealing options including mechanical seals with specialized face materials, gland packing for high-temperature applications, and magnetic drive configurations for zero-leakage requirements. Our patented sealing technologies reduce maintenance requirements by up to 75% in demanding applications.
Control Systems: For automated operations, we integrate intelligent control systems that monitor pump performance parameters in real-time. These systems adjust operating parameters automatically to maintain optimal performance and provide early warning of potential issues before they cause downtime.
Key Technical Specifications
Our custom concentrate slurry pumps deliver industry-leading performance parameters:
| Parameter | Specification Range |
|---|---|
| Flow Rate | 0.5-2000 m³/h (customizable) |
| Discharge Pressure | Up to 35MPa (5,000 psi) |
| Temperature Range | -40°C to +350°C |
| Viscosity Handling | Up to 50,000 cP |
| Solid Content | Up to 70% by weight |
Industry-Specific Pump Solutions
Our application engineering team develops customized solutions for diverse industrial requirements:
Mining Applications: For ore concentrate transfer, we engineer pumps with hardened wet ends that withstand abrasive slurries containing particles up to 10mm in diameter. Our high-pressure models efficiently transport slurries over long distances with minimal energy consumption.
Chemical Processing: In corrosive environments, we select materials like Hastelloy C-276 or titanium that resist chemical attack while maintaining structural integrity. Our hermetically sealed designs prevent leakage of hazardous substances, ensuring worker safety and environmental protection.
Oil & Gas Production: For well stimulation and fracturing operations, we supply high-pressure pumps capable of handling proppant-laden fluids at pressures exceeding 10,000 psi. These robust designs feature reinforced casings and specialized seals to withstand extreme operating conditions.
Power Generation: Our boiler feed pumps and water treatment systems maintain precise flow control for optimal plant efficiency. The automated chemical dosing units we supply reduce water consumption by up to 30% through precise pH control and corrosion inhibition.
Quality Assurance & Certification
Every pump we manufacture undergoes rigorous testing before shipment, including:
- Hydrostatic pressure testing to 1.5x maximum operating pressure
- Performance verification against specified flow and pressure curves
- Material composition analysis using spectrometric methods
- Noise and vibration measurements per ISO standards
- Functional testing of control and monitoring systems
Our quality management system complies with ISO 9001:2015 standards, and we hold multiple international certifications including ATEX, CE, and API 675. These certifications demonstrate our commitment to meeting the highest industry standards for safety, reliability, and performance.
FAQ
What makes your concentrate slurry pumps different from standard models?
Our pumps feature custom-engineered components tailored to your specific slurry characteristics, including particle size, concentration, and chemical composition. We use advanced materials and hydraulic designs that extend service life by up to 300% compared to standard models, while our intelligent control systems optimize performance and reduce maintenance requirements.
How do you ensure pump reliability in abrasive applications?
We employ multiple strategies including hardened wet end materials, specialized coatings, and optimized hydraulic designs that minimize wear. Our application engineers analyze your specific slurry composition to select the most appropriate materials and design features, ensuring reliable operation even in the most demanding environments.
What lead time should I expect for custom pump orders?
Standard configurations typically ship within 4-6 weeks, while fully customized solutions require 8-12 weeks depending on complexity. Our project management team provides detailed timelines during the quotation phase and keeps you updated on production progress throughout the manufacturing process.
Do you offer installation and commissioning services?
Yes, we provide comprehensive field services including installation supervision, system commissioning, and operator training. Our service technicians have extensive experience with complex pumping systems and can ensure your equipment operates at peak efficiency from day one.
What warranty coverage do your pumps include?
All our pumps come with a standard 12-month warranty covering manufacturing defects and premature component failure. We also offer extended warranty options up to 36 months for additional peace of mind, subject to specific terms and conditions.
Summary
Depamp (Hangzhou) Pump Technology Co., Ltd. stands as your premier partner for customized concentrate slurry pump solutions. With nearly two decades of experience serving global industries, we combine advanced engineering capabilities with rigorous quality standards to deliver pumping systems that exceed expectations. Our comprehensive approach covers everything from initial consultation and custom design through manufacturing, testing, and field support, ensuring you receive a complete solution tailored to your specific requirements. Whether you need a single custom pump or a complete fluid handling system, our team has the expertise to deliver reliable, efficient, and cost-effective solutions that drive your operational success.