
In modern industrial processes, precision and reliability in fluid handling are non-negotiable requirements. For over two decades, Depamp (Hangzhou) Pump Technology Co., Ltd. has established itself as a premier manufacturer of high pressure sealed diaphragm pumps and comprehensive fluid handling solutions. With 400+ skilled professionals, a 35,000m² production facility, and annual output exceeding 500 million RMB, our company delivers engineered excellence across petrochemical, nuclear, power generation, and environmental protection industries worldwide.
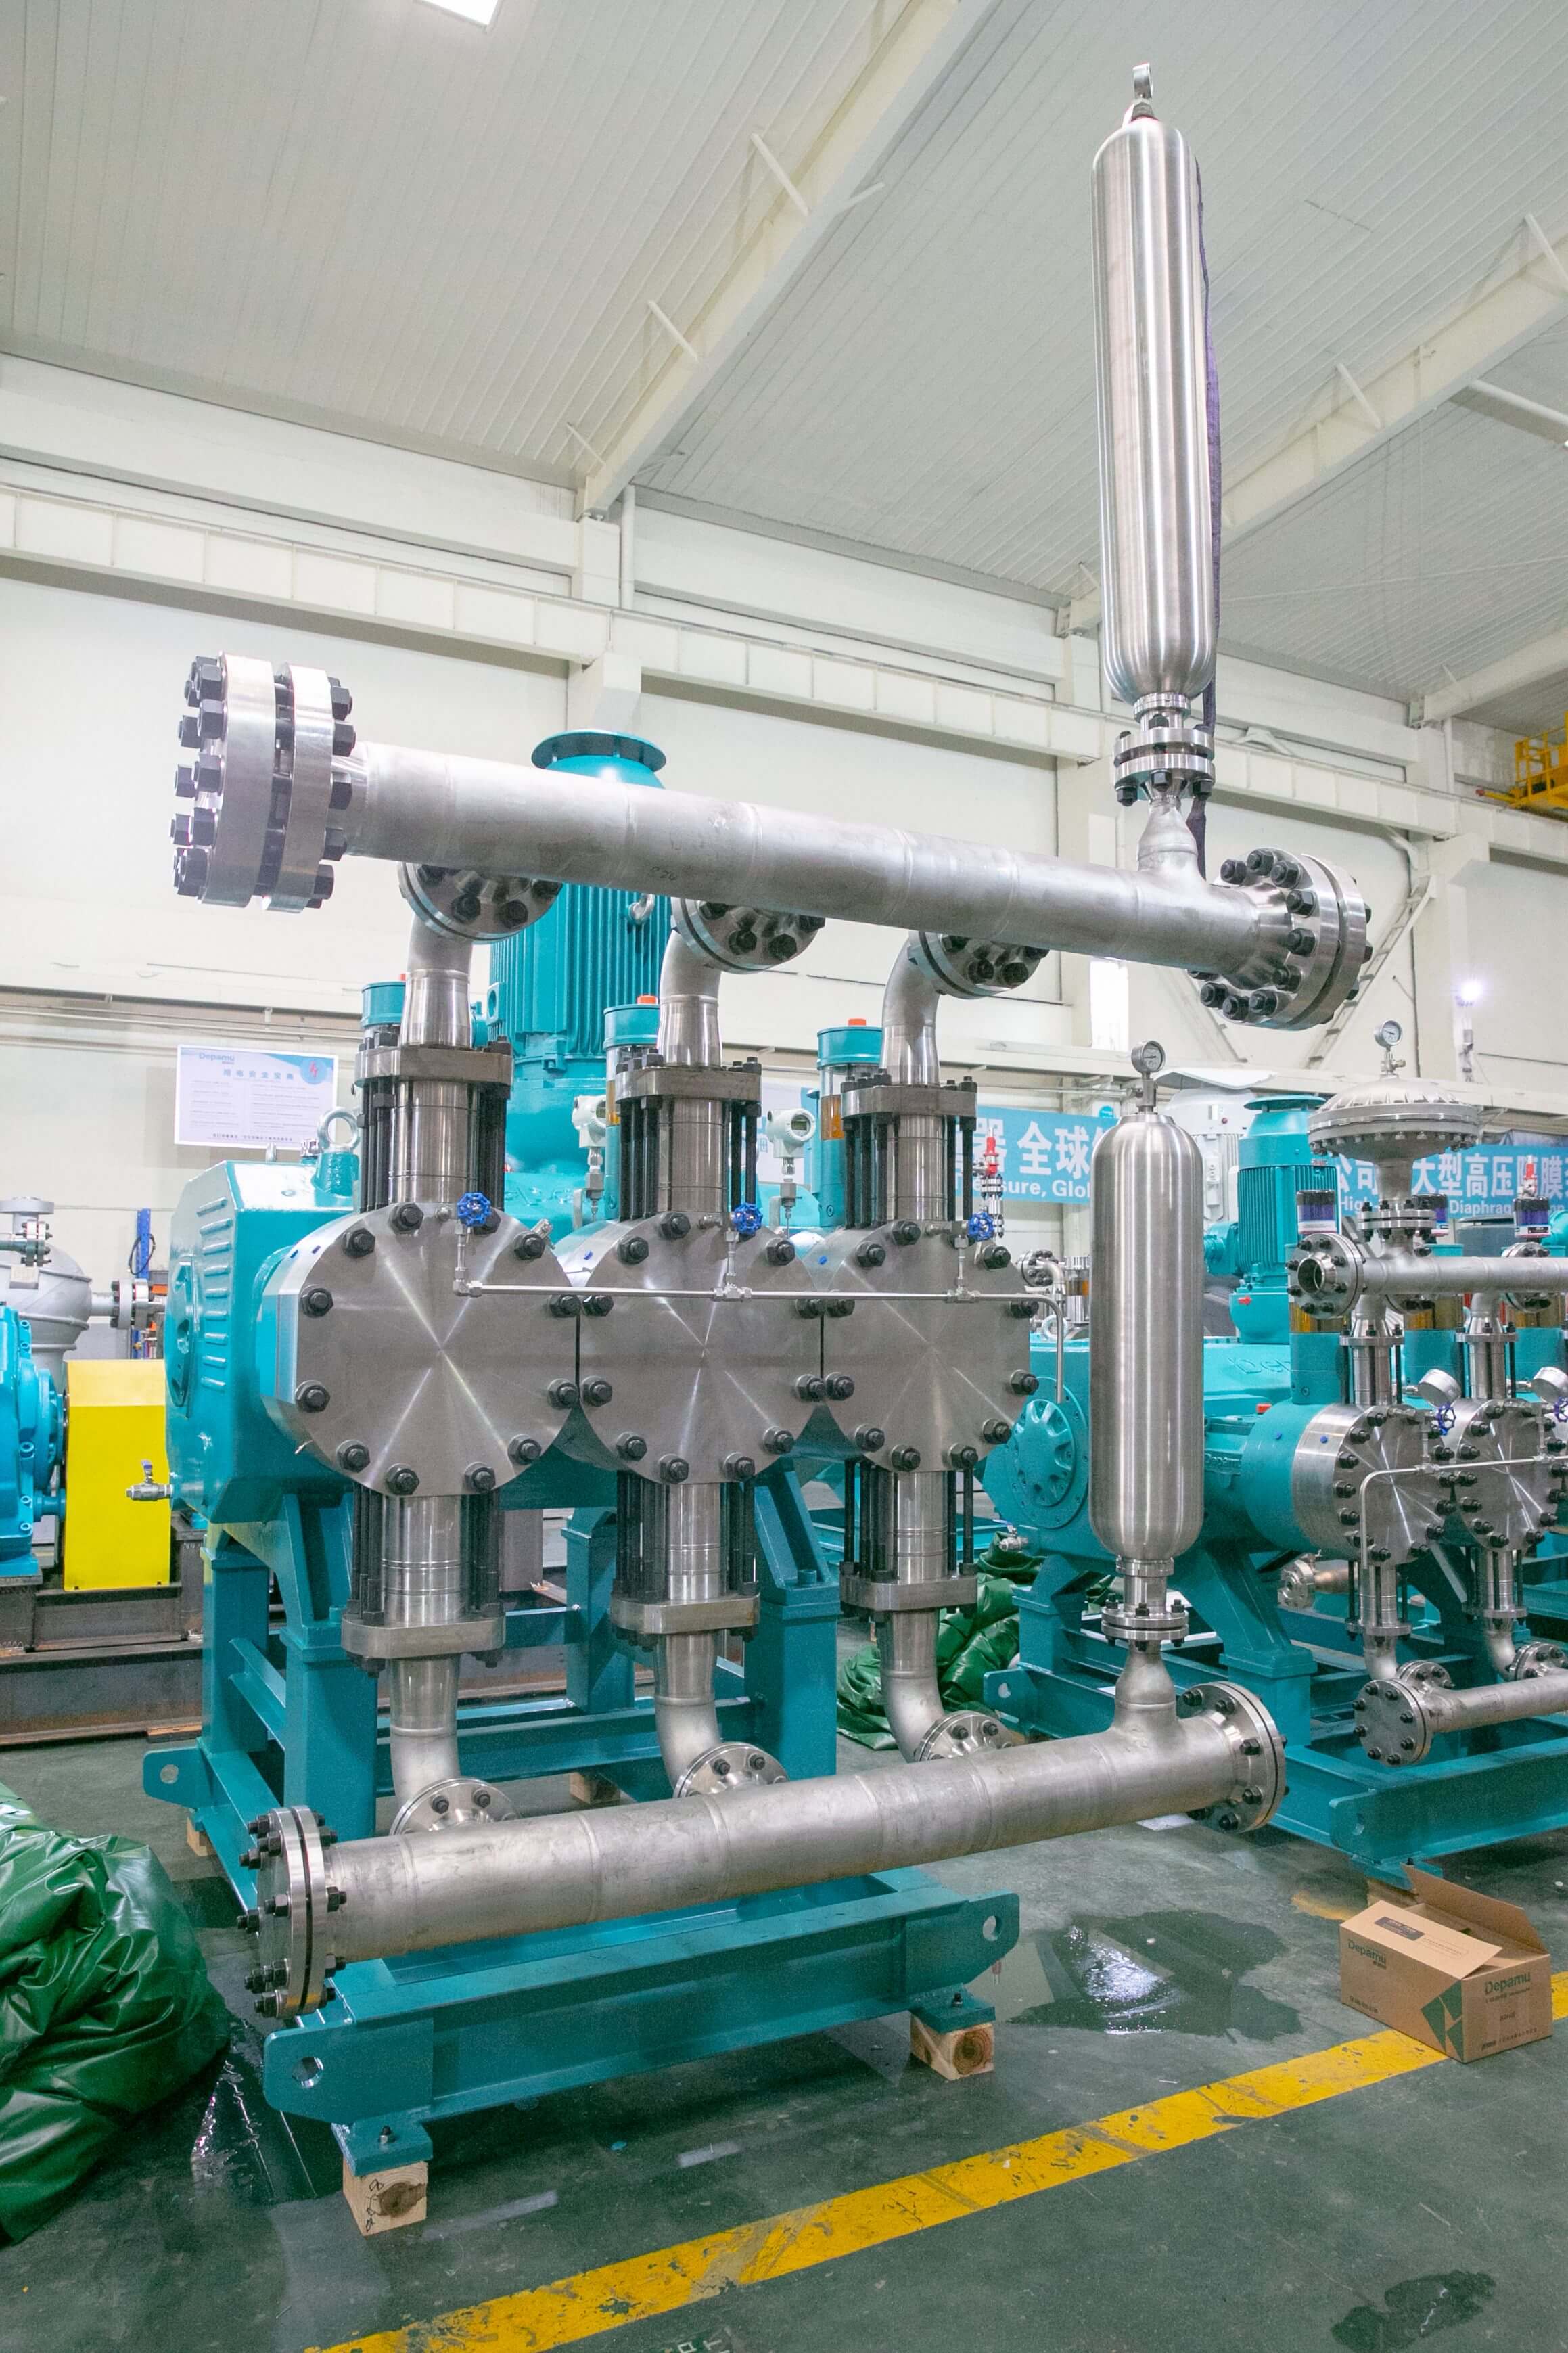
Core Competencies in High Pressure Pump Engineering
Our technical foundation rests on three pillars: German-engineered precision, continuous innovation, and application-specific customization. The hydraulic diaphragm metering pump series exemplifies this approach, functioning as industrial-grade “precision infusion devices” that deliver chemical agents with ±1% accuracy across 0-100% stroke length adjustment. These pumps maintain zero leakage through their patented hydraulic diaphragm structure, enabling safe handling of corrosive, volatile, and high-pressure media in petrochemical refining, wastewater treatment, and pharmaceutical production.
The high pressure process reciprocating pumps represent another technological breakthrough. With pressure ratings exceeding 35MPa and flow rates from 0.5 to 500m³/h, these “industrial power boosters” efficiently transport viscous fluids, slurries containing solid particles, and high-temperature media over long distances. Their robust design incorporates hardened alloy components, self-lubricating bearings, and modular valve assemblies, ensuring continuous operation in demanding environments like offshore oil platforms and geothermal power stations.
Comprehensive Fluid Handling Solutions
Beyond individual pump units, Depamp specializes in integrated systems that streamline industrial processes. Our fully automatic chemical dosing systems combine storage, dissolution, mixing, metering, and control functions into turnkey solutions. These “automated chemical stations” feature:
- Dual-powder/liquid dosing capabilities
- Multi-point injection with automatic synchronization
- PLC-based control with remote monitoring
- Pre-assembled skid mounting for rapid deployment
Such systems have proven instrumental in boiler water treatment, circulating cooling systems, and petrochemical refining operations, reducing chemical consumption by 15-30% while improving process stability.
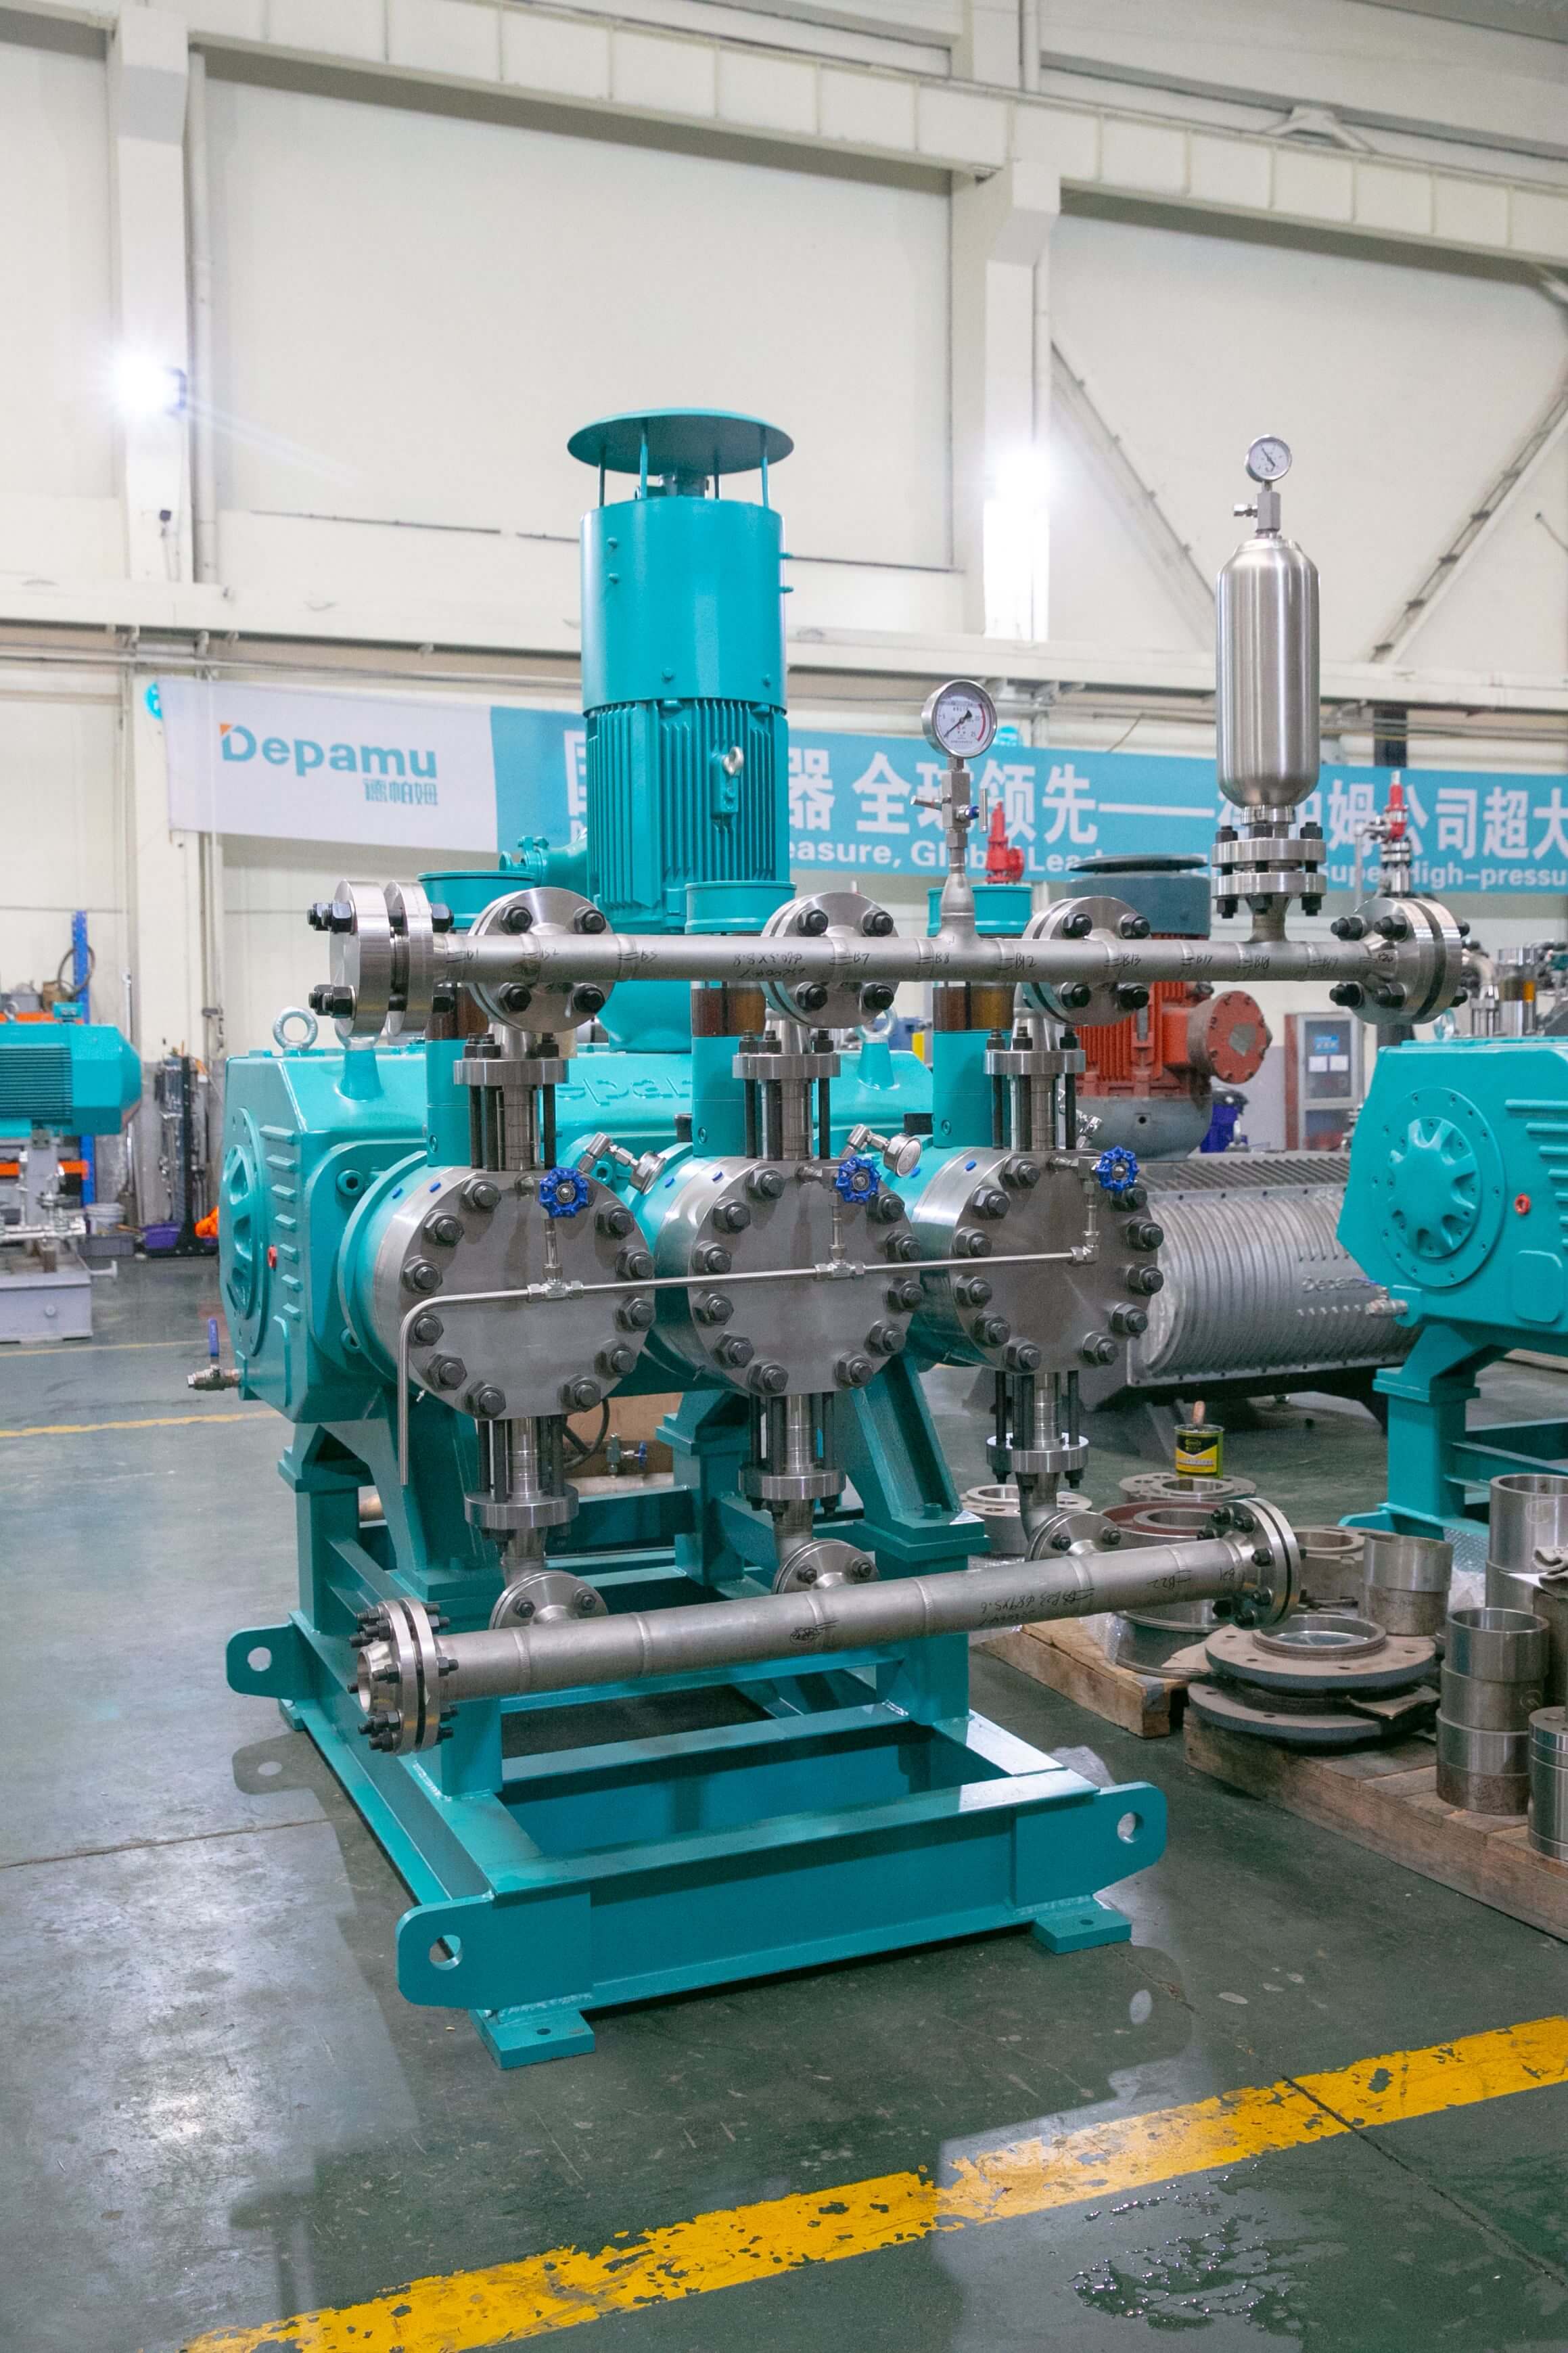
Application-Specific Product Matrix
Our product portfolio addresses diverse industrial requirements through specialized designs:
| Product Category | Key Features | Target Applications |
|---|---|---|
| Hydraulic Diaphragm Pumps | ±1% accuracy, 0-35MPa pressure, PTFE/PPS diaphragm | Chemical injection, wastewater treatment |
| High Pressure Reciprocating | 35MPa+ pressure, 500m³/h flow, alloy construction | Oilfield injection, pipeline boosting |
| Screw Pumps | Gentle handling, 10,000cSt viscosity, self-priming | Food processing, lubricant transfer |
| Chemical Dosing Systems | PLC control, 6-channel dosing, explosion-proof | Power plant chemistry, refinery units |
Custom Engineering Capabilities
What truly distinguishes Depamp is our ability to transform standard products into tailored solutions. Our engineering team follows a structured customization process:
- Media Analysis: Comprehensive testing of fluid properties including pH, viscosity, temperature, and particulate content
- Process Simulation: Computational fluid dynamics modeling to optimize pump sizing and configuration
- Material Selection: Choice from 200+ special alloys and elastomers for maximum component compatibility
- Prototyping: Rapid production of sample units for field testing under actual operating conditions
- Documentation: Detailed technical manuals, spare parts diagrams, and maintenance protocols
This approach enabled us to develop a corrosion-resistant pump system for a Middle Eastern refinery handling hydrogen sulfide-laden crude at 220°C, extending service life by 400% compared to standard models. Another success story involves our custom-designed slurry pump for a Canadian mining operation, which reduced downtime by 75% through its wear-resistant ceramic lining and self-cleaning valve design.
FAQ
What makes hydraulic diaphragm pumps superior for chemical dosing?
Hydraulic diaphragm pumps maintain absolute separation between the process fluid and hydraulic oil through a dual-diaphragm system. This design prevents cross-contamination while enabling precise flow control from 0.1 to 50,000 L/h. The hydraulic actuation also provides smoother operation compared to mechanical diaphragm pumps, reducing pulsation by up to 90% when paired with our patented pulsation dampeners.
How do you ensure pump compatibility with corrosive media?
Our material selection process considers three critical factors: chemical compatibility, concentration, and temperature. For highly aggressive applications like hydrochloric acid injection, we specify PTFE-lined flow paths with Hastelloy C-276 wetted parts. Each pump undergoes 72-hour corrosion testing in simulated process conditions before release, with certification available per NACE MR0175/ISO 15156 standards.
What maintenance procedures extend pump lifespan?
Preventive maintenance should follow this schedule:
- Daily: Check lubricant levels and inspect for leaks
- Weekly: Verify calibration and clean air filters (for pneumatic models)
- Monthly: Replace diaphragms and seals based on wear indicators
- Annually: Overhaul pump head and validate performance curves
Our digital maintenance kits include NFC-tagged spare parts and an IoT-enabled condition monitoring system that predicts component failures 2-4 weeks in advance.
How do your pumps comply with international standards?
All products meet or exceed:
- API 675 for reciprocating pumps
- ISO 5199 for centrifugal pumps
- ATEX Zone 2/22 for explosive atmospheres
- ASME B73.1 for chemical process pumps
Facilities holding ISO 9001, ISO 14001, and ISO 45001 certifications ensure consistent quality through automated production lines with 100% final inspection and traceability to raw material batches.
Summary
Depamp’s evolution from a regional pump supplier to a global fluid handling leader stems from our unwavering commitment to technical precision and customer-centric innovation. By combining German engineering heritage with Chinese manufacturing efficiency, we deliver solutions that reduce total cost of ownership by 20-35% through extended service life, lower energy consumption, and minimized maintenance requirements. Our 35,000m² smart factory, equipped with Industry 4.0 technologies like digital twin modeling and AI-powered quality control, ensures consistent delivery of the 50,000+ pumps and systems we produce annually. Whether handling simple water transfer or complex chemical processes, clients worldwide trust Depamp for pumps that work smarter, last longer, and deliver measurable value.