
When it comes to industrial fluid handling, precision, reliability, and durability are non-negotiable. For over two decades, Depamump (Hangzhou) Pump Technology Co., Ltd. has been at the forefront of developing and manufacturing high-performance three-lobe pumps that meet the most demanding requirements across various industries. As a trusted three-lobe pump manufacturer and supplier, we combine German engineering expertise with continuous innovation to deliver solutions that optimize your processes and enhance operational efficiency.
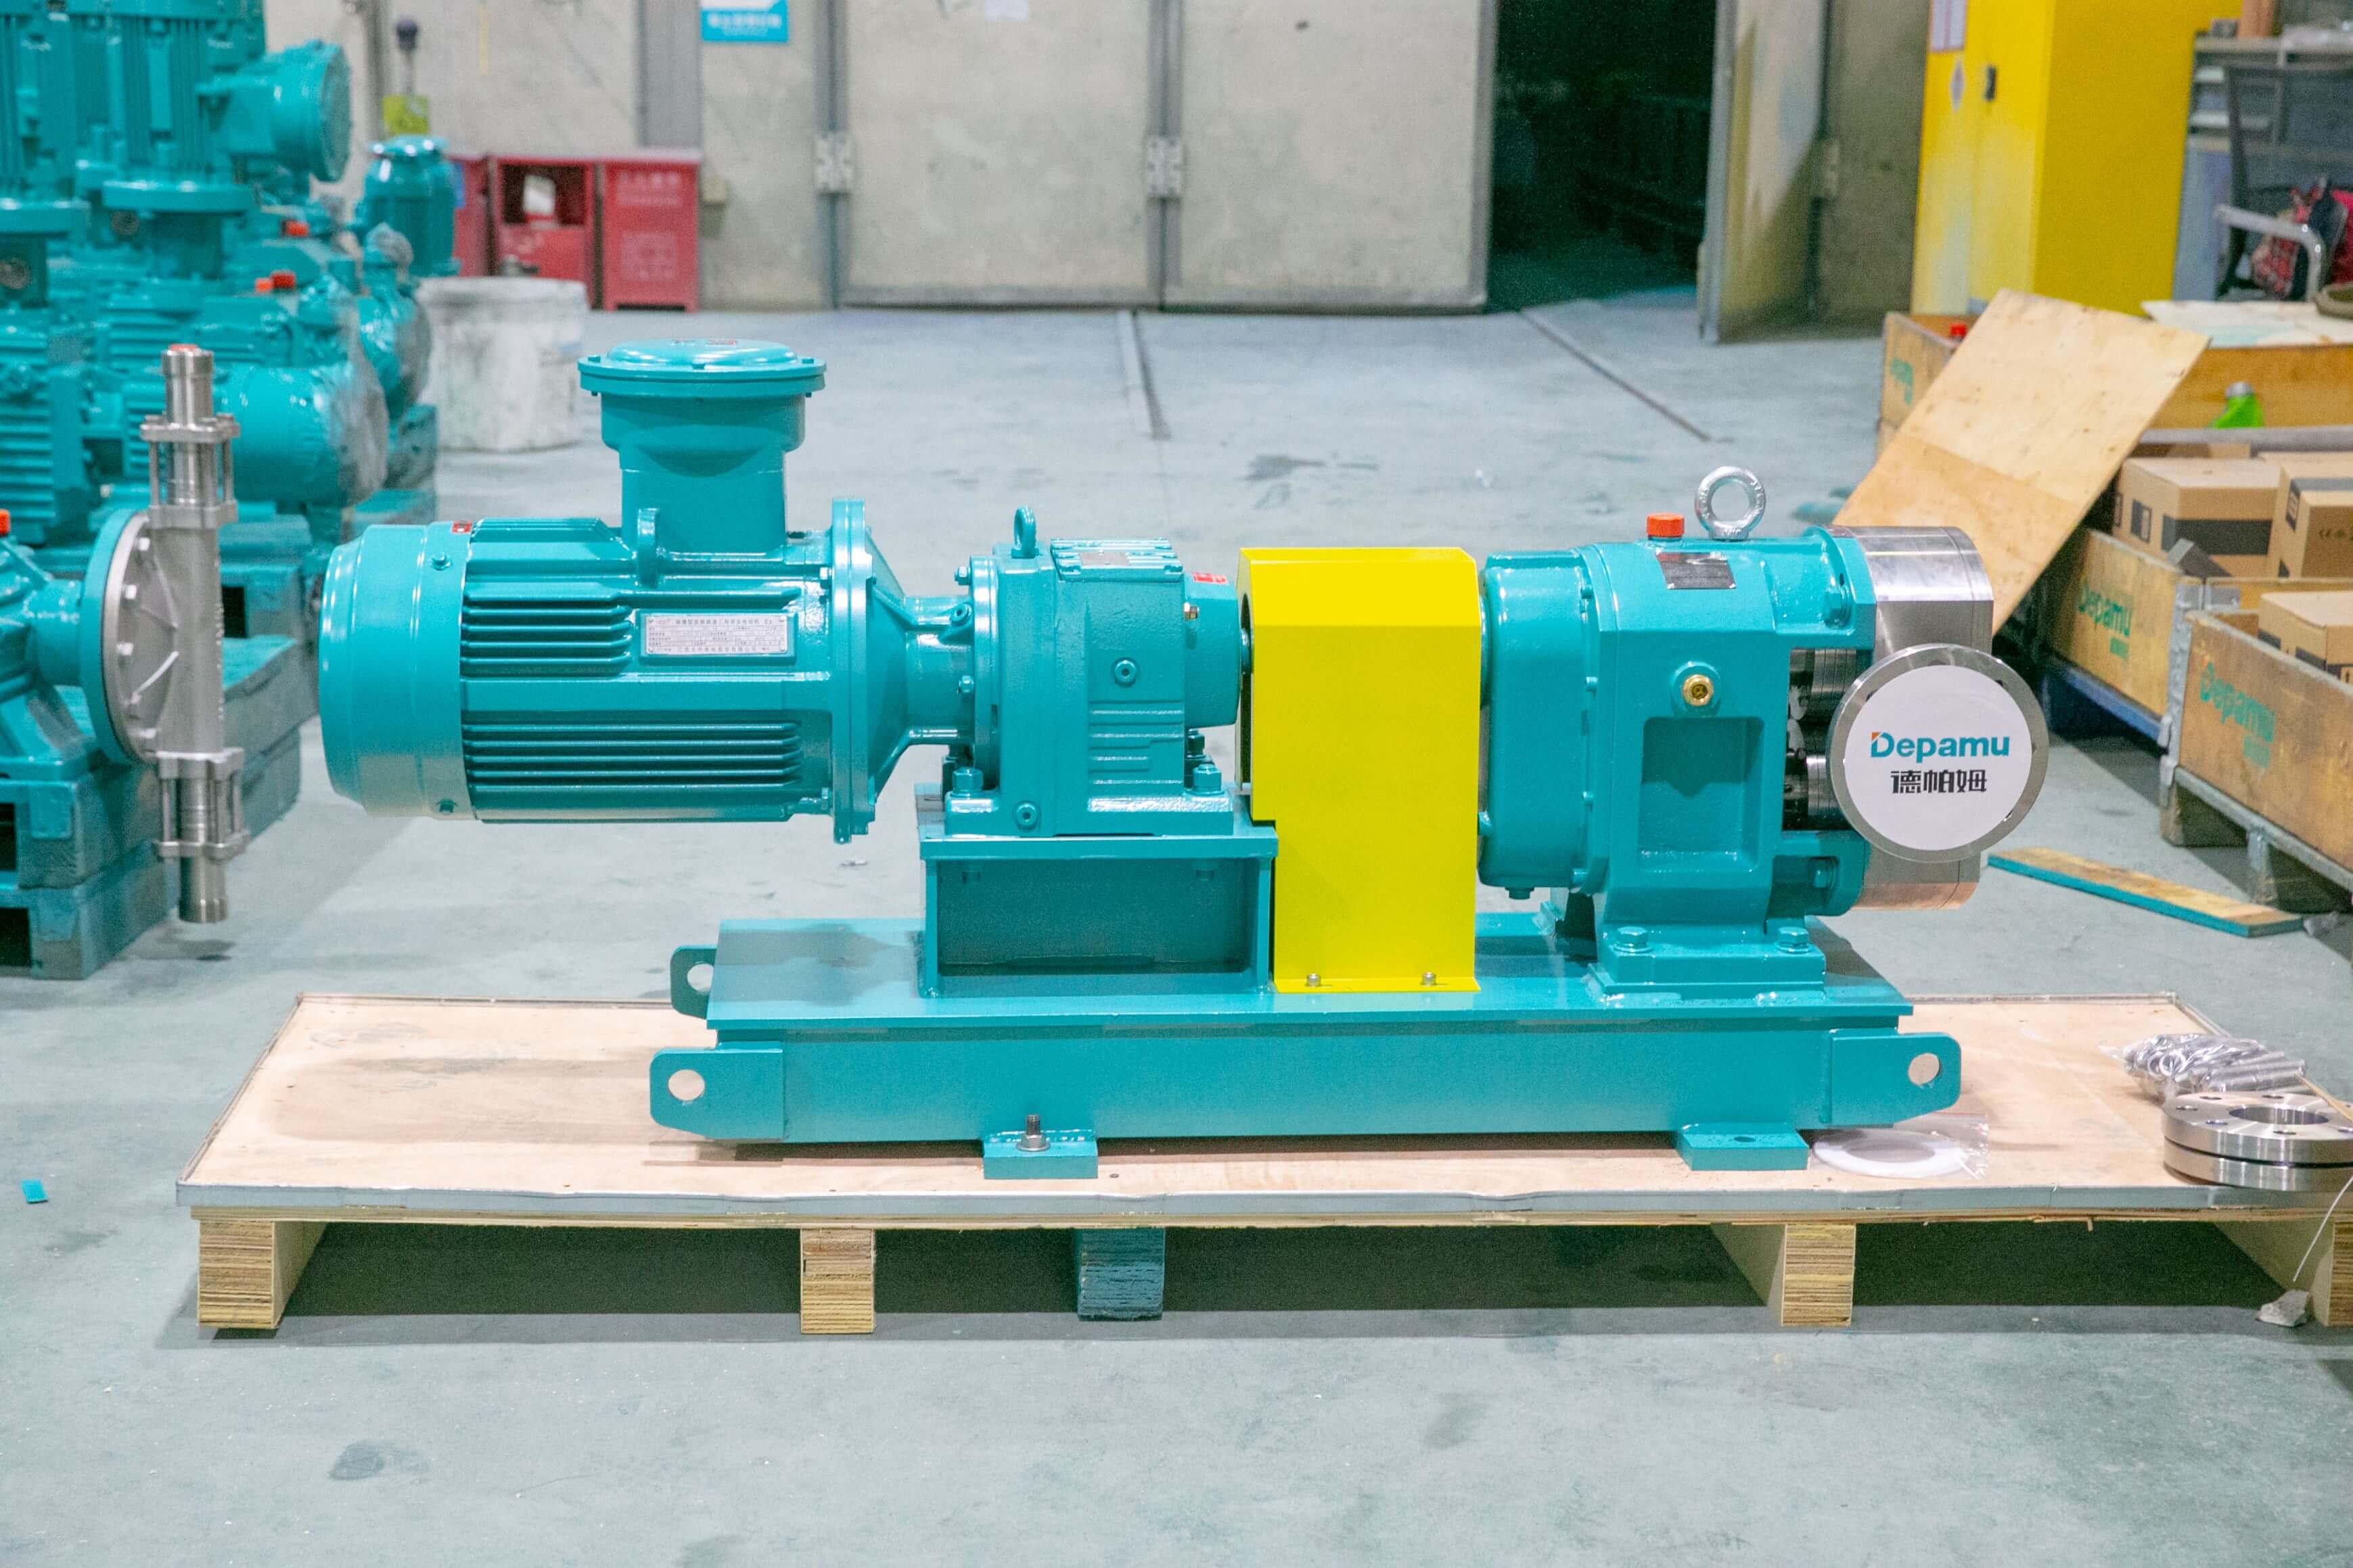
Why Choose Depamump as Your Three-Lobe Pump Manufacturer?
At Depamump, we understand that every industrial application has unique challenges. That’s why we don’t just manufacture standard three-lobe pumps – we engineer customized solutions tailored to your specific needs. Our comprehensive approach covers everything from initial consultation and design to manufacturing, testing, and after-sales support.
With a 35,000-square-meter production facility and a team of over 400 skilled professionals, we maintain strict quality control throughout the manufacturing process. Our annual production value exceeds 500 million RMB, reflecting our commitment to delivering high-volume, high-quality three-lobe pumps to clients worldwide.
Key Features of Our Three-Lobe Pumps
Our three-lobe pumps are designed to handle the most challenging fluid transfer applications with exceptional precision and reliability. Here are some of the key features that set our products apart:
- Precise Metering Capability: Our three-lobe pumps excel at delivering accurate flow rates, making them ideal for applications requiring precise chemical dosing or additive injection.
- Robust Construction: Built to withstand harsh operating conditions, our pumps feature durable materials and corrosion-resistant components that ensure long service life even in demanding environments.
- Versatile Media Handling: From viscous slurries to abrasive chemicals, our three-lobe pumps can handle a wide range of fluids with varying properties, including those with high solid content or aggressive chemical compositions.
- Low Pulsation Design: The three-lobe rotor configuration minimizes flow pulsation, providing smooth, continuous operation that protects your piping system and ensures consistent process performance.
- Customizable Options: We offer extensive customization options, including different materials of construction, sealing arrangements, and drive configurations to match your specific application requirements.
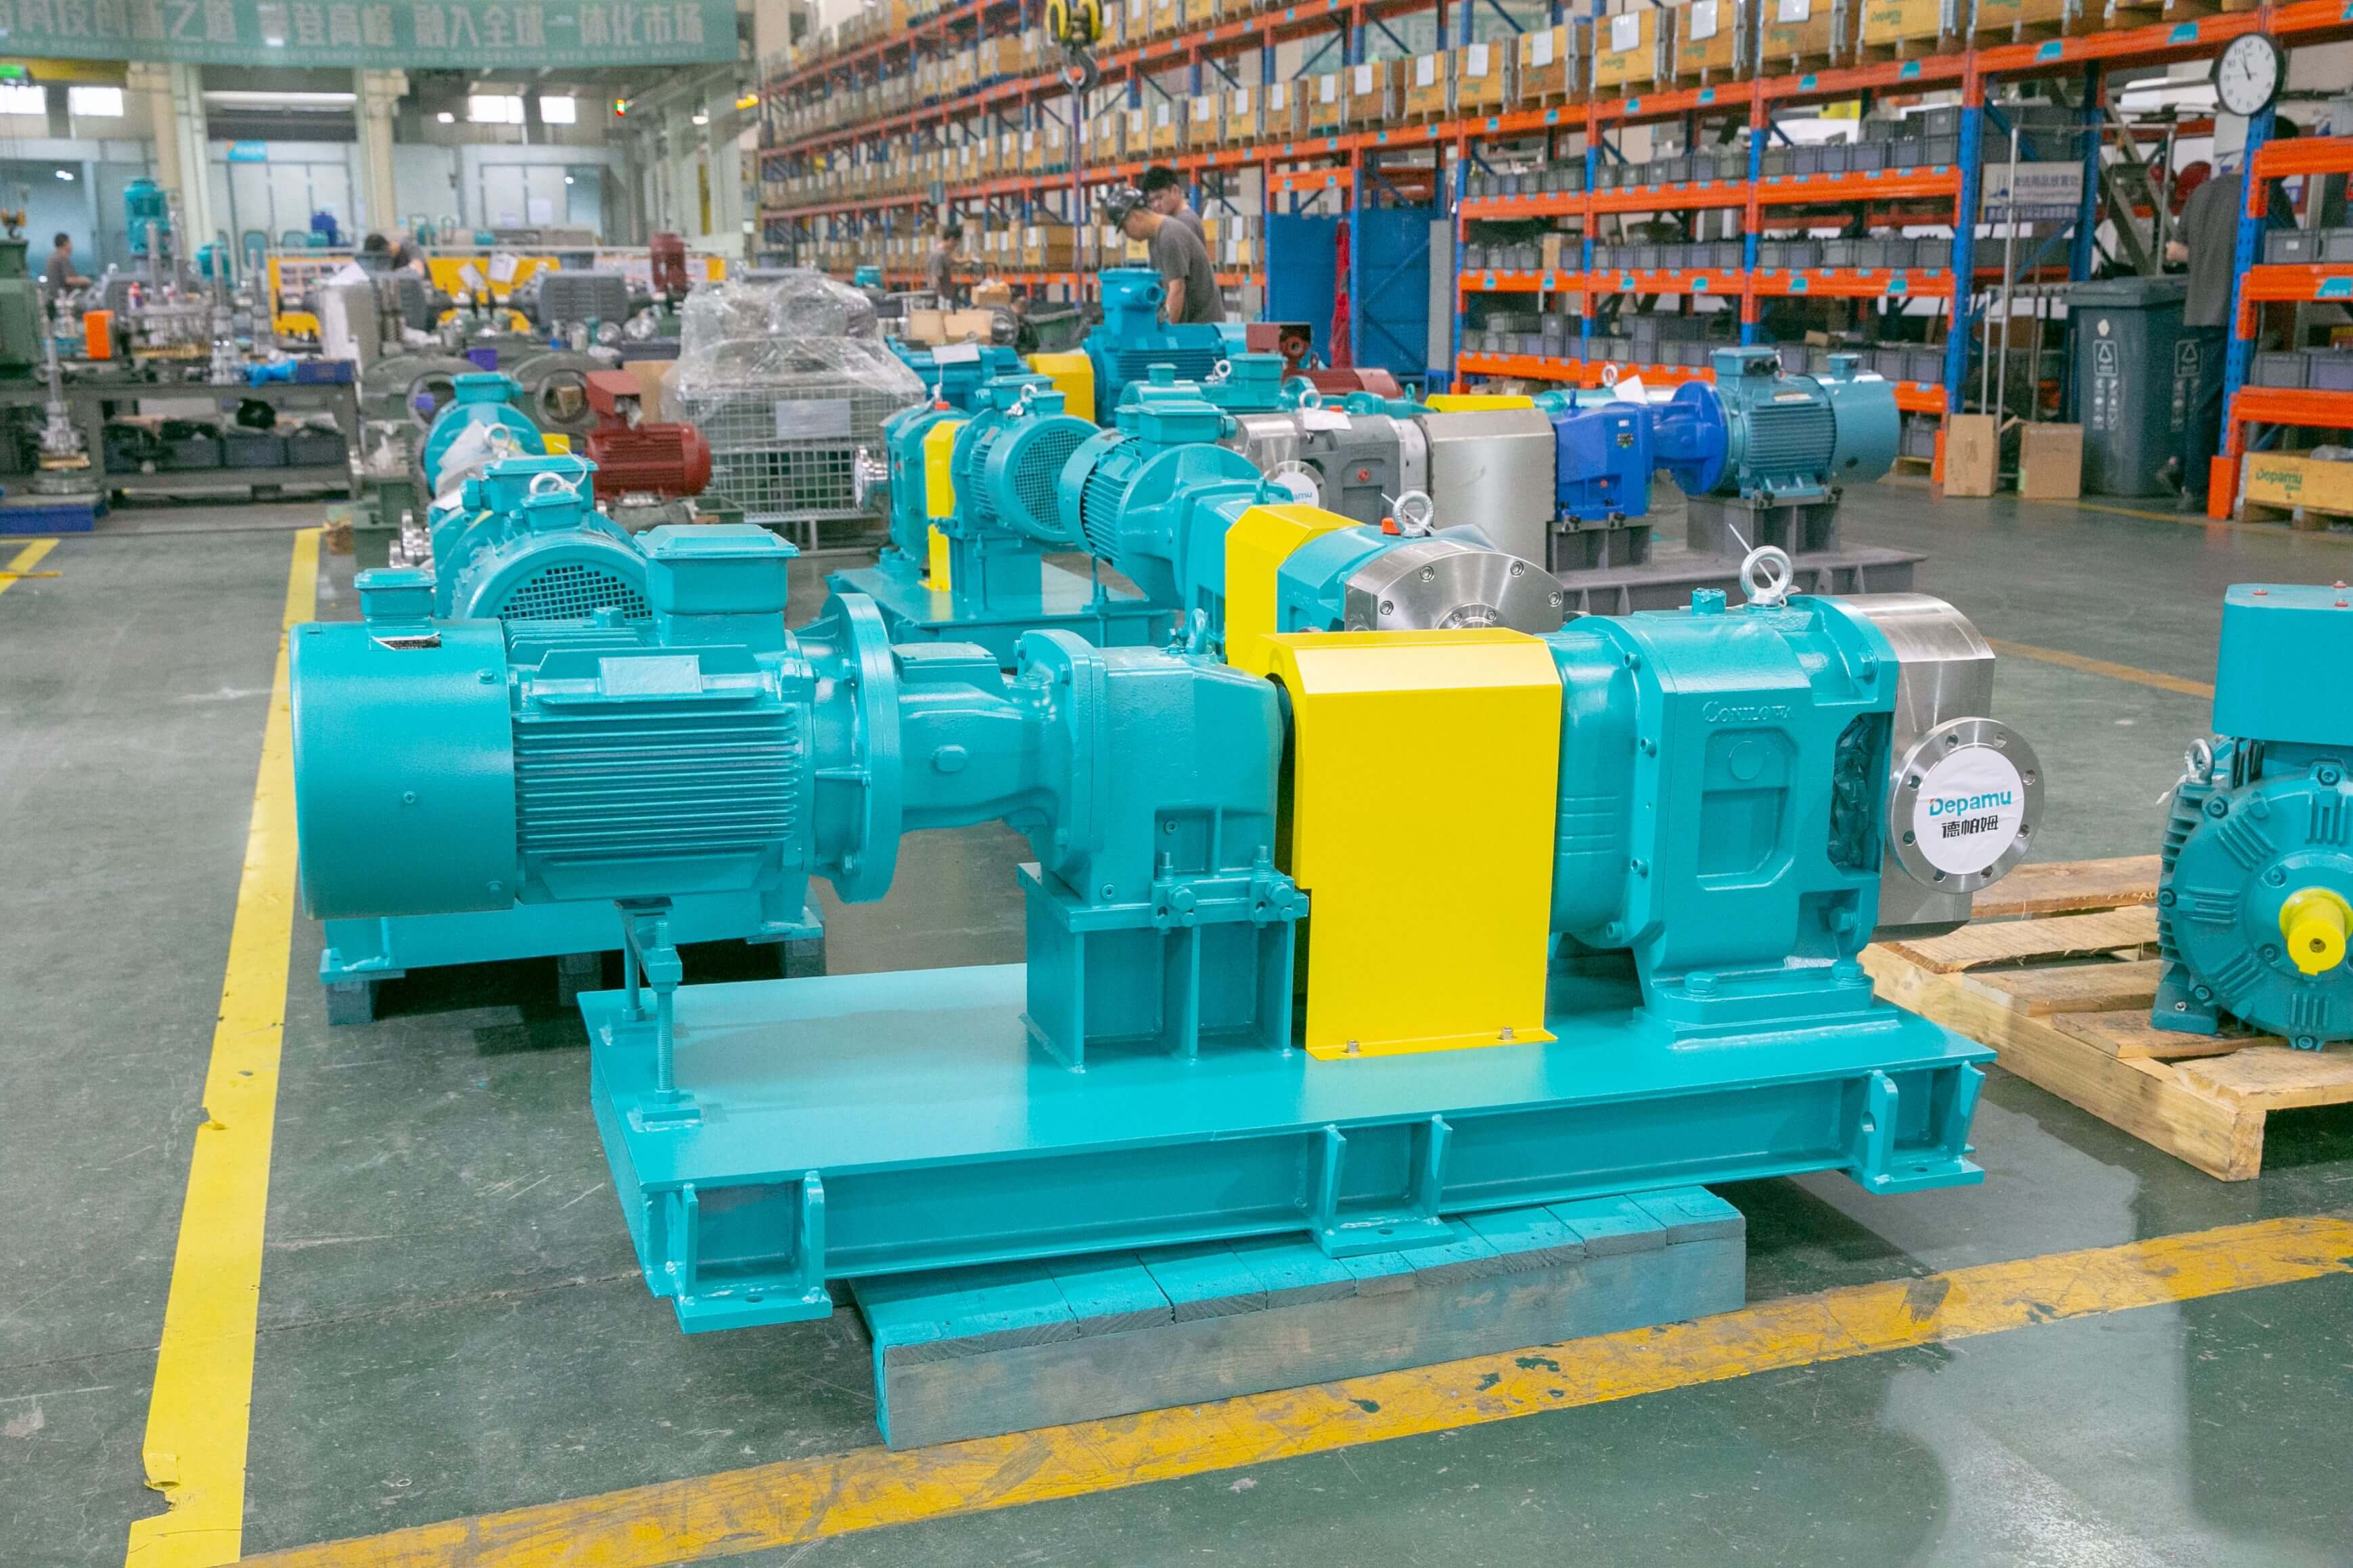
Industries Served by Our Three-Lobe Pumps
Our three-lobe pumps find applications across a diverse range of industries where precise, reliable fluid handling is critical. Some of our key market sectors include:
Petrochemical Industry
In petrochemical processing, our three-lobe pumps play a vital role in chemical injection, catalyst handling, and polymer processing applications. Their ability to handle corrosive chemicals at high pressures makes them indispensable in refineries and chemical plants.
Environmental Protection
For wastewater treatment and environmental protection applications, our three-lobe pumps provide accurate dosing of flocculants, coagulants, and other treatment chemicals. Their leak-free design ensures compliance with strict environmental regulations.
Food & Beverage
In the food and beverage industry, our sanitary three-lobe pumps meet the highest hygiene standards for transferring viscous products like sauces, dressings, and dairy products. Their gentle pumping action preserves product quality and integrity.
Pharmaceuticals
Pharmaceutical manufacturing requires pumps that can handle sensitive ingredients with precision and maintain sterile conditions. Our three-lobe pumps are designed for clean-in-place (CIP) and sterilize-in-place (SIP) applications, ensuring product purity and safety.
Custom Three-Lobe Pump Solutions
At Depamump, we recognize that off-the-shelf solutions don’t always meet the unique requirements of every application. That’s why we offer comprehensive customization services to create three-lobe pumps that perfectly match your specifications.
Our engineering team works closely with you to understand your process parameters, media characteristics, and operational requirements. We then develop a customized solution that optimizes performance, efficiency, and reliability for your specific application.
From material selection to sealing arrangements and drive configurations, every aspect of your three-lobe pump can be tailored to your needs. We also provide complete skid-mounted systems that integrate pumps, valves, instrumentation, and control systems for plug-and-play installation.
| Customization Option | Available Choices |
|---|---|
| Materials of Construction | Stainless steel, duplex steel, Hastelloy, titanium, PTFE-lined, etc. |
| Sealing Options | Mechanical seals, packed glands, magnetic drive, double mechanical seals |
| Drive Configurations | Electric motor, diesel engine, pneumatic motor, variable frequency drive |
| Control Systems | Local control panel, PLC-based automation, remote monitoring, flow meter integration |
| Mounting Options | Baseplate mounted, skid-mounted, mobile trailer-mounted |
FAQ
What makes three-lobe pumps different from other positive displacement pumps?
Three-lobe pumps offer several advantages over other positive displacement pumps like gear pumps or vane pumps. Their three-lobe rotor design provides smoother flow with lower pulsation, which reduces stress on piping systems and improves process stability. They also offer better self-priming capabilities and can handle fluids with higher solid content without clogging.
Can your three-lobe pumps handle corrosive chemicals?
Absolutely. We offer three-lobe pumps constructed from a wide range of corrosion-resistant materials including stainless steel, duplex steel, Hastelloy, and titanium. We can also provide pumps with PTFE-lined casings for handling the most aggressive chemicals. Our engineering team will help you select the optimal material based on your specific media properties.
What is the maximum pressure your three-lobe pumps can achieve?
Our three-lobe pumps are designed for medium to high-pressure applications. Depending on the model and configuration, we can provide pumps that achieve pressures up to 200 bar (2,900 psi) or higher for specialized applications. The exact pressure rating will depend on factors like pump size, material construction, and sealing arrangement.
Do you offer explosion-proof three-lobe pumps for hazardous areas?
Yes, we provide three-lobe pumps that comply with international explosion-proof standards such as ATEX and IECEx. These pumps feature explosion-proof motors, static grounding provisions, and other safety features to ensure safe operation in Class I, Division 1 or Zone 1 hazardous locations.
How do you ensure the quality of your three-lobe pumps?
Quality is at the core of everything we do at Depamump. We implement a comprehensive quality management system that covers every stage of production, from material inspection to final testing. Our pumps undergo rigorous performance testing, including hydrostatic testing, pressure testing, and functional testing before shipment. We also hold ISO 9001 certification and comply with other international quality standards.
Summary
As a leading three-lobe pump manufacturer and supplier, Depamump (Hangzhou) Pump Technology Co., Ltd. is committed to delivering innovative fluid handling solutions that drive your success. With over two decades of experience, state-of-the-art manufacturing facilities, and a team of dedicated engineers, we have the expertise to meet your most challenging three-lobe pump requirements.
Whether you need standard three-lobe pumps for general industrial applications or customized solutions for specialized processes, we have the capabilities to deliver. Our comprehensive product range, combined with our commitment to quality and customer service, makes us the ideal partner for all your three-lobe pump needs.
Contact us today to discuss your requirements and discover how our three-lobe pumps can optimize your fluid handling processes, improve efficiency, and reduce operating costs. Together, we can engineer solutions that propel your business forward.